Каталог Tungaloy глубокое сверление 1 - страница 32
Навигация
 Брошюра Tungaloy новая продукция
 Каталог Tungaloy инструмент для автоматов швейцарского типа
 Каталог Tungaloy глубокое сверление 2
 Общий каталог Tungaloy 2020 - 2021
 Каталог Tungaloy зубофрезерование
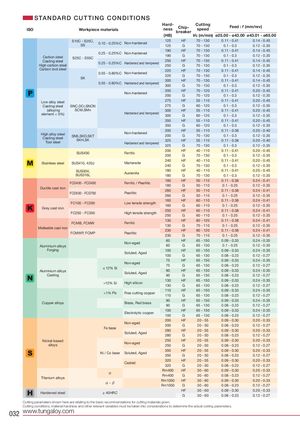
| ISO | Workpiec | e materials | Hard- ness | Chip- | Cutting speed | Feed :f | (mm/rev) | ||
| (HB) | breaker | Vc (m/min) | ø25.00 - ø43.0 | 0 ø43.01 - ø65.00 | |||||
| S10C - S25C, SS | 0.10 - 0.25%C | Non-hardened | 125 125 | HF G | 70 - 130 70 - 130 | 0.11 - 0.41 0.1 - 0.3 | 0.14 - 0.45 0.12 - 0.35 | ||
| 0.25 - 0.25%C | Non-hardened | 190 190 | HF G | 70 - 130 70 - 130 | 0.11 - 0.41 0.1 - 0.3 | 0.14 - 0.45 0.12 - 0.35 | |||
| Carbon steel Casting steel | S25C - S55C | 025 - 025%C | Hardened and tempered | 250 | HF | 70 - 130 | 0.11 - 0.41 | 0.14 - 0.45 | |
| High carbon steel | . . | 250 | G | 70 - 130 | 0.1 - 0.3 | 0.12 - 0.35 | |||
| Carbon tool steel | 0.55 - 0.80%C | Non-hardened | 220 220 | HF G | 70 - 130 70 - 130 | 0.11 - 0.41 01 - 03 | 0.14 - 0.45 012 - 035 | ||
| SK | H | 300 | HF | 70 - 130 | . . 0.11 - 0.41 | . . 0.14 - 0.45 | |||
| 0.55 - 0.80%C | ardened and tempered | 300 | G | 70 - 130 | 0.1 - 0.3 | 0.12 - 0.35 | |||
| Non-hardened | 200 | HF | 70 - 120 | 0.11 - 0.41 | 0.20 - 0.45 | ||||
| 200 | G | 70 - 120 | 0.1 - 0.3 | 0.12 - 0.35 | |||||
| Llll | 275 | HF | 55 - 110 | 0.11 - 0.41 | 0.20 - 0.45 | ||||
| ow aoy stee | 275 | G | 60 - 120 | 01 - 03 | 012 - 035 | ||||
| Casting steel (alloying | SNC,DCr,SNCN SCM,SMn | Hdd d td | 300 | HF | 55 - 110 | . . 0.11 - 0.41 | . . 0.20 - 0.45 | ||
| element < 5%) | arene an empere | 300 | G | 60 - 120 | 0.1 - 0.3 | 0.12 - 0.35 | |||
| 350 | HF | 55 - 110 | 0.11 - 0.41 | 0.20 - 0.45 | |||||
| 350 200 | G HF | 60 - 120 55 - 110 | 0.1 - 0.3 0.11 - 0.38 | 0.12 - 0.35 0.20 - 0.40 | |||||
| High alloy steel Casting steel | SNS,SKD,SKT | Non-hardened | 200 | G | 70 - 130 | 0.1 - 0.3 | 0.12 - 0.35 | ||
| Tool steel | SKH,SK | Hardened and temered | 325 | HF | 55 - 110 | 0.11 - 0.38 | 0.20 - 0.40 | ||
| p | 325 | G | 70 - 130 | 0.1 - 0.3 | 0.12 - 0.35 | ||||
| SUS430 | Ferritic | 200 | HF | 40 - 110 | 0.11 - 0.41 | 0.20 - 0.45 | |||
| 200 240 | G HF | 70 - 130 40 - 110 | 0.1 - 0.3 0.11 - 0.41 | 0.12 - 0.35 0.20 - 0.45 | |||||
| Stainless steel | SUS410, 420J | Martensite | 240 | G | 70 - 130 | 0.1 - 0.3 | 0.12 - 0.35 | ||
| SUS304, | Austenite | 180 | HF | 40 - 110 | 0.11 - 0.41 | 0.20 - 0.45 | |||
| SUS316L | 180 | G | 70 - 130 | 0.1 - 0.3 | 0.12 - 0.35 | ||||
| FCD400 - FCD450 | Ferritic / Pearlitic | 180 | HF | 50 - 110 | 0.11 - 0.38 | 0.24 - 0.41 | |||
| Ductile cast iron | 180 260 | G HF | 50 - 110 50 - 110 | 0.1 - 0.25 0.11 - 0.38 | 0.12 - 0.35 0.24 - 0.41 | ||||
| FCD500 - FCD700 | Pearlitic | 260 | G | 50 - 110 | 0.1 - 0.25 | 0.12 - 0.35 | |||
| FC100 - FC200 | Low tensile strength | 160 | HF | 60 - 110 | 0.11 - 0.38 | 0.24 - 0.41 | |||
| 160 | G | 60 - 110 | 0.1 - 0.25 | 0.12 - 0.35 | |||||
| Grey cast iron | FC250 - FC350 | High tensile strength | 250 250 | HF G | 60 - 110 60 - 110 | 0.11 - 0.38 0.1 - 0.25 | 0.24 - 0.41 0.12 - 0.35 | ||
| 130 | HF | 80 - 120 | 0.11 - 0.38 | 0.24 - 0.41 | |||||
| FCMB, FCMW | Ferritic | 130 | G | 70 - 110 | 0.1 - 0.25 | 0.12 - 0.35 | |||
| Malleable cast iron | FCMWP, FCMP | Pearlitic | 230 230 | HF G | 80 - 120 70 - 110 | 0.11 - 0.38 0.1 - 0.25 | 0.24 - 0.41 0.12 - 0.35 | ||
| 60 | HF | 65 - 150 | 0.09 - 0.33 | 0.24 - 0.35 | |||||
| Aluminium alloys | Non-aged | 60 | G | 65 - 130 | 0.1 - 0.25 | 0.12 - 0.35 | |||
| Forging | Sltd Ad | 100 | HF | 65 - 150 | 0.09 - 0.33 | 0.24 - 0.35 | |||
| oue,ge | 100 | G | 65 - 130 | 0.08 - 0.23 | 0.12 - 0.27 | ||||
| 12% Si | Non-aged | 75 75 | HF G | 65 - 150 65 - 130 | 0.09 - 0.33 0.08 - 0.23 | 0.24 - 0.35 0.12 - 0.27 | |||
| Aluminium alloys | ≤ | 90 | HF | 65 - 150 | 0.09 - 0.33 | 0.24 - 0.35 | |||
| Casting | Soluted, Aged | 90 | G | 65 - 130 | 0.08 - 0.23 | 0.12 - 0.27 | |||
| >12% Si | Hih silicon | 130 | HF | 65 - 150 | 0.09 - 0.33 | 0.24 - 0.35 | |||
| g | 130 110 | G HF | 65 - 130 65 - 150 | 0.08 - 0.23 009 - 033 | 0.12 - 0.27 024 - 035 | ||||
| >1% Pb | Free cuttingcopper | 110 | G | 65 - 130 | . . 0.08 - 0.23 | . . 0.12 - 0.27 | |||
| 90 | HF | 65 - 150 | 0.09 - 0.33 | 0.24 - 0.35 | |||||
| Copper alloys | Brass, Red brass | 90 | G | 65 - 130 | 0.08 - 0.23 | 0.12 - 0.27 | |||
| Electrolytic copper | 100 | HF | 65 - 150 | 0.09 - 0.33 | 0.24 - 0.35 | ||||
| 100 200 | G HF | 65 - 130 20 - 55 | 0.08 - 0.23 009 - 030 | 0.12 - 0.27 020 - 033 | |||||
| Fe base | Non-aged | 200 | G | 20 - 50 | . . 0.08 - 0.23 | . . 0.12 - 0.27 | |||
| 280 | HF | 20 - 55 | 0.09 - 0.30 | 0.20 - 0.33 | |||||
| Soluted, Aged | 280 | G | 20 - 50 | 008 - 023 | 012 - 027 | ||||
| Nickel-based | Non-aged | 250 | HF | 20 - 55 | . . 0.09 - 0.30 | . . 0.20 - 0.33 | |||
| alloys | 250 350 | G HF | 20 - 50 20 - 55 | 0.08 - 0.23 009 - 030 | 0.12 - 0.27 020 - 033 | ||||
| Ni / Co base | Soluted, Aged | 350 | G | 20 - 50 | . . 0.08 - 0.23 | . . 0.12 - 0.27 | |||
| 320 | HF | 20 - 55 | 0.09 - 0.30 | 0.20 - 0.33 | |||||
| Casted | 320 | G | 20 - 50 | 0.08 - 0.23 | 0.12 - 0.27 | ||||
| α | Rm400 | HF | 30 - 60 | 0.09 - 0.30 | 0.20 - 0.33 | ||||
| Rm400 | G | 30 - 60 | 0.08 - 0.23 | 0.12 - 0.27 | |||||
| Titanium alloys | α-β | Rm1050 Rm1050 | HF G | 30 - 60 30 - 60 | 0.09 - 0.30 0.08 - 0.23 | 0.20 - 0.33 0.12 - 0.27 | |||
| Hardened steel | ≥ 40HRC | HF G | 30 - 60 30 - 60 | 0.09 - 0.30 0.08 - 0.23 | 0.20 - 0.33 0.12 - 0.27 |
Cutting parameters shown here are relating to the basic recommendations for cutting materials given. Cutting conditions, material hardness and other relevant variables must be taken into considerations to determine the actual cutting parameters.