Каталог Tungaloy глубокое сверление 1 - страница 20
Навигация
 Брошюра Tungaloy новая продукция
 Каталог Tungaloy инструмент для автоматов швейцарского типа
 Каталог Tungaloy глубокое сверление 2
 Общий каталог Tungaloy 2020 - 2021
 Каталог Tungaloy зубофрезерование
Tro u b l e s h o oting fo r insert damages
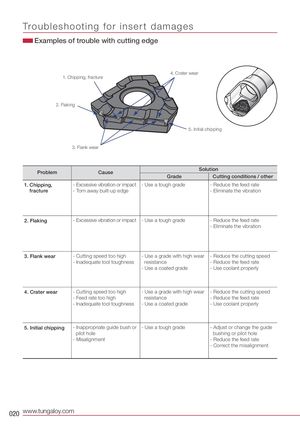
Examples of trouble with cutting edge
4. Crater wear 1. Chipping, fracture
2. Flaking
5. Initial chipping
3. Flank wear
| Problem | Cause | Sol | ution |
| Grade | Cuttingconditions / other | ||
| 1. Chipping, fracture | - Excessive vibration or impact - Torn away built-up edge | - Use a tough grade | - Reduce the feed rate - Eliminate the vibration |
| 2. Flaking | - Excessive vibration or impact | - Use a tough grade | - Reduce the feed rate - Eliminate the vibration |
| 3. Flank wear | - Cutting speed too high - Inadequate tool toughness | - Use a grade with high wear resistance - Use a coated grade | - Reduce the cutting speed - Reduce the feed rate - Use coolant properly |
| 4. Crater wear | - Cutting speed too high - Feed rate too high - Inadequate tool toughness | - Use a grade with high wear resistance - Use a coated grade | - Reduce the cutting speed - Reduce the feed rate - Use coolant properly |
| 5. Initial chipping | - Inappropriate guide bush or pilot hole - Misalignment | - Use a tough grade | - Adjust or change the guide bushing or pilot hole - Reduce the feed rate - Correct the misalignment |