Брошюра Tungaloy новая продукция - страница 84
Навигация
 Каталог Tungaloy глубокое сверление 2
 Каталог Tungaloy глубокое сверление 1
 Каталог Tungaloy зубофрезерование
 Общий каталог Tungaloy 2020 - 2021
 Каталог Tungaloy инструмент для автоматов швейцарского типа
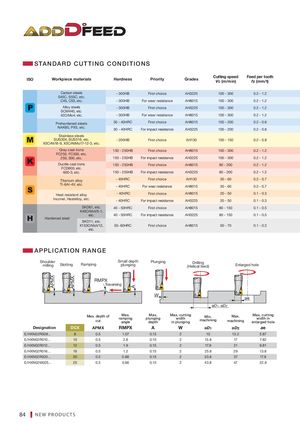
STANDARD CUTTING CONDITIONS
| ISO | Workpiece materials | Hardness | Priority | Grades | Cutting speed Vc (m/min) | Feed per tooth fz (mm/t) |
| Carbon steels S45C S55C etc | - 300HB | First choice | AH3225 | 100 - 300 | 0.2 - 1.2 | |
| , , . C45, C55, etc. | - 300HB | For wear resistance | AH8015 | 100 - 300 | 0.2 - 1.2 | |
| Alloy steels SCM440 etc | - 300HB | First choice | AH3225 | 100 - 300 | 0.2 - 1.2 | |
| , . 42CrMo4, etc. | - 300HB | For wear resistance | AH8015 | 100 - 300 | 0.2 - 1.2 | |
| Prehardened steels | 30 - 40HRC | First choice | AH8015 | 100 - 200 | 0.2 - 0.8 | |
| NAK80, PX5, etc. | 30 - 40HRC | For impact resistance | AH3225 | 100 - 200 | 0.2 - 0.8 | |
| Stainless steels SUS304, SUS316, etc. X5CrNi18-9, X5CrNiMo17-12-3, etc. | - 200HB | First choice | AH130 | 100 - 150 | 0.2 - 0.8 | |
| Gray cast irons FC250 FC300 etc | 150 - 250HB | First choice | AH8015 | 100 - 300 | 0.2 - 1.2 | |
| , , . 250, 300, etc. | 150 - 250HB | For impact resistance | AH3225 | 100 - 300 | 0.2 - 1.2 | |
| Ductile cast irons FCD600 etc | 150 - 250HB | First choice | AH8015 | 80 - 200 | 0.2 - 1.2 | |
| , . 600-3, etc. | 150 - 250HB | For impact resistance | AH3225 | 80 - 200 | 0.2 - 1.2 | |
| Titanium alloy | - 40HRC | First choice | AH130 | 30 - 60 | 0.2 - 0.7 | |
| Ti-6Al-4V, etc. | - 40HRC | For wear resistance | AH8015 | 30 - 60 | 0.2 - 0.7 | |
| Heat resistant alloy | - 40HRC | First choice | AH8015 | 20 - 50 | 0.1 - 0.3 | |
| Inconel, Hastelloy, etc. | - 40HRC | For impact resistance | AH3225 | 20 - 50 | 0.1 - 0.3 | |
| SKD61, etc. X40CrMoV5-1 | 40 - 50HRC | First choice | AH8015 | 80 - 150 | 0.1 - 0.5 | |
| Hardened steel , etc. | 40 - 50HRC | For impact resistance | AH3225 | 80 - 150 | 0.1 - 0.5 | |
| SKD11, etc. X153CrMoV12, etc. | 50~60HRC | First choice | AH8015 | 50 - 70 | 0.1 - 0.3 |
APPLICATION RANGE
| Shoulder | Small depth | Plunging | Drilling | |||
| milling | Slotting | Ramping | plunging | Enlarged hole |
(Helical feed) RMPX Traversing W
ae
øD1, øD 2
| Max. depth of | Max. | Max. | Max. cutting | Max. | Max. cutting | ||
| Min. | |||||||
| ramping | plunging | width | width in |
cut machining machining
angle depth in plunging enlarged hole
| Designation DCX | APMX | RMPX | A | W | øD | øD | ae | |||
| 1 | 2 | |||||||||
| E/HXN02R008... | 8 | 0.5 | 1.07 | 0.15 | 2 | 10 | 13.2 | 5.87 | ||
| E/HXN02R010... | 10 | 0.5 | 2.8 | 0.15 | 2 | 13.8 | 17 | 7.82 | ||
| E/HXN02R012... | 12 | 0.5 | 1.9 | 0.15 | 2 | 17.8 | 21 | 9.81 | ||
| E/HXN02R016... | 16 | 0.5 | 1.2 | 0.15 | 2 | 25.8 | 29 | 13.8 | ||
| E/HXN02R020... | 20 | 0.5 | 0.88 | 0.15 | 2 | 33.8 | 37 | 17.8 | ||
| E/HXN02M025... | 25 | 0.5 | 0.66 | 0.15 | 2 | 43.8 | 47 | 22.8 |