Каталог TooTool техническая информация 2 - страница 161
Навигация
 Каталог TooTool техническая информация 1
 Общий каталог TooTool
 Каталог TooTool монолитные фрезы
Technical Information for Spade Drill A\
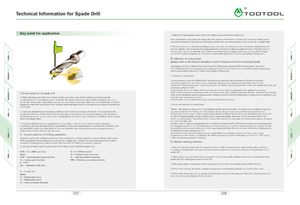
Key point for application 2. Selection of feed speed ( please refer to the Drilling Speed Recommendation List).
irons and different scrap irons will change the chip removal performance. Therefore, the control of drilling speed
can directly decide the chip removal performance and it's also the decisive factor of the service life os spade drills
If the feed speed is too slow during drilling process, the scrap iron will be too soft to be broken and will twine the
arbor. In addition, the excessively slow feed speed will accelerate the abrasion speed of insert. If the feed speed is
too fast, the scrap iron is relatively hard, will be removed in fragment shape, and is easy to cause chip blockage
and result in tipping, fragmenting. Therefore, it's particularly important to choose appropriate drilling speed..
III. Selection of cooling liqid
(please refer to the Recommendation List for Pressure and Flow of Cooling Liquid)
Reasonable selection of drilling fluid can reduce the drilling force, decrease drilling temperature, reduce the
thermal deformation of processing system, prolong the service life of tools, and improve the quality of processing
surface, particularly important to choose appropriate drilling speed.
1. Functions of clling liquid
Cooling function : pour the drilling fluid in the processing area and take advantage of thermal conduction,
convection, gasification and other means to decrease the processing temperature and reduce the thermal
deformation of processing syste. Lubricating function: the drilling liquid can permeate to the tools and between chip and
processing surface to form
protective film which can reduce the friction between contact surfaces and improve the quality of processing
surface. Chip removal and washing fuctions: it can remove the chip, guide the chip flow direction, and flush the scattered
I.Correct selection of spade drill
chips on the equipment and processing surface. Antirust function: since the drilling fluid is added antirust additive, it can
1. When selecting spade drill, users should get the connection type of arbor shank according to spindle react with the metal surface to form
connection type of the equipment used. Generally, the spindle connection type of ordinary equipment such as protective film. So as to play the functions of antirust and anti-corrosion.
bench drill, vertical drill, radial drilling machine, etc. is in taper shank mode, while as to the numerically controlled
equipment, side fixed type flange shank, straight shank and taper shank can be selected according to spindle type 2. Kinds and selection of cooling liquid
of the lathe.
"Water ”, with almost no direct cost, is the rapidest and the most convenient. The water can be supplied as much as
2. Users should determine the maximum drilling length of arbor according to the depth of the machined hole. you want. However, the indirect cost is the highest. Since it doesn’t have antirust & lubricating functions, the
Usually, the selection of arbor shall follow the principle of the minimum arbor length suitable to the thickness of cooling effect is not so good. After using the water, the life of drill bit will be influenced, the drilling machine & drill
machining workpiece, so as to improve the drilling rigidity of arbor and give full play to the drilling effects of spade bit will be oxidized quickly, and the machine will be damaged quickly. Therefore, it's not recommended to use ”
drill to the largest effect. water” as cooling liquid. "Oily drilling fluid” can reach the maximum in the aspect of various performances. However,
the cost is too high and
3. Users should determine the equivalent insert's and arbor's diameter, insert’ material and coating type it's often used on high-end equipment and is recycled."Emulsified liquid", with lower economic cost and proportion
according to the hole diameter, material and hardness of the machined workpiece. Generally, the machining hole for mixing with water of 1:20, has lubricating and antirust functions, as well as cooling function. It's featured by high
by spade drills can be controlled within 0.1mm and relatively high machining precision can guarantee users' acceptability and economical efficiency. Due to rapid speed and high efficiency of spade drill during drilling process,
requirements on hole diameter and tolerance. to realize full cooling and improve the
service life of tools, internal cooling method is adopted during the drilling process and there is also certain
IK Correct selection of drilling parameters requirement on the cooling. For example, the drilling pressure of common steel plate (such as Q235, Q345, etc) is
Aiming at spade drills of different diameters, the requirement on drilling speed is certainly different. Reasonable 3 -4kg, and the flow is about 20-25L/min.
drilling speed will directly influence the service life of spade drill. Therefore, it's particularly important to select
reasonable drilling speed so that the spade drill can match the drilling & machining material. IV. Matters needing attention
1. Selection of drilling speed (please refer to the Drilling Speed Recommendation List) 1. When selecting the spade drill, it's required to choose sitable connection type and matching arbor and insert
according to requirements on equipment and workpeice materials, so as to give full play to the performances of
RPM = (Vc x 1000) / (n x Dia.) Vf = fn x RPM (mm/min) spade drill.
where: Vf = Feed per minute (mm/min)
RPM = Revolution per minute (rev/min) fn = Feed per revolution (mm/rev) 2. Select correct and reasonable cutting parameters in accordance with workpeice material to avoid mismatching
Vc = Cutting speed (m/min) RPM = Revolution per minute (rev/min) spade drill with drilling parameters of twist drill.
TT =3.1416
3. Select appropriate cooling liquid and cooling pressure to improve the drilling quality and life of tools.
Dia. = Diameter of drill (mm)
4. Prevent violent bump during the cutting and spotting to avoid tipping and influence on life of the insert.
Tc = H / (Vf x 60)
where: 5. Prevent the phenomena such as spindle off and reverse rotation of the equipment during the drilling process for
such phenomena amy damage the insert easily.
Tc = Drilling Time (secs.)
H = Drilling depth (mm)
Vf = Feed per minute (mm/min)
677 678