Общий каталог Sumitomo 2018 - 2019 - страница 497
Навигация
 Общий каталог Sumitomo 2012
 Каталог Sumitomo резьбонарезной инструмент
 Каталог Sumitomo пластины с режущей кромкой-моноалмаз Sumicristal
 Каталог Sumitomo инструмент для обработки канавок
 Общий каталог Sumitomo 2019 - 2020
 Каталог Sumitomo запасные части
- Pages 3-6_CS6_EN_web
- A 1-20 insert selection EN_web
- B 1-14 grades_EN_web
- C01-17 inserts intro pages_EN_web
- C18-56 negative inserts_EN_web
- C57-86 positive inserts_EN_web
- D 1-46 tool holders_EN_web
- E 1-24 boring bars_EN_web
- F 1-48 grooving_thread tools_EN_web
- G 1-54 milling cutters_EN_web
- H 1-48 insert type endmills_EN_web
- J 1-24 new endmills_EN_web
- J 25-50 endmills_EN_web
- K 1-46 Multi-Drills_EN_web
- K 47-76 Multi-Drills_EN_web
- L 1-28 cbn_pcd grades_EN_web
- M 1-34 cbn_pcd inserts_EN_web
- M 35-56 SHM tools_EN_web
- N1-24 technical guidance_EN_web
- P 1-8 spare parts_neu_EN_web
- P 9-22 index_notes_EN_web
SUMIDIA N
DA1000 Non-ferrous Metal
- General Features
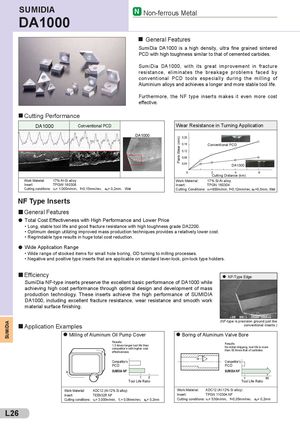
SumiDia DA1000 is a high density, ultra fine grained sintered
PCD with high toughness similar to that of cemented carbides.
SumiDia DA1000, with its great improvement in fracture
resistance, eliminates the breakage problems faced by
conventional PCD tools especially during the milling of
Aluminium alloys and achieves a longer and more stable tool life.
Furthermore, the NF type inserts makes it even more cost
effective. - Cutting Performance
DA1000 Conventional PCD Wear Resistance in Turning Application
DA1000 0,20 0,16 Conventional PCD 0,12
0,08 0,04 DA1000
| 0 | 2 | 4 | 6 |
| Cutting Distance (km) |
| Work Material: | 17% Al-Si alloy | Work Material: | 17% Si-Al alloy |
| Insert: | TPGW 160308 | Insert: | TPGN 160304 |
Cutting conditions: vc= 1.000m/min, f=0,15mm/rev, ap= 0,2mm, Wet Cutting Conditions: v =800m/min, f=0,12mm/rev, a =0,5mm, Wet c p NF Type Inserts - General Features
Total Cost Effectiveness with High Performance and Lower Price
- Long, stable tool life and good fracture resistance with high toughness grade DA2200.
- Optimum design utilizing improved mass production techniques provides a relatively lower cost.
- Regrindable type results in huge total cost reduction.
Wide Application Range
- Wide range of stocked items for small hole boring, OD turning to milling processes.
- Negative and positive type inserts that are applicable on standard lever-lock, pin-lock type holders.
Efficiency
- NF-Type Edge
l
SumiDia NF-type inserts preserve the excellent basic performance of DA1000 while
achieving high cost performance through optimal design and development of mass
production technology. These inserts achieve the high performance of SUMIDIA
DA1000, including excellent fracture resistance, wear resistance and smooth work
material surface finishing. Application Examples (NF-type is precision ground just like - conventional inserts.)
Milling of Aluminum Oil Pump Cover Boring of Aluminum Valve Bore
| Results: | Results: | ||||
| 1,5 times longer tool life than | No initial chipping, tool life is more | ||||
| competitor‘s with higher cost | than 50 times that of carbides. | ||||
| effectiveness. | |||||
| Competitor’s | Competitor’s | ||||
| PCD | PCD | ||||
| SUMIDIA NF | SUMIDIA NF | ||||
| Tool Life Ratio | Tool Life Ratio | ||||
| Work Material: | ADC12 (Al-12% Si alloy) | Work Material: | ADC12 (Al-12% Si alloy) | ||
| Insert: | TEEN32R NF | Insert: | TPGN 110304 NF | ||
| Cutting conditions: v = 3.000m/min, f = 0,06mm/rev, a = 0,2mm | Cutting conditions: v = 530m/min, f=0,05mm/rev, a = 0,2mm | ||||
| c | p t | c | p |