Общий каталог Sumitomo 2018 - 2019 - страница 473
Навигация
 Общий каталог Sumitomo 2012
 Каталог Sumitomo резьбонарезной инструмент
 Каталог Sumitomo пластины с режущей кромкой-моноалмаз Sumicristal
 Каталог Sumitomo инструмент для обработки канавок
 Общий каталог Sumitomo 2019 - 2020
 Каталог Sumitomo запасные части
- Pages 3-6_CS6_EN_web
- A 1-20 insert selection EN_web
- B 1-14 grades_EN_web
- C01-17 inserts intro pages_EN_web
- C18-56 negative inserts_EN_web
- C57-86 positive inserts_EN_web
- D 1-46 tool holders_EN_web
- E 1-24 boring bars_EN_web
- F 1-48 grooving_thread tools_EN_web
- G 1-54 milling cutters_EN_web
- H 1-48 insert type endmills_EN_web
- J 1-24 new endmills_EN_web
- J 25-50 endmills_EN_web
- K 1-46 Multi-Drills_EN_web
- K 47-76 Multi-Drills_EN_web
- L 1-28 cbn_pcd grades_EN_web
- M 1-34 cbn_pcd inserts_EN_web
- M 35-56 SHM tools_EN_web
- N1-24 technical guidance_EN_web
- P 1-8 spare parts_neu_EN_web
- P 9-22 index_notes_EN_web
CBN Tools H K PM S
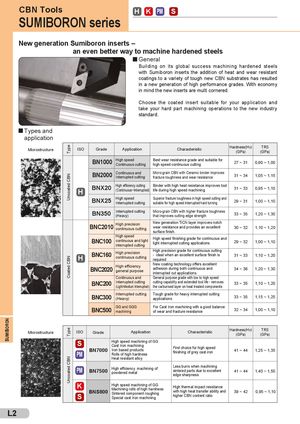
SUMIBORON series New generation Sumiboron inserts – an even better way to machine hardened steels - General
Building on its global success machining hardened steels
with Sumiboron inserts the addition of heat and wear resistant
coatings to a variety of tough new CBN substrates has resulted
in a new generation of high performance grades. With economy
in mind the new inserts are multi cornered.
Choose the coated insert suitable for your application and
take your hard part machining operations to the new industry
standard. - Types and
application
| Microstructure | Type | ISO | Grade | Application | Characteristic | Hardness(Hv) (GPa) | TRS (GPa) |
| BN1000 | High speed Continuous cutting | Best wear resistance grade and suitable for high speed continuous cutting | 27 ~ 31 | 0,90 ~ 1,00 | |||
| CBN | BN2000 | Continuous and Interrupted cutting | Micro-grain CBN with Ceramic binder improves fracture toughness and wear resistance | 31 ~ 34 | 1,05 ~ 1,15 | ||
| coated | H | BNX20 | High efficiency cutting (Continuous~Interrupted) | Binder with high heat resistance improves tool life during high speed machining | 31 ~ 33 | 0,95 ~ 1,10 | |
| Un | BNX25 | High speed Interrupted cutting | Superior fracture toughness in high speed cutting and suitable for high speed interrupted hard turning | 29 ~ 31 | 1,00 ~ 1,10 | ||
| BN350 | Interrupted cutting (Heavy) | Micro-grain CBN with higher fracture toughness that improves cutting edge strength | 33 ~ 35 | 1,20 ~ 1,30 | |||
| BNC2010 | High precision continuous cutting | New generation TiCN layer improves notch wear resistance and provides an excellent surface finish. | 30 ~ 32 | 1,10 ~ 1,20 | |||
| BNC100 | High speed continuous and light interrupted cutting | High speed finishing grade for continuous and light interrupted cutting applications | 29 ~ 32 | 1,00 ~ 1,10 | |||
| BN | H | BNC160 | High precision continuous cutting | High precision grade for continuous cutting - ideal when an excellent surface finish is required | 31 ~ 33 | 1,10 ~ 1,20 | |
| oated C | BNC2020 | High efficiency general purpose | New coating technology offers excellent adhesion during both continuous and interrupted cut applications. | 34 ~ 36 | 1,20 ~ 1,30 | ||
| C | BNC200 | Continuous and Interrupted cutting (Light-Medium Interrupted) | General purpose grade with low to high speed cutting capability and extended tool life - removes the carburised layer on heat treated components | 33 ~ 35 | 1,10 ~ 1,20 | ||
| BNC300 | Interrupted cutting (Heavy) | Tough grade for heavy interrupted cutting applications | 33 ~ 35 | 1,15 ~ 1,25 | |||
| BNC500 | GG and GGG machining | For Cast Iron machining with a good balance of wear and fracture resistance | 32 ~ 34 | 1,00 ~ 1,10 | |||
| Microstructure | Type | ISO | Grade | Application | Characteristic | Hardness(Hv) (GPa) | TRS (GPa) |
| BN | PM S | BN7000 H C Ir R H | igh speed machining of ast Iron machining on based products olls of high hardness eat resistant alloy | GG First choice for high speed finishing of grey cast iron | 41 ~ 44 | 1,25 ~ 1,35 | |
| ncoated C | PM | BN7500 H i p | igh efficiency machinin owdered metal | i g of Less burrs when machining sintered parts due to excellent edge sharpness | 41 ~ 44 | 1,40 ~ 1,50 | |
| U | K S | BNS800 H M S S | igh speed machining of achining rolls of high h intered component rou pecial cast Iron machin | GG ardness ghing ing High thermal impact resistance with high heat transfer ability and higher CBN content ratio | 39 ~ 42 | 0,95 ~ 1,10 |