Общий каталог Sumitomo 2018 - 2019 - страница 449
Навигация
 Общий каталог Sumitomo 2012
 Каталог Sumitomo резьбонарезной инструмент
 Каталог Sumitomo пластины с режущей кромкой-моноалмаз Sumicristal
 Каталог Sumitomo инструмент для обработки канавок
 Общий каталог Sumitomo 2019 - 2020
 Каталог Sumitomo запасные части
- Pages 3-6_CS6_EN_web
- A 1-20 insert selection EN_web
- B 1-14 grades_EN_web
- C01-17 inserts intro pages_EN_web
- C18-56 negative inserts_EN_web
- C57-86 positive inserts_EN_web
- D 1-46 tool holders_EN_web
- E 1-24 boring bars_EN_web
- F 1-48 grooving_thread tools_EN_web
- G 1-54 milling cutters_EN_web
- H 1-48 insert type endmills_EN_web
- J 1-24 new endmills_EN_web
- J 25-50 endmills_EN_web
- K 1-46 Multi-Drills_EN_web
- K 47-76 Multi-Drills_EN_web
- L 1-28 cbn_pcd grades_EN_web
- M 1-34 cbn_pcd inserts_EN_web
- M 35-56 SHM tools_EN_web
- N1-24 technical guidance_EN_web
- P 1-8 spare parts_neu_EN_web
- P 9-22 index_notes_EN_web
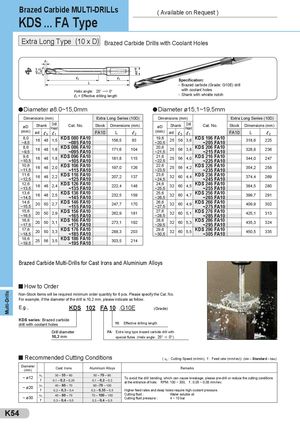
KDS FA Type ( Available on Request )
Extra Long Type (10 x D) Brazed Carbide Drills with Coolant Holes
Specification: - Brazed carbide (Grade: G10E) drill Helix angle: 25° ---> 0° with coolant holes l = Effective drilling length - Shank with whistle notch 2
| Dia Dime | me nsion | ter s(m | ø8. m) | 0~15,0mm | Extra L | ongSerie | s(10D) | Dia Dime | met nsions | er (m | ø15 m) | ,1~19,5mm | Extra | LongSerie | s(10D) |
| øD | Sh | ank | Drill Head | Cat. No. | Stock | Dimensio | ns(mm) | øD | Sha | nk | Drill Head | Cat. No. | Stock | Dimensio | ns(mm) |
| (mm) | ød | l3 | l1 | FA10 | L | l2 | (mm) | ød | l3 | l1 | FA10 | L | l2 | ||
| 8,0 ~8,5 | 16 | 48 | 1,5 | KDS 080 FA10 ~085 FA10 | 156,5 | 93 | 19,6 ~20,5 | 25 | 56 | 3,6 | KDS 196 FA10 ~205 FA10 | 318,6 | 225 | ||
| 8,6 ~9,5 | 16 | 48 | 1,6 | KDS 086 FA10 ~095 FA10 | 171,6 | 104 | 20,6 ~21,5 | 25 | 56 | 3,8 | KDS 206 FA10 ~215 FA10 | 328,8 | 236 | ||
| 9,6 ~10,5 | 16 | 48 | 1,8 | KDS 096 FA10 ~105 FA10 | 181,8 | 115 | 21,6 ~22,5 | 25 | 56 | 4,0 | KDS 216 FA10 ~225 FA10 | 344,0 | 247 | ||
| 10,6 ~11,5 | 16 | 48 | 2,0 | KDS 106 FA10 ~115 FA10 | 197,0 | 126 | 22,6 ~23,5 | 25 | 56 | 4,2 | KDS 226 FA10 ~235 FA10 | 354,2 | 258 | ||
| 11,6 ~12,5 | 16 | 48 | 2,2 | KDS 116 FA10 ~125 FA10 | 207,2 | 137 | 23,6 ~24,5 | 32 | 60 | 4,4 | KDS 236 FA10 ~245 FA10 | 374,4 | 269 | ||
| 12,6 ~13,5 | 16 | 48 | 2,4 | KDS 126 FA10 ~135 FA10 | 222,4 | 148 | 24,6 ~25,5 | 32 | 60 | 4,5 | KDS 246 FA10 ~255 FA10 | 384,5 | 280 | ||
| 13,6 ~14,5 | 16 | 48 | 2,5 | KDS 136 FA10 ~145 FA10 | 232,5 | 159 | 25,6 ~26,5 | 32 | 60 | 4,7 | KDS 256 FA10 ~265 FA10 | 399,7 | 291 | ||
| 14,6 ~15,5 | 20 | 50 | 2,7 | KDS 146 FA10 ~155 FA10 | 247,7 | 170 | 26,6 ~27,5 | 32 | 60 | 4,9 | KDS 266 FA10 ~275 FA10 | 409,9 | 302 | ||
| 15,6 ~16,5 | 20 | 50 | 2,9 | KDS 156 FA10 ~165 FA10 | 262,9 | 181 | 27,6 ~28,5 | 32 | 60 | 5,1 | KDS 276 FA10 ~285 FA10 | 425,1 | 313 | ||
| 16,6 ~17,5 | 20 | 50 | 3,1 | KDS 166 FA10 ~175 FA10 | 273,1 | 192 | 28,6 ~29,5 | 32 | 60 | 5,3 | KDS 286 FA10 ~295 FA10 | 435,3 | 324 | ||
| 17,6 ~18,5 | 20 | 50 | 3,3 | KDS 176 FA10 ~185 FA10 | 288,3 | 203 | 29,6 ~30,5 | 32 | 60 | 5,5 | KDS 296 FA10 ~305 FA10 | 450,5 | 335 | ||
| 18,6 ~19,5 | 25 | 56 | 3,5 | KDS 186 FA10 ~195 FA10 | 303,5 | 214 |
Brazed Carbide Multi-Drills for Cast Irons and Aluminium Alloys
How to Order
Non-Stock Items will be required minimum order quantity for 6 pcs. Please specify the Cat. No. For example, if the diameter of the drill is 10,2 mm, please indicate as follow.
E.g., KDS 102 FA 10 ,G10E (Grade)
KDS series: Brazed carbide drill with coolant holes 10: Effective drilling length Drill diameter FA: Extra long type brazed carbide drill with 10,2 mm special flutes (Helix angle: 25° a 0°)
Recommended Cutting Conditions
( v : Cutting Speed (m/min), f : Feed rate (mm/rev)) (Min – Standard – Max) c
| Diameter (mm) | Cast Irons | Aluminium Alloys | Remarks | |
| ~ ø12 ~ 20 | vc f vc | 30 –55– 60 0,1 –0,2– 0,25 40 –60– 70 | 50 –70– 90 0,1 –0,2– 0,3 60 –70– 100 | To avoid the drill bending, which can cause breakage, please pre-drill or reduce the cutting conditions at the entrance of hole; RPM: 100 ~ 300, f : 0,05 ~ 0,08 mm/rev. |
| ø | f | 0,2 –0,3– 0,4 | 0,3 –0,35– 0,5 | Higher feed rates and deep holes require high coolant pressure. l |
| ~ ø30 | vc f | 40 –60– 70 0,3 –0,4– 0,5 | 70 –100– 150 0,3 –0,4– 0,5 | Cutting fluid : Water soluble oil Cutting fluid pressure : 4 ~ 10 bar |