Общий каталог Sumitomo 2018 - 2019 - страница 432
Навигация
 Общий каталог Sumitomo 2012
 Каталог Sumitomo резьбонарезной инструмент
 Каталог Sumitomo пластины с режущей кромкой-моноалмаз Sumicristal
 Каталог Sumitomo инструмент для обработки канавок
 Общий каталог Sumitomo 2019 - 2020
 Каталог Sumitomo запасные части
- Pages 3-6_CS6_EN_web
- A 1-20 insert selection EN_web
- B 1-14 grades_EN_web
- C01-17 inserts intro pages_EN_web
- C18-56 negative inserts_EN_web
- C57-86 positive inserts_EN_web
- D 1-46 tool holders_EN_web
- E 1-24 boring bars_EN_web
- F 1-48 grooving_thread tools_EN_web
- G 1-54 milling cutters_EN_web
- H 1-48 insert type endmills_EN_web
- J 1-24 new endmills_EN_web
- J 25-50 endmills_EN_web
- K 1-46 Multi-Drills_EN_web
- K 47-76 Multi-Drills_EN_web
- L 1-28 cbn_pcd grades_EN_web
- M 1-34 cbn_pcd inserts_EN_web
- M 35-56 SHM tools_EN_web
- N1-24 technical guidance_EN_web
- P 1-8 spare parts_neu_EN_web
- P 9-22 index_notes_EN_web
Solid Carbide Drills for Deep Hole Drilling MDW XHG/XHT/PHT
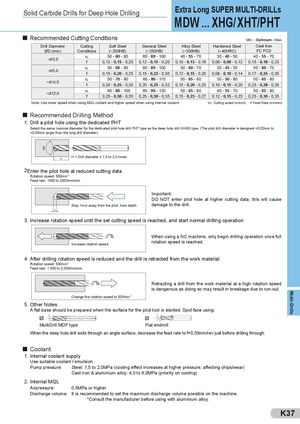
Recommended Cutting Conditions
| ug | Min. -Optimum- Max. | |||||
| Drill Diameter ØD (mm) | Cutting Conditions | Soft Steel (~200HB) | General Steel (~250HB) | Alloy Steel (~300HB) | Hardened Steel (~40HRC) | Cast Iron FC FCD |
| ~Ø30 | vc | 50 -60- 80 | 60 -80- 100 | 40 -55- 70 | 30 -40- 50 | 40 -55- 70 |
| , | f | 0,12 -0,15- 0,20 | 0,12 -0,15- 0,20 | 0,10 -0,13- 0,16 | 0,06 -0,08- 0,12 | 0,15 -0,18- 0,23 |
| ~Ø50 | vc | 50 -60- 80 | 60 -80- 100 | 50 -60- 70 | 30 -45- 55 | 50 -60- 70 |
| , | f | 0,15 -0,20- 0,25 | 0,15 -0,23- 0,30 | 0,12 -0,15- 0,20 | 0,08 -0,10- 0,14 | 0,17 -0,25- 0,35 |
| ~Ø100 | vc | 50 -70- 90 | 60 -80- 110 | 50 -65- 80 | 30 -50- 60 | 50 -65- 80 |
| , | f | 0,20 -0,25- 0,30 | 0,20 -0,25- 0,32 | 0,15 -0,20- 0,25 | 0,10 -0,15- 0,20 | 0,25 -0,28- 0,35 |
| ~Ø120 | vc | 60 -80- 100 | 60 -90- 120 | 50 -65- 80 | 40 -55- 70 | 50 -65- 80 |
| , | f | 0,25 -0,30- 0,35 | 0,25 -0,30- 0,35 | 0,15 -0,23- 0,27 | 0,12 -0,15- 0,23 | 0,25 -0,30- 0,35 |
Note: Use lower speed when using MQL coolant and higher speed when using internal coolant. Vc: Cutting speed (m/min), f: Feed Rate (mm/rev)
Recommended Drilling Method
1. Drill a pilot hole using the dedicated PHT
Select the same nominal diameter for the dedicated pilot hole drill PHT type as the deep hole drill XHGS type. (The pilot drill diameter is designed +0,02mm to +0,05mm larger than the long drill diameter)
H = Drill diameter x 1,5 to 2,0 times
2.Enter the pilot hole at reduced cutting data
Rotation speed: 500min-1, Feed rate: 1000 to 2000mm/min Important: DO NOT enter pilot hole at higher cutting data, this will cause Stop 1mm away from the pilot hole depth damage to the drill.
3. Increase rotation speed until the set cutting speed is reached, and start normal drilling operation
When using a NC machine, only begin drilling operation once full rotation speed is reached. Increase rotation speed
4. After drilling rotation speed is reduced and the drill is retracted from the work material
Rotation speed: 500min-1 Feed rate: 1.000 to 2.000mm/min Retracting a drill from the work material at a high rotation speed is dangerous as doing so may result in breakage due to run-out. Change the rotation speed to 500min-1
5. Other Notes
A flat base should be prepared when the surface for the pilot tool is slanted. Spot face using: MultiDrill MDF type Flat endmill When the deep hole drill exits through an angle surface, decrease the feed rate to f=0,05mm/rev just before drilling through.
Coolant
1. Internal coolant supply
Use suitable coolant / emulsion Pump pressure: Steel: 1,5 to 2,0MPa (cooling effect increases at higher pressure, affecting chips/wear) Cast iron & aluminium alloy: 4,0 to 6,0MPa (priority on cooling)
2. Internal MQL
Airpressure: 0,5MPa or higher Discharge volume: It is recommended to set the maximum discharge volume possible on the machine. *Consult the manufacturer before using with aluminium alloy.