Общий каталог Sumitomo 2018 - 2019 - страница 427
Навигация
 Общий каталог Sumitomo 2012
 Каталог Sumitomo резьбонарезной инструмент
 Каталог Sumitomo пластины с режущей кромкой-моноалмаз Sumicristal
 Каталог Sumitomo инструмент для обработки канавок
 Общий каталог Sumitomo 2019 - 2020
 Каталог Sumitomo запасные части
- Pages 3-6_CS6_EN_web
- A 1-20 insert selection EN_web
- B 1-14 grades_EN_web
- C01-17 inserts intro pages_EN_web
- C18-56 negative inserts_EN_web
- C57-86 positive inserts_EN_web
- D 1-46 tool holders_EN_web
- E 1-24 boring bars_EN_web
- F 1-48 grooving_thread tools_EN_web
- G 1-54 milling cutters_EN_web
- H 1-48 insert type endmills_EN_web
- J 1-24 new endmills_EN_web
- J 25-50 endmills_EN_web
- K 1-46 Multi-Drills_EN_web
- K 47-76 Multi-Drills_EN_web
- L 1-28 cbn_pcd grades_EN_web
- M 1-34 cbn_pcd inserts_EN_web
- M 35-56 SHM tools_EN_web
- N1-24 technical guidance_EN_web
- P 1-8 spare parts_neu_EN_web
- P 9-22 index_notes_EN_web
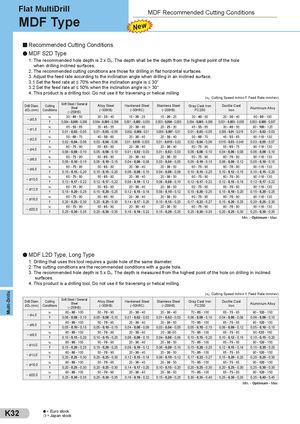
MDF Type MDF Recommended Cutting Conditions
Recommended Cutting Conditions
MDF S2D Type
1. The recommended hole depth is 2 x Dc. The depth shall be the depth from the highest point of the hole
when drilling inclined surfaces. 2. The recommended cutting conditions are those for drilling in flat horizontal surfaces. 3. Adjust the feed rate according to the inclination angle when drilling in an inclined surface.
3.1 Set the feed rate at ≤ 70% when the inclination angle is ≤ 30°
3.2 Set the feed rate at ≤ 50% when the inclination angle is:> 30°
4. This product is a drilling tool. Do not use it for traversing or helical milling
| Soft Steel / General | (vc: Cu | tting Speed m/min f: | Feed Rate mm/rev) | |||||
| Drill Diam. ØDc(mm) | Cutting Conditions | Steel (~250HB) | Alloy Steel (~300HB) | Hardened Steel (~50HRC) | Stainless Steel (~200HB) | Gray Cast Iron FC250 | Ductile Cast Iron | Aluminium Alloy |
| ~05 | vc | 30 -40- 50 | 30 -35- 40 | 15 -20- 25 | 15 -20- 25 | 30 -40- 50 | 20 -30- 40 | 60 -80- 100 |
| Ø, | f | 0,004 -0,005- 0,006 | 0,004 -0,005- 0,006 | 0,001 -0,002- 0,003 | 0,003 -0,004- 0,005 | 0,004 -0,005- 0,006 | 0,001 -0,003- 0,005 | 0,003 -0,005- 0,007 |
| 1 | vc | 45 -55- 65 | 35 -45- 55 | 20 -30- 40 | 20 -25- 30 | 45 -55- 65 | 30 -40- 50 | 80 -100- 120 |
| ~Ø,0 | f | 0,01 -0,03- 0,05 | 0,01 -0,03- 0,05 | 0,002 -0,006- 0,01 | 0,005 -0,007- 0,01 | 0,01 -0,03- 0,05 | 0,005 -0,01- 0,015 | 0,01 -0,02- 0,03 |
| vc | 50 -60- 70 | 40 -50- 60 | 20 -30- 40 | 20 -30- 40 | 50 -60- 70 | 45 -55- 65 | 90 -110- 130 | |
| ~Ø2,0 | f | 0,02 -0,04- 0,06 | 0,02 -0,04- 0,06 | 0,01 -0,018- 0,025 | 0,01 -0,015- 0,02 | 0,02 -0,04- 0,06 | 0,015 -0,03- 0,045 | 0,03 -0,05- 0,07 |
| ~40 | vc | 60 -75- 90 | 50 -65- 80 | 20 -30- 40 | 20 -30- 40 | 60 -75- 90 | 55 -65- 75 | 90 -110- 130 |
| Ø, | f | 0,06 -0,08- 0,10 | 0,05 -0,08- 0,10 | 0,01 -0,02- 0,03 | 0,01 -0,02- 0,03 | 0,06 -0,08- 0,10 | 0,04 -0,06- 0,08 | 0,06 -0,08- 0,10 |
| ~Ø60 | vc | 60 -75- 90 | 50 -65- 80 | 20 -30- 40 | 20 -30- 50 | 60 -75- 90 | 60 -70- 80 | 90 -110- 130 |
| , | f | 0,05 -0,10- 0,15 | 0,05 -0,10- 0,15 | 0,04 -0,06- 0,08 | 0,03 -0,04- 0,05 | 0,05 -0,10- 0,15 | 0,06 -0,09- 0,12 | 0,05 -0,10- 0,15 |
| ~80 | vc | 60 -75- 90 | 50 -65- 80 | 20 -30- 40 | 20 -30- 50 | 60 -75- 90 | 60 -70- 80 | 90 -110- 130 |
| Ø, | f | 0,10 -0,15- 0,20 | 0,10 -0,15- 0,20 | 0,06 -0,08- 0,10 | 0,04 -0,06- 0,08 | 0,10 -0,15- 0,20 | 0,10 -0,12- 0,15 | 0,10 -0,15- 0,20 |
| ~Ø100 | vc | 60 -75- 90 | 50 -65- 80 | 20 -30- 40 | 20 -30- 50 | 60 -75- 90 | 60 -70- 80 | 90 -110- 130 |
| , | f | 0,12 -0,17- 0,22 | 0,12 -0,17- 0,22 | 0,08 -0,10- 0,12 | 0,06 -0,08- 0,10 | 0,12 -0,17- 0,22 | 0,12 -0,15- 0,18 | 0,12 -0,17- 0,22 |
| ~Ø120 | vc | 60 -75- 90 | 50 -65- 80 | 20 -30- 40 | 20 -30- 50 | 60 -75- 90 | 60 -70- 80 | 90 -110- 130 |
| , | f | 0,15 -0,20- 0,25 | 0,15 -0,20- 0,25 | 0,12 -0,15- 0,18 | 0,08 -0,10- 0,12 | 0,15 -0,20- 0,25 | 0,15 -0,18- 0,20 | 0,15 -0,20- 0,25 |
| vc | 60 -75- 90 | 50 -65- 80 | 20 -30- 40 | 20 -30- 50 | 60 -75- 90 | 60 -70- 80 | 90 -110- 130 | |
| ~Ø16,0 | f | 0,20 -0,25- 0,30 | 0,20 -0,25- 0,30 | 0,14 -0,17- 0,20 | 0,10 -0,15- 0,20 | 0,17 -0,22- 0,27 | 0,15 -0,20- 0,25 | 0,20 -0,25- 0,30 |
| ~200 | vc | 60 -75- 90 | 50 -65- 80 | 20 -30- 40 | 20 -30- 50 | 60 -75- 90 | 60 -70- 80 | 90 -110- 130 |
| Ø, | f | 0,25 -0,30- 0,35 | 0,25 -0,30- 0,35 | 0,16 -0,19- 0,22 | 0,15 -0,20- 0,25 | 0,25 -0,30- 0,35 | 0,20 -0,25- 0,30 | 0,25 -0,30- 0,35 |
| Min | . -Optimum- Max. |
MDF L2D Type, Long Type
1. Drilling that uses this tool requires a guide hole of the same diameter. 2. The cutting conditions are the recommended conditions with a guide hole. 3. The recommended hole depth is 5 x Dc. The depth is measured from the highest point of the hole on drilling in inclined surfaces. 4. This product is a drilling tool. Do not use it for traversing or helical milling.
| (vc: Cu | tting Speed m/min f | : Feed Rate mm/rev) | ||||||
| Drill Diam. ØDc(mm) | Cutting Conditions | Soft Steel / General Steel (~250HB) | Alloy Steel (~300HB) | Hardened Steel (~50HRC) | Stainless Steel (~200HB) | Gray Cast Iron FC250 | Ductile Cast Iron | Aluminium Alloy |
| vc | 60 -80- 100 | 50 -70- 90 | 20 -30- 40 | 20 -30- 40 | 70 -85- 100 | 65 -75- 85 | 90 -120- 150 | |
| ~Ø4,0 | f | 0,06 -0,08- 0,10 | 0,05 -0,08- 0,10 | 0,01 -0,02- 0,03 | 0,01 -0,02- 0,03 | 0,06 -0,08- 0,10 | 0,04 -0,06- 0,08 | 0,06 -0,08- 0,10 |
| vc | 60 -80- 100 | 50 -70- 90 | 20 -30- 40 | 20 -30- 50 | 70 -85- 100 | 65 -75- 85 | 90 -120- 150 | |
| ~Ø6,0 | f | 0,05 -0,10- 0,15 | 0,05 -0,10- 0,15 | 0,04 -0,06- 0,08 | 0,03 -0,04- 0,05 | 0,05 -0,10- 0,15 | 0,06 -0,09- 0,12 | 0,05 -0,10- 0,15 |
| vc | 60 -80- 100 | 50 -70- 90 | 20 -30- 40 | 20 -30-50 | 70 -85- 100 | 65 -75- 85 | 90 -120- 150 | |
| ~Ø8,0 | f | 0,10 -0,15- 0,20 | 0,10 -0,15- 0,20 | 0,06 -0,08- 0,10 | 0,04 -0,06- 0,08 | 0,10 -0,15- 0,20 | 0,10 -0,12- 0,15 | 0,10 -0,15- 0,20 |
| vc | 60 -80- 100 | 50 -70- 90 | 20 -30- 40 | 20 -30- 50 | 70 -85- 100 | 65 -75- 85 | 90 -120- 150 | |
| ~Ø10,0 | f | 0,15 -0,20- 0,25 | 0,15 -0,20- 0,25 | 0,08 -0,10- 0,12 | 0,06 -0,08- 0,10 | 0,15 -0,20- 0,25 | 0,12 -0,15- 0,18 | 0,15 -0,20- 0,25 |
| vc | 60 -80- 100 | 50 -70- 90 | 20 -30- 40 | 20 -30- 50 | 70 -85- 100 | 65 -75- 85 | 90 -120- 150 | |
| ~Ø12,0 | f | 0,20 -0,25- 0,30 | 0,20 -0,25- 0,30 | 0,12 -0,15- 0,18 | 0,08 -0,10- 0,12 | 0,17 -0,22- 0,27 | 0,15 -0,20- 0,25 | 0,20 -0,25- 0,30 |
| vc | 60 -80- 100 | 50 -70- 90 | 20 -30- 40 | 20 -30- 50 | 70 -85- 100 | 65 -75- 85 | 90 -120- 150 | |
| ~Ø16,0 | f | 0,20 -0,25- 0,30 | 0,20 -0,25- 0,30 | 0,14 -0,17- 0,20 | 0,10 -0,15- 0,20 | 0,20 -0,25- 0,30 | 0,20 -0,25- 0,30 | 0,25 -0,30- 0,35 |
| 2 | vc | 60 -80- 100 | 50 -70- 90 | 20 -30- 40 | 20 -30- 50 | 70 -85- 100 | 65 -75- 85 | 90 -120- 150 |
| ~Ø0,0 | f | 0,25 -0,30- 0,35 | 0,25 -0,30- 0,35 | 0,16 -0,19- 0,22 | 0,15 -0,20- 0,25 | 0,30 -0,35- 0,40 | 0,25 -0,30- 0,35 | 0,35 -0,40- 0,45 |
Min. - Optimum - Max.