Общий каталог Sumitomo 2018 - 2019 - страница 339
Навигация
 Общий каталог Sumitomo 2012
 Каталог Sumitomo резьбонарезной инструмент
 Каталог Sumitomo пластины с режущей кромкой-моноалмаз Sumicristal
 Каталог Sumitomo инструмент для обработки канавок
 Общий каталог Sumitomo 2019 - 2020
 Каталог Sumitomo запасные части
- Pages 3-6_CS6_EN_web
- A 1-20 insert selection EN_web
- B 1-14 grades_EN_web
- C01-17 inserts intro pages_EN_web
- C18-56 negative inserts_EN_web
- C57-86 positive inserts_EN_web
- D 1-46 tool holders_EN_web
- E 1-24 boring bars_EN_web
- F 1-48 grooving_thread tools_EN_web
- G 1-54 milling cutters_EN_web
- H 1-48 insert type endmills_EN_web
- J 1-24 new endmills_EN_web
- J 25-50 endmills_EN_web
- K 1-46 Multi-Drills_EN_web
- K 47-76 Multi-Drills_EN_web
- L 1-28 cbn_pcd grades_EN_web
- M 1-34 cbn_pcd inserts_EN_web
- M 35-56 SHM tools_EN_web
- N1-24 technical guidance_EN_web
- P 1-8 spare parts_neu_EN_web
- P 9-22 index_notes_EN_web
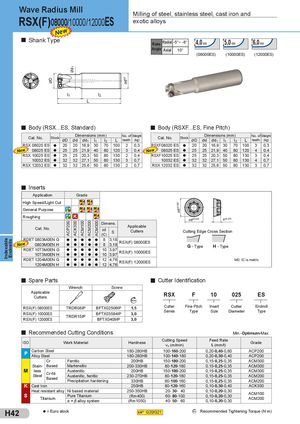
| RSX(F) | ES | Milling of steel, stainless steel, cast iron and | |
| 08000/10000/12000 | exotic alloys |
Shank Type 4,0 5,0 6,0
Rake Radial -5°~ -8° mm mm mm
Angle Axial 10°
(08000ES) (10000ES) (12000ES)
l1 l2 L
Body (RSX...ES, Standard) Body (RSXF...ES, Fine Pitch)
| Cat No | Stock | Di | mensio | ns(m | m) | No. of | Weight | Cat No | Stock | Di | mensio | ns(m | m) | No. of | Weight | ||||
| . . | ØD | Ød | Ød1 | l1 | l2 | L | teeth | (kg) | . . | ØD | Ød | Ød1 | l1 | l2 | L | teeth | (kg) | ||
| RSX 08020 ES | l | 20 | 20 | 16,9 | 30 | 70 | 100 | 2 | 0,3 | RSXF08020 ES | l | 20 | 20 | 16,9 | 30 | 70 | 100 | 3 | 0,3 |
| 08025 ES New | l | 25 | 25 | 21,9 | 40 | 80 | 120 | 3 | 0,4 | 08025 ES New | l | 25 | 25 | 21,9 | 40 | 80 | 120 | 4 | 0,4 |
| RSX 10025 ES | l | 25 | 25 | 20,3 | 50 | 80 | 130 | 2 | 0,4 | RSXF10025 ES | l | 25 | 25 | 20,3 | 50 | 80 | 130 | 3 | 0,4 |
| 10032 ES | l | 32 | 32 | 27,1 | 50 | 80 | 130 | 3 | 0,7 | 10032 ES | l | 32 | 32 | 27,1 | 50 | 80 | 130 | 4 | 0,7 |
| RSX 12032 ES | l | 32 | 32 | 25,6 | 50 | 80 | 130 | 2 | 0,7 | RSX 12032 ES | l | 32 | 32 | 25,6 | 50 | 80 | 130 | 3 | 0,7 |
Inserts
Application Grade High Speed/Light Cut General Purpose P M
Roughing P K
| M | d | s | |||
| Ø ±0,025 | ±0,025 | ||||
| Dimens. | |||||
| Applicable | |||||
| Cat. No. | d |
| Ø | Cutters | Cutting Edge Cross Section |
| (IC) S |
RDET 0803M0EN G lllll 8 3,18 RSX(F) 08000ES
| New | 0803M0EN H | lllll | 8 3,18 | G - Type | H - Type | |||
| RDET 10T3M0EN G | lllll | 10 3,97 RSX(F) 10000ES | ||||||
| Indexable Endmills | 10T3M0EN H | lllll | 10 3,97 | |||||
| RDET 1204M0EN G | lllll | 12 4,76 RSX(F) 12000ES | M0: IC is metric | |||||
| 1204M0EN H | lllll | 12 4,76 |
Spare Parts Cutter Identification
| Wrench | Screw | ||
| Applicable Cutters | |||
| RSX(F)08000ES | TRDR08IP | BFTX02506IP | 1,5 |
| RSX(F)10000ES | TRDR15IP | BFTX03584IP | 3,0 |
| RSX(F)12000ES | BFTX0409IP | 3,0 |
Recommended Cutting Conditions Min.-Optimum-Max.
| ISO | W | ork Material | Hardness | Cutting Speed vc(m/min) | Feed Rate ft(mm/t) | Grade |
| P | Carbon Steel | 180-280HB | 100-160-200 | 0,20-0,40-0,60 | ACP200 | |
| AlloySteel | 180-280HB | 100-140-180 | 0,20-0,30-0,40 | ACP200 | ||
| Cr | Ferritic | 200HB | 150-180-200 | 0,15-0,25-0,35 | ACM300 | |
| Based Stain- | Martensitic | 200-330HB | 80-120-180 | 0,15-0,25-0,35 | ACM300 | |
| M | CNi less | Austenitic | 200HB | 150-180-200 | 0,15-0,25-0,35 | ACM300 |
| r- Bd Steel | Austenitic,ferritic | 230-270HB | 80-120-180 | 0,15-0,25-0,35 | ACM200 | |
| ase | Precipitation hardening | 330HB | 60-100-160 | 0,15-0,25-0,35 | ACM200 | |
| K | Cast Iron | 250HB | 80-120-160 | 0,10-0,30-0,40 | ACK300 | |
| Heat resistant alloy | Ni based material | 250-350HB | 20-30- 40 | 0,10-0,20-0,30 | ACM100 | |
| S | Titi | Pure Titanium | (Rm400) | 60-80-100 | 0,10-0,20-0,30 | ACM200 |
| anum | α +β alloysystem | (Rm1050) | 40-50-60 | 0,10-0,20-0,30 |