Общий каталог Sumitomo 2018 - 2019 - страница 323
Навигация
 Общий каталог Sumitomo 2012
 Каталог Sumitomo резьбонарезной инструмент
 Каталог Sumitomo пластины с режущей кромкой-моноалмаз Sumicristal
 Каталог Sumitomo инструмент для обработки канавок
 Общий каталог Sumitomo 2019 - 2020
 Каталог Sumitomo запасные части
- Pages 3-6_CS6_EN_web
- A 1-20 insert selection EN_web
- B 1-14 grades_EN_web
- C01-17 inserts intro pages_EN_web
- C18-56 negative inserts_EN_web
- C57-86 positive inserts_EN_web
- D 1-46 tool holders_EN_web
- E 1-24 boring bars_EN_web
- F 1-48 grooving_thread tools_EN_web
- G 1-54 milling cutters_EN_web
- H 1-48 insert type endmills_EN_web
- J 1-24 new endmills_EN_web
- J 25-50 endmills_EN_web
- K 1-46 Multi-Drills_EN_web
- K 47-76 Multi-Drills_EN_web
- L 1-28 cbn_pcd grades_EN_web
- M 1-34 cbn_pcd inserts_EN_web
- M 35-56 SHM tools_EN_web
- N1-24 technical guidance_EN_web
- P 1-8 spare parts_neu_EN_web
- P 9-22 index_notes_EN_web
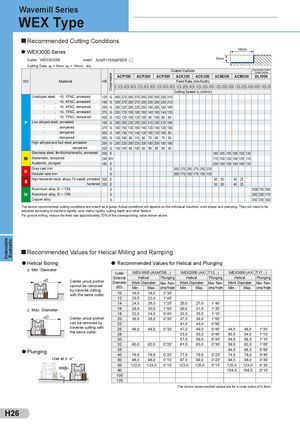
WEX Type
Recommended Cutting Conditions
WEX3000 Series 16mm
| Cutter: WEX30325E | Insert: AXMT170508PEER - | 5mm | ||
| Cutting Data: ap = 5mm, ae = 16mm, dry | ||||
| Coated Carbide | „Diamond like Carbon“ | |||
| Coated Carbide |
ACP100 ACP200 ACP300 ACK200 ACK300 ACM200 ACM300 DL1000
| ISO | Material | HB | Feed Rate (mm/tooth) | ||
| 0,12 0,25 0,35 0,12 0,25 0,35 0,12 0,25 0,35 0,12 0,25 0,35 0,12 0,25 0,35 0,12 0,25 0,35 0,12 0,25 0,35 0,05 0,15 0,25 | |||||
| Cutting Speed vc (m/min) | |||||
| Unalloyed steel, <0, 15%C, annealed | 125 G 400 370 350 370 350 330 350 330 310 |
- , <0, 45%C, annealed 190 G 300 270 250 270 250 230 250 230 210
- , <0, 45%C, tempered 250 G 250 220 200 220 200 180 200 180 160
- , <0, 75%C, annealed 270 G 200 170 150 180 160 140 160 140 120
- , <0, 75%C, tempered 300 G 150 120 100 120 100 80 100 80 60
P Low alloyed steel, annealed 180 G 280 250 230 250 230 210 230 210 190
- , tempered 275 G 180 150 130 160 140 120 140 120 100
- , tempered 300 G 160 130 110 140 120 100 120 100 80
- , tempered 350 G 130 100 80 110 90 70 90 70 50
High alloyed and tool steel, annealed 200 G 250 220 200 220 200 180 200 180 160
- , tempered 325 G 130 100 80 100 80 60 80 60 40
| Stainless steel, ferritic/martensitic, annealed | 200 E | 185 165 135 165 150 120 | |||||
| M | Martensitic, tempered | 240 EH | 170 150 120 150 135 110 | ||||
| Austenitic, plunged | 180 E | 200 180 150 180 160 135 | |||||
| K | Grey cast iron | G | 300 270 250 270 250 230 | ||||
| Nodular cast iron | G | 200 170 150 170 150 130 | |||||
| S | High tempered resist. alloys, Fe based, annealed 300 E | 50 30 | 45 25 | ||||
| „ , hardened 330 E | 50 30 | 45 25 | |||||
| Aluminium alloy, Si < 13% | S | 1000 750 500 | |||||
| N | Aluminium alloy, Si > 13% | S | 250 200 170 | ||||
| Copper alloy | S | 350 330 300 |
The above recommended cutting conditions are meant as a guide. Actual conditions will depend on the individual machine, work shape and clamping. They will need to be adjusted according to machine rigidity, work clamp rigidity, cutting depth and other factors. For groove milling, reduce the feed rate approximately 70% of the corresponding value shown above.
Recommended Values for Helical Milling and Ramping
Indexable Endmills
Helical Boring Recommended Values for Helical and Plunging
≤ Min. Diameter
Cutter WEX1000 (AXMT06...) WEX2000 (AX T12...) WEX3000 (AX T17...)
External Helical Plunging Helical Plunging Helical Plunging
ø Center uncut portion Diameter Work Diameter Work Diameter Work Diameter
Max. Ram- Max. Ram- Max. Ram-
| cannot be removed | ØD | Min. | Max. | ping Angle | Min. | Max. | ping Angle | Min. | Max. | ping Angle | |
| by traverse cutting | c | ||||||||||
| with the same cutter. | 10 | 16,0 | 18,0 | 2°30' | |||||||
| 12 | 20,0 | 22,0 | 1°45' | ||||||||
| 14 | 24,0 | 26,0 | 1°25' | 25,0 | 27,0 | 1°40' | |||||
| ≥ Max. Diameter | 16 | 28,0 | 30,0 | 1°00' | 29,0 | 31,0 | 1°20' | ||||
| 18 | 32,0 | 34,0 | 0°45' | 33,0 | 35,0 | 1°10' | |||||
| ø Center uncut portion | 20 | 36,0 | 38,0 | 0°30' | 37,0 | 39,0 | 1°00' | ||||
| can be removed by | 22 | 41,0 | 43,0 | 0°50' | |||||||
| traverse cutting with | 25 | 46,0 | 48,0 | 0°30' | 47,0 | 49,0 | 0°45' | 44,5 | 48,0 | 1°30' | |
| the same cutter. | |||||||||||
| 28 | 53,0 | 55,0 | 0°45' | 50,5 | 54,0 | 1°10' | |||||
| 30 | 57,0 | 59,0 | 0°40' | 54,5 | 58,0 | 1°10' | |||||
| 32 | 60,0 | 62,0 | 0°25' | 61,0 | 63,0 | 0°35' | 58,5 | 62,0 | 1°00' | ||
| Plunging | 35 | 64,5 | 68,0 | 0°50' | |||||||
| 40 | 76,0 | 78,0 | 0°20' | 77,0 | 79,0 | 0°25' | 74,5 | 78,0 | 0°45' | ||
| Use at ≤ α° | 50 | 96,0 | 98,0 | 0°15' | 97,0 | 99,0 | 0°20' | 94,5 | 98,0 | 0°30' | |
| 63 | 122,0 | 124,0 | 0°10' | 123,0 | 125,0 | 0°15' | 120,5 | 124,0 | 0°20' | ||
| 80 | 154,5 | 158,0 | 0°15' |
100 125 The above recommended values are for a nose radius of 0,8mm.