”METAL SLASH MILL”
MSX Type
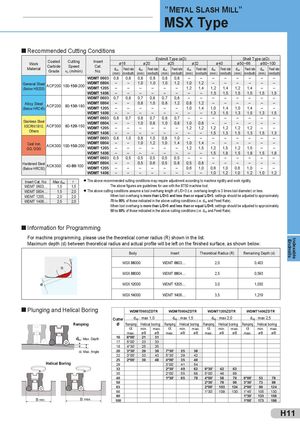
Recommended Cutting Conditions
| Ctd | Ctti | It | | | | En | dmill | Type (ø | D) | | | | | Shell Ty | pe (øD | ) |
| Work | oae Carbide | ung Seed | nser Cat | ø | 16 | ø | 20 | ø | 25 | ø | 32 | ø | 40 | ø50 | ~66 | ø80 | ~100 |
| Material | Grade | p vc(m/min) | . No. | doc (mm) | Feed rate (mm/tooth) | doc (mm) | Feed rate (mm/tooth) | doc (mm) | Feed rate (mm/tooth) | doc (mm) | Feed rate (mm/tooth) | doc (mm) | Feed rate (mm/tooth) | doc (mm) | Feed rate (mm/tooth) | doc (mm) | Feed rate (mm/tooth) |
| | | WDMT 0603 | 0,8 | 0,8 | 0,8 | 0,8 | 0,8 | 0,8 | – | – | – | – | – | – | – | – |
| General Steel | | | WDMT 0804 | – | – | 1,0 | 1,0 | 1,0 | 1,2 | 1,0 | 1,2 | – | – | – | – | – | – |
| (Below HB200) | ACP200 | 00-150-200 | WDMT 1205 | – | – | – | – | – | – | 1,2 | 1,4 | 1,2 | 1,4 | 1,2 | 1,4 | – | – |
| | | WDMT 1406 | – | – | – | – | – | – | – | – | 1,5 | 1,5 | 1,5 | 1,5 | 1,5 | 1,5 |
| | | WDMT 0603 | 0,7 | 0,8 | 0,7 | 0,8 | 0,7 | 0,8 | – | – | – | – | – | – | – | – |
| Alloy Steel | | | WDMT 0804 | – | – | 0,8 | 1,0 | 0,8 | 1,2 | 0,8 | 1,2 | – | – | – | – | – | – |
| (Below HRC45) | ACP200 | 80-130-180 | WDMT 1205 | – | – | – | – | – | – | 1,0 | 1,4 | 1,0 | 1,4 | 1,0 | 1,4 | – | – |
| | | WDMT 1406 | – | – | – | – | – | – | – | – | 1,3 | 1,5 | 1,3 | 1,5 | 1,3 | 1,5 |
| | | WDMT 0603 | 0,8 | 0,7 | 0,8 | 0,7 | 0,8 | 0,7 | – | – | – | – | – | – | – | – |
| Stainless Steel | | | WDMT 0804 | – | – | 1,0 | 0,8 | 1,0 | 0,8 | 1,0 | 0,8 | – | – | – | – | – | – |
| X5CRNI1810, | ACP300 | 80-120-150 | WDMT 1205 | – | – | – | – | – | – | 1,2 | 1,2 | 1,2 | 1,2 | 1,2 | 1,2 | – | – |
| Others | | | WDMT 1406 | – | – | – | – | – | – | – | – | 1,5 | 1,3 | 1,5 | 1,3 | 1,5 | 1,3 |
| | | WDMT 0603 | 0,8 | 1,0 | 0,8 | 1,0 | 0,8 | 1,0 | – | – | – | – | – | – | – | – |
| Cast Iron | | | WDMT 0804 | – | – | 1,0 | 1,2 | 1,0 | 1,4 | 1,0 | 1,4 | – | – | – | – | – | – |
| GG, GGG | ACK300 | 00-150-200 | WDMT 1205 | – | – | – | – | – | – | 1,2 | 1,5 | 1,2 | 1,5 | 1,2 | 1,5 | – | – |
| | | WDMT 1406 | – | – | – | – | – | – | – | – | 1,5 | 1,8 | 1,5 | 1,8 | 1,5 | 1,8 |
| | | WDMT 0603 | 0,5 | 0,5 | 0,5 | 0,5 | 0,5 | 0,5 | – | – | – | – | – | – | – | – |
| Hardened Steel | | | WDMT 0804 | – | – | 0,5 | 0,6 | 0,5 | 0,8 | 0,5 | 0,8 | – | – | – | – | – | – |
| (Below HRC50) | ACK300 | 40-80-100 | WDMT 1205 | – | – | – | – | – | – | 0,6 | 1,0 | 0,6 | 1,0 | 0,6 | 1,0 | – | – |
| | | WDMT 1406 | – | – | – | – | – | – | – | – | 10 | 12 | 10 | 12 | 10 | 12 |
| WDMT0603.. Insert Cat. No | .. 1,0 Max do . | 1,5 r l c | The above reco i | mmende The abo i | d cutting ve figure | conditi is are gu | ons may r i idelines f | equire a i or use w | djustmen i ith the B | t accor i T50 ma | ding to ma i chine tool | , chine ri i . | , gidity and | , work ri | , gidity. | , | , |
| WDMT0804.. | .. 1,5 | 2,0 l | i The above cutti | i ng condi | i tions ass | i umeat | i ool overha | i ng leng | i th of L/D | i =3 (i.e. | i overhang | i length i | s 3 times | tool dia | meter) or | less. | |
| WDMT 1205.. | .. 2,0 | 2,0 | | When to | ol overha | ng ism | ore than | L/D=3 | and less | than or | equal L/ | D=5, se | ttings sho | uld be a | djusted t | o appro | ximately |
| WDMT 1406.. | .. 2,5 | 2,0 | | 70 to 80 When to 50 to 60 | %of thos ol overha %of thos | e indic ng ism e indic | ated in the ore than ated in the | above L/D=5 above | cutting c and less cutting c | ondition than or ondition | s (i.e. doc equal L/ s (i.e. doc | and Fe D=8, se and Fe | ed Rate). ttings sho ed Rate). | uld be a | djusted t | o appro | ximately |
Information for Programming
For machine programming, please use the theoretical corner radius (R) shown in the list. Maximum depth (d) between theoretical radius and actual profile will be left on the finished surface, as shown below.
| Body | Insert | Theoretical Radius (R) | Remaining Depth (d) |
| MSX06000 | WDMT0603.... | 2,0 | 0,403 |
| MSX08000 | WDMT0804.... | 2,5 | 0,593 |
| d | MSX12000 | WDMT1205.... | 3,0 | 1,030 |
| MSX14000 | WDMT1406.... | 3,5 | 1,219 |
Plunging and Helical Boring
| WDM | T0603Z | DTR | WDM | T0804Z | DTR | WDM | T1205Z | DTR | WDM | T1406Z | DTR |
| Cutter | doc | : max 1 | ,0 | doc | : max 1 | ,5 | doc | : max 2 | ,0 | doc | : max 2 | ,5 |
| Ø | Ramping | Helical | boring | Ramping | Helical | boring | Ramping | Helical | boring | Ramping | Helical | boring |
| a max. | min. øB | max. øB | a max. | min. øB | max. øB | a max. | min. øB | max. øB | a max. | min. øB | max. øB |
| 16 | 6°00’ | 21 | 31 | | | | | | | | | |
| 17 | 5°00’ | 23 | 33 | | | | | | | | | |
| 18 | 4°30’ | 25 | 35 | | | | | | | | | |
| 20 | 3°30’ | 29 | 39 | 7°30’ | 25 | 38 | | | | | | |
| 22 | 3°00’ | 33 | 43 | 5°30’ | 29 | 42 | | | | | | |
| 25 | 2°00’ | 39 | 48 | 4°00’ | 35 | 48 | | | | | | |
| 28 | | | | 3°00’ | 41 | 54 | | | | | | |
| 32 | | | | 2°30’ | 49 | 62 | 6°30’ | 42 | 63 | | | |
| 35 | | | | 2°00’ | 55 | 68 | 5°00’ | 48 | 69 | | | |
| 40 | | | | 1°30’ | 65 | 78 | 4°00’ | 58 | 79 | 6°00’ | 53 | 78 |
| 50 | | | | | | | 2°30’ | 78 | 99 | 3°30’ | 73 | 98 |
| 63 | | | | | | | 2°00’ | 103 | 124 | 2°00’ | 99 | 124 |
| 66 | | | | | | | 1°30’ | 109 | 130 | 1°45’ | 105 | 130 |
| 80 | | | | | | | | | | 1°30’ | 133 | 158 |
| 100 | | | | | | | | | | 1°00’ | 173 | 198 |
 Общий каталог Sumitomo 2012
 Каталог Sumitomo резьбонарезной инструмент
 Каталог Sumitomo пластины с режущей кромкой-моноалмаз Sumicristal
 Каталог Sumitomo инструмент для обработки канавок
 Общий каталог Sumitomo 2019 - 2020
 Каталог Sumitomo запасные части