Общий каталог Sumitomo 2018 - 2019 - страница 303
Навигация
 Общий каталог Sumitomo 2012
 Каталог Sumitomo резьбонарезной инструмент
 Каталог Sumitomo пластины с режущей кромкой-моноалмаз Sumicristal
 Каталог Sumitomo инструмент для обработки канавок
 Общий каталог Sumitomo 2019 - 2020
 Каталог Sumitomo запасные части
- Pages 3-6_CS6_EN_web
- A 1-20 insert selection EN_web
- B 1-14 grades_EN_web
- C01-17 inserts intro pages_EN_web
- C18-56 negative inserts_EN_web
- C57-86 positive inserts_EN_web
- D 1-46 tool holders_EN_web
- E 1-24 boring bars_EN_web
- F 1-48 grooving_thread tools_EN_web
- G 1-54 milling cutters_EN_web
- H 1-48 insert type endmills_EN_web
- J 1-24 new endmills_EN_web
- J 25-50 endmills_EN_web
- K 1-46 Multi-Drills_EN_web
- K 47-76 Multi-Drills_EN_web
- L 1-28 cbn_pcd grades_EN_web
- M 1-34 cbn_pcd inserts_EN_web
- M 35-56 SHM tools_EN_web
- N1-24 technical guidance_EN_web
- P 1-8 spare parts_neu_EN_web
- P 9-22 index_notes_EN_web
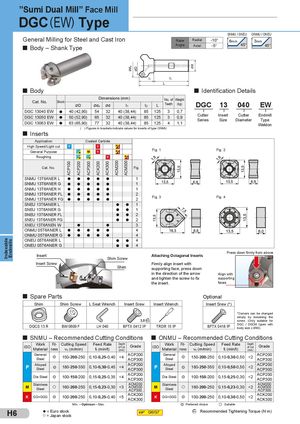
”Sumi Dual Mill” Face Mill
DGC(EW) Type
SNMU / SNEU ONMU / ONEU
General Milling for Steel and Cast Iron Radial -10°
Rake 6mm 3mm
Body – Shank Type Angle Axial -5° 45° 45°
l l2 1 L
Body Identification Details
Dimensions (mm) No. of Weight
Cat. No. Stock DGC 13 040 EW
| ØD | Ød | Ød | l | (kg) Teeth L l | ||||
| 4 | 1 | 2 | ||||||
| DGC 13040 EW | l 40 (42,90) | 54 | 32 | 40 (38,44) | 0,7 3 125 85 | |||
| DGC 13050 EW | 50 (52,90) | 65 | 32 | 40 (38,44) | Endmill Cutter Insert Cutter 0,9 3 125 85 | |||
| l | Type Diameter Size Series | |||||||
| DGC 13063 EW | l 63 (65,90) | 77 | 32 | 40 (38,44) | Weldon 1,1 4 125 85 | |||
| Inserts | ( ) Figures in brackets indicate values for inserts of type ONMU | |||||||
| Application | Coated Carbide | |||||||
| High Speed/Light cut P | K | M | ||||||
| S | Fig. 2 Fig. 1 | |||||||
| General Purpose | P | M | K | M | ||||
| M | S | |||||||
| Roughing | P | P | K | M | ||||
| M | M | S | ||||||
| Cat. No. | Fig. | |||||||
| SNMU 13T6ANER L | l | l | l | l | l | 1 | ||
| SNMU 13T6ANER G | l | l | l | l | l | 1 | ||
| SNMU 13T6ANER H | l | l | l | l | l | 1 | ||
| SNMU 13T6ANER FL | l | l | l | l | l | 2 | ||
| SNMU 13T6ANER FG | Fig. 4 Fig. 3 2 | |||||||
| l | l | l | l | l | ||||
| SNEU 13T6ANER L | l | l | 1 | |||||
| SNEU 13T6ANER G | l | l | 1 | |||||
| SNEU 13T6ANER FL | l | l | 2 | |||||
| SNEU 13T6ANER FG | l | l | 2 | |||||
| XNEU 13T6ANEN W | l | l | 3 | |||||
| ONMU 05T6ANER L | l | l | l | l | l | 4 | ||
| ONMU 05T6ANER G | l | l | l | l | l | 4 | ||
| ONEU 05T6ANER L | l | l | 4 | |||||
| ONEU 05T6ANER G | l | l | 4 | |||||
| Press down firmly from above | ||||||||
| Indexable Endmills | Insert | Attaching Octagonal Inserts |
Shim Screw Insert Screw Firmly align insert with Shim supporting face, press down in the direction of the arrow Align with
and tighten the screw to fix supporting the insert. faces
Spare Parts Optional
| Shim Shim Screw | L Seat Wrench Insert Srew | Insert Wrench | Insert Srew (*) | ||
| *Corners can be changed | |||||
| simply by loosening the | |||||
| 3,0 | screw. (Only suitable for | ||||
| DGCS 13 R | BW 0609 F | LH 040 BFTX 0412 IP | TRDR 15 IP | BFTX 0418 IP | DGC / DGCM types with |
| body size ≥ Ø80). | |||||
| SNMU – Recommended Cutting Conditions | ONMU – Recommended Cutting Conditions |
Work Fit- Cutting Speed Feed Rate Depth Work Fit- Cutting Speed Feed Rate Depth
ISO of Cut Grade ISO of Cut Grade
| Material | ness vc (m/min) | (mm) ft (min/t) | Material | ness vc (m/min) | (mm) ft (min/t) | ||
| General | 150-200-250 0,10-0,25-0,40 <4 ACP200 | General | 150-200-250 0,10-0,30-0,50 <2 ACP200 | ||||
| Steel | ACP300 | Steel | ACP300 | ||||
| P | Alloyed | 180-250-350 0,10-0,30-0,45 <4 ACP200 | P | Alloyed | 180-250-350 0,10-0,50-0,50 <2 ACP200 | ||
| Steel | ACP300 | Steel | ACP300 | ||||
| Die Steel | 100-150-200 0,15-0,25-0,35 <4 ACP200 | Die Steel | 100-150-200 0,15-0,25-0,30 <2 ACP200 | ||||
| ACP300 | ACP300 | ||||||
| Stainless | ACM200 | Stainless | ACM200 | ||||
| M | Steel | 160-200-250 0,15-0,23-0,30 <3 | ACM300 | M | Steel | 160-200-250 0,15-0,23-0,30 <2 | ACM300 |
| ACP300 | ACP300 | ||||||
| K | GG+GGG | 100-200-250 0,10-0,25-0,40 <5 ACK200 | K | GG+GGG | 100-200-250 0,10-0,30-0,50 <2 ACK200 | ||
| ACK300 | ACK300 |
Min. – Optimum – Max. Preferred choice Suitable