Общий каталог Sumitomo 2018 - 2019 - страница 285
Навигация
 Общий каталог Sumitomo 2012
 Каталог Sumitomo резьбонарезной инструмент
 Каталог Sumitomo пластины с режущей кромкой-моноалмаз Sumicristal
 Каталог Sumitomo инструмент для обработки канавок
 Общий каталог Sumitomo 2019 - 2020
 Каталог Sumitomo запасные части
- Pages 3-6_CS6_EN_web
- A 1-20 insert selection EN_web
- B 1-14 grades_EN_web
- C01-17 inserts intro pages_EN_web
- C18-56 negative inserts_EN_web
- C57-86 positive inserts_EN_web
- D 1-46 tool holders_EN_web
- E 1-24 boring bars_EN_web
- F 1-48 grooving_thread tools_EN_web
- G 1-54 milling cutters_EN_web
- H 1-48 insert type endmills_EN_web
- J 1-24 new endmills_EN_web
- J 25-50 endmills_EN_web
- K 1-46 Multi-Drills_EN_web
- K 47-76 Multi-Drills_EN_web
- L 1-28 cbn_pcd grades_EN_web
- M 1-34 cbn_pcd inserts_EN_web
- M 35-56 SHM tools_EN_web
- N1-24 technical guidance_EN_web
- P 1-8 spare parts_neu_EN_web
- P 9-22 index_notes_EN_web
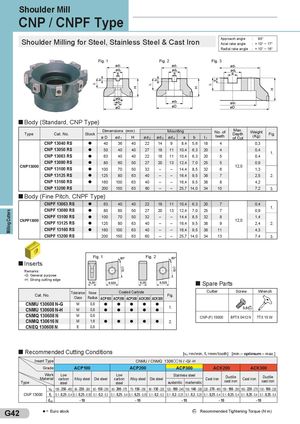
Shoulder Mill
CNP / CNPF Type
| Shoulder Milling for Steel, Stainless Steel & Cast Iron | Approach angle | : 90° |
| Axial rake angle | : + 10° ~ 17° | |
| Radial rake angle : + 10° ~ 16° |
Fig. 1 Fig. 2 Fig. 3
Body (Standard, CNP Type)
| Dimensions (mm) | Mounting | No. of | Max. | Weight | ||||
| Type | Cat. No. | Stock | teeth | Depth | (Kg) | Fig. |
ø D ød H ød ød ød a b l of Cut
1 2 3 4 1
| CNP 13040 RS | l | 40 36 40 22 14 9 8,4 5,6 18 | 4 | 0,3 | |
| CNP 13050 RS | l | 50 40 40 27 18 11 10,4 6,3 20 | 4 | 0,4 | |
| 1. | |||||
| CNP 13063 RS | l | 63 40 40 22 18 11 10,4 6,3 20 | 5 | 0,4 | |
| CNP 13080 RS | l | 80 60 50 27 20 13 12,4 7,0 25 | 5 | 0,9 |
CNP13000 CNP 13100 RS 12,0
| l | 100 70 50 32 – – 14,4 8,5 32 6 | 1,3 | ||||
| CNP 13125 RS | l | 125 80 63 40 – – 16,4 9,5 38 7 | 2,5 | 2. | ||
| CNP 13160 RS | l | 160 100 63 40 – – 16,4 9,5 38 8 | 4,2 | |||
| CNP 13200 RS | 200 150 63 60 – – 25,7 14,0 34 10 | 7,2 | 3. | |||
| Body (Fine Pitch, CNPF Type) | ||||||
| CNPF 13063 RS | l | 63 40 40 22 18 11 10,4 6,3 20 | 7 | 0,4 | ||
| CNPF 13080 RS | 1. | |||||
| l | 80 60 50 27 20 13 12,4 7,0 25 | 7 | 0,9 | |||
| CNPF 13100 RS | l | 100 70 50 32 – – 14,4 8,5 32 8 | 1,4 |
CNPF13000 CNPF 13125 RS 12,0
| l | 125 80 63 40 – – 16,4 9,5 38 9 | 2,4 | 2. | |
| CNPF 13160 RS | l | 160 100 63 40 – – 16,4 9,5 38 11 | 4,3 | |
| CNPF 13200 RS | 200 150 63 60 – – 25,7 14,0 34 13 | 7,4 | 3. |
Fig. 1 Fig. 2
Inserts
Remarks: -G: General purpose -H: Strong cutting edge Spare Parts
| Tolerance | Nose | Coated Carbide | Cutter | Screw Wrench | |||
| Cat. No. | Fig. | ||||||
| Class | Radius | ACP100 ACP200 ACP300 ACK200 ACK300 |
CNMU 130608 N-G M 0,8 l l l l l
CNMU 130608 N-H 1. 3,0
| M | 0,8 | l | l | l | l | l | ||||
| CNMQ 130608 N | M | 0,8 | ||||||||
| CNP-(F) 13000 | BFTX 0412 N TTX 15 W | |||||||||
| CNMQ 130616 N | M | 1,6 | l | l | l | l | l | 2. | ||
| CNEQ 130608 N | E | 0,8 |
Recommended Cutting Conditions
[v =m/min, f =mm/ tooth] [min.– optimum – max.] c t
| Grade Insert Type | ACP100 | CNMU ACP200 | / CNMQ | ACP300 1306 N / -G/ -H | ACK | 200 | ACK | 300 | |||
| Work Material Type | Low carbon steel | Alloy steel | Die steel | Low carbon steel | Alloy steel | Die steel | martensitic Stainless steel austenitic | Cast iron | Ductile cast iron | Cast iron | Ductile cast iron |
| vc | 100 –250 –400 | 80 –220 –280 | 80 –150 –250 | 80 –200 –370 | 70 –150 –250 | 60 –130 –220 | 120 –180 –240 100 –140 –200 | 220 –270 –450 | 150 –180 –250 | 180 –220 –270 | 130 –160 –220 |
| CNP 13000 ft doc | 0,1 –0,25 –0,4 | ~10 0,1 –0,25 –0,35 | 0,1 –0,2 –0,3 | 0,1 –0,25 –0,4 | ~10 0,1 –0,25 –0,35 | 0,1 –0,2 –0,3 | ~10 0,1 –0,2 –0,25 0,1 –0,2 –0,25 | ~1 0,1 –0,25 –0,4 | 0 0,1 –0,25 –0,4 | ~ 0,1 –0,25 –0,4 | 10 0,1 –0,25 –0,4 |
G42 = Euro stock Recommended Tightening Torque (N·m)