Общий каталог Sumitomo 2018 - 2019 - страница 279
Навигация
 Общий каталог Sumitomo 2012
 Каталог Sumitomo резьбонарезной инструмент
 Каталог Sumitomo пластины с режущей кромкой-моноалмаз Sumicristal
 Каталог Sumitomo инструмент для обработки канавок
 Общий каталог Sumitomo 2019 - 2020
 Каталог Sumitomo запасные части
- Pages 3-6_CS6_EN_web
- A 1-20 insert selection EN_web
- B 1-14 grades_EN_web
- C01-17 inserts intro pages_EN_web
- C18-56 negative inserts_EN_web
- C57-86 positive inserts_EN_web
- D 1-46 tool holders_EN_web
- E 1-24 boring bars_EN_web
- F 1-48 grooving_thread tools_EN_web
- G 1-54 milling cutters_EN_web
- H 1-48 insert type endmills_EN_web
- J 1-24 new endmills_EN_web
- J 25-50 endmills_EN_web
- K 1-46 Multi-Drills_EN_web
- K 47-76 Multi-Drills_EN_web
- L 1-28 cbn_pcd grades_EN_web
- M 1-34 cbn_pcd inserts_EN_web
- M 35-56 SHM tools_EN_web
- N1-24 technical guidance_EN_web
- P 1-8 spare parts_neu_EN_web
- P 9-22 index_notes_EN_web
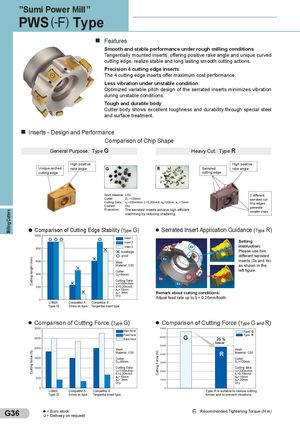
PWS(-F) Type
Features
Smooth and stable performance under rough milling conditions
Tangentially mounted inserts, offering positive rake angle and unique curved
cutting edge, realize stable and long lasting smooth cutting actions.
Precision 4 cutting edge inserts
The 4 cutting edge inserts offer maximum cost performance.
Less vibration under unstable condition
Optimized variable pitch design of the serrated inserts minimizes vibration
during unstable conditions.
Tough and durable body
Cutter body shows excellent toughness and durability through special steel
and surface treatment.
Inserts - Design and Performance
Comparison of Chip Shape
General Purpose: Type G Heavy Cut: Type R
High positive High positive
Unique arched rake angle G R Serrated rake angle
cutting edge cutting edge
Work Material: C50 2 different
| Cutter: | D c =100mm | serrated cut- |
| Cutting Data: | vc =200m/min, ft =0,20mm/t, ap =20mm, a e =10mm | ting edges |
| Coolant: | Dry | generate |
Evaluation: The serrated inserts achieve high efficient machining by reducing chattering. smaller chips Comparison of Cutting Edge Stability (Type G) Serrated Insert Application Guidance (Type R) 1000
Insert 1 Insert 2 Setting
Insert 3 4x instruction:
800 3x breakage Please use two good different serrated 4x inserts (3x and 4x)
600 Work Material: C50 as shown in the left figure. Cutter: 400 D c=80mm 3x 3x Cutting Data: vc=150m/min 4x 200 ft =0,20mm/t ap=10mm Remark about cutting conditions: ae= 3mm Dry Adjust feed rate up to f = 0,25mm/tooth. 0 t
| LNMX | Competitor A | Competitor B | ||||
| Type:G | Screw on type | Tangential insert type | ||||
| Comparison of Cutting Force (Type G) | Comparison of Cutting Force (Type G and R) | |||||
| 3000 | 7000 | |||||
| Main force | Type: G |
Feed force G Type: R
| 2500 | Back force | 6000 | 25 % |
| lower | |||
| 5000 |
| 2000 | Work | R Work | |
| Material: C50 | Material: C50 | ||
| 4000 | |||
| 1500 | Cutter: | Cutter: | |
| D c=80mm | D c=100mm | ||
| 3000 | |||
| 1000 | Cutting Data: | Cutting data: | |
| vc=150m/min | 2000 | vc=200m/min | |
| ft =0,20mm/t | ft =0,15mm/t | ||
| ap=10mm | ap=10mm | ||
| 500 | a = 3mm | a =20mm | |
| e | 1000 | e | |
| Dry | Dry |
| LNMX | Competitor A | Competitor B | Type R is suitable to reduce cutting |
| Type:G | Screw on type | Tangential insert type | forces and to prevent vibrations. |