Общий каталог Sumitomo 2018 - 2019 - страница 272
Навигация
 Общий каталог Sumitomo 2012
 Каталог Sumitomo резьбонарезной инструмент
 Каталог Sumitomo пластины с режущей кромкой-моноалмаз Sumicristal
 Каталог Sumitomo инструмент для обработки канавок
 Общий каталог Sumitomo 2019 - 2020
 Каталог Sumitomo запасные части
- Pages 3-6_CS6_EN_web
- A 1-20 insert selection EN_web
- B 1-14 grades_EN_web
- C01-17 inserts intro pages_EN_web
- C18-56 negative inserts_EN_web
- C57-86 positive inserts_EN_web
- D 1-46 tool holders_EN_web
- E 1-24 boring bars_EN_web
- F 1-48 grooving_thread tools_EN_web
- G 1-54 milling cutters_EN_web
- H 1-48 insert type endmills_EN_web
- J 1-24 new endmills_EN_web
- J 25-50 endmills_EN_web
- K 1-46 Multi-Drills_EN_web
- K 47-76 Multi-Drills_EN_web
- L 1-28 cbn_pcd grades_EN_web
- M 1-34 cbn_pcd inserts_EN_web
- M 35-56 SHM tools_EN_web
- N1-24 technical guidance_EN_web
- P 1-8 spare parts_neu_EN_web
- P 9-22 index_notes_EN_web
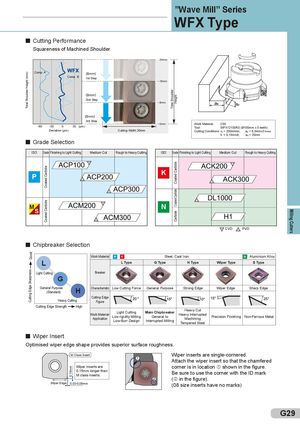
WFX Type
Cutting Performance
Squareness of Machined Shoulder
Comp. A Comp. B 1st Step
2nd Step
3rd Step Work Material: C50
| -60 | -30 | 0 | 30 (µm) | Tool: | WFX12100RS (Ø100mm x 5 teeth) | ||
| Deviation (µm) | Cutting Width 20mm | Cutting Conditions: v = 200m/min, a = 8,0mmx3 times | |||||
| c | p | ||||||
| ft = 0,15mm/t, a e = 20mm | |||||||
| Grade Selection |
ISO Grade Finishing to Light Cutting Medium Cut Rough to Heavy Cutting ISO Grade Finishing to Light Cutting Medium Cut Rough to Heavy Cutting
P K
M N
S
CVD PVD
Chipbreaker Selection
Work Material P K Steel, Cast Iron N Aluminium Alloy
L L Type G Type H Type Wiper Type S Type
Light Cutting G Breaker
| General Purpose H | Characteristic | Low Cutting Force | General Purpose | Sharp Edge Wiper Edge Strong Edge | ||
| (Standard) | ||||||
| Cutting Edge | ||||||
| Heavy Cutting | Figure | |||||
| Cutting Edge Strength High | ||||||
| Light Cutting | Main Chipbreaker | Heavy Cut | ||||
| Work Material- | Low rigidity Milling | Precision Finishing Non-Ferrous Metal Heavy Interrupted General to | ||||
| Application | Machining | |||||
| Low-Burr Design | Interrupted Milling | Tempered Steel |
Wiper Insert Optimised wiper edge shape provides superior surface roughness. M Class Insert Wiper inserts are single-cornered. Attach the wiper insert so that the chamfered
Wiper inserts are corner is in location shown in the figure. 0,15mm longer than Be sure to use the corner with the ID mark M class inserts. ( in the figure).
Wiper Edge 0,03-0,05mm (08 size inserts have no marks)