Общий каталог Sumitomo 2018 - 2019 - страница 197
Навигация
 Общий каталог Sumitomo 2012
 Каталог Sumitomo резьбонарезной инструмент
 Каталог Sumitomo пластины с режущей кромкой-моноалмаз Sumicristal
 Каталог Sumitomo инструмент для обработки канавок
 Общий каталог Sumitomo 2019 - 2020
 Каталог Sumitomo запасные части
- Pages 3-6_CS6_EN_web
- A 1-20 insert selection EN_web
- B 1-14 grades_EN_web
- C01-17 inserts intro pages_EN_web
- C18-56 negative inserts_EN_web
- C57-86 positive inserts_EN_web
- D 1-46 tool holders_EN_web
- E 1-24 boring bars_EN_web
- F 1-48 grooving_thread tools_EN_web
- G 1-54 milling cutters_EN_web
- H 1-48 insert type endmills_EN_web
- J 1-24 new endmills_EN_web
- J 25-50 endmills_EN_web
- K 1-46 Multi-Drills_EN_web
- K 47-76 Multi-Drills_EN_web
- L 1-28 cbn_pcd grades_EN_web
- M 1-34 cbn_pcd inserts_EN_web
- M 35-56 SHM tools_EN_web
- N1-24 technical guidance_EN_web
- P 1-8 spare parts_neu_EN_web
- P 9-22 index_notes_EN_web
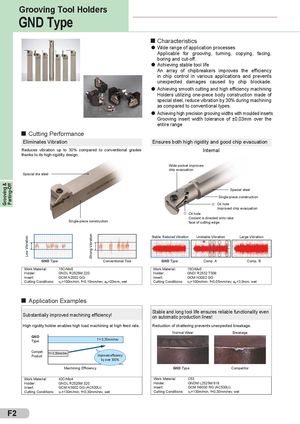
Characteristics
Wide range of application processes
Applicable for grooving, turning, copying, facing, boring and cut-off.
Achieving stable tool life
An array of chipbreakers improves the efficiency
in chip control in various applications and prevents
unexpected damages caused by chip blockade.
Achieving smooth cutting and high efficiency machining
Holders utilizing one-piece body construction made of
special steel, reduce vibration by 30% during machining
as compared to conventional types.
Achieving high precision grooving widths with moulded inserts
Grooving insert width tolerance of ±0,03mm over the
entire range
Cutting Performance
Eliminates Vibration Ensures both high rigidity and good chip evacuation
Reduces vibration up to 30% compared to conventional grades Internal
thanks to its high-rigidity design. Wide pocket improves chip evacuation Special die steel
Special steel Single-piece construction Grooving & Parting-Off Oil hole Improved chip evacuation Oil hole Coolant is directed onto rake Single-piece construction face of cutting edge
Stable, Reduced Vibration Unstable Vibration Large Vibration
GND Type Conventional Tool GND Type Comp. A Comp. B
| Work Material: | 15CrMo5 | Work Material: | 15CrMo5 |
| Holder: | GNDL R2525M 220 | Holder: | GNDI R2532 T306 |
| Insert: | GCM N2002 GG | Insert: | GCM N3002 GG |
| Cutting Conditions: | v c=100m/min, f=0,10mm/rev, a p=20mm, wet | Cutting Conditions: | vc=100m/min, f=0,05mm/rev, ap=3,0mm, wet |
Application Examples Stable and long tool life ensures reliable functionality even Substantially improved machining efficiency! on automatic production lines! High rigidity holder enables high load machining at high feed rate. Reduction of chattering prevents unexpected breakage.
Normal Wear Breakage GND Type f = 0,30mm/rev Compet. f = 0,30mm/rev Product Improved efficiency by over 300%
Machining Efficiency GND Type Competitor
| Work Material: | 42CrMo4 | Work Material: | C53 |
| Holder: | GNDL R2525M 320 | Holder: | GNDM L2525M 618 |
| Insert: | GCM N3002 GG (AC530U) | Insert: | GCM N6030 RG (AC530U) |
| Cutting Conditions: | v =130m/min, f=0,30mm/rev, wet | Cutting Conditions: | vc=130m/min, f=0,30mm/rev, wet |