Каталог Stellram твердосплавные цельные фрезы - страница 3
Навигация
 Каталог Stellram фрез со сменными пластинами
 Каталог Stellram токарный инструмент
 Каталог Stellram высокопроизводительные фрезерные системы
 Каталог Stellram системы со сменными пластинами для фрезерования с высокими подачами
 Каталог Stellram материалы и сплавы
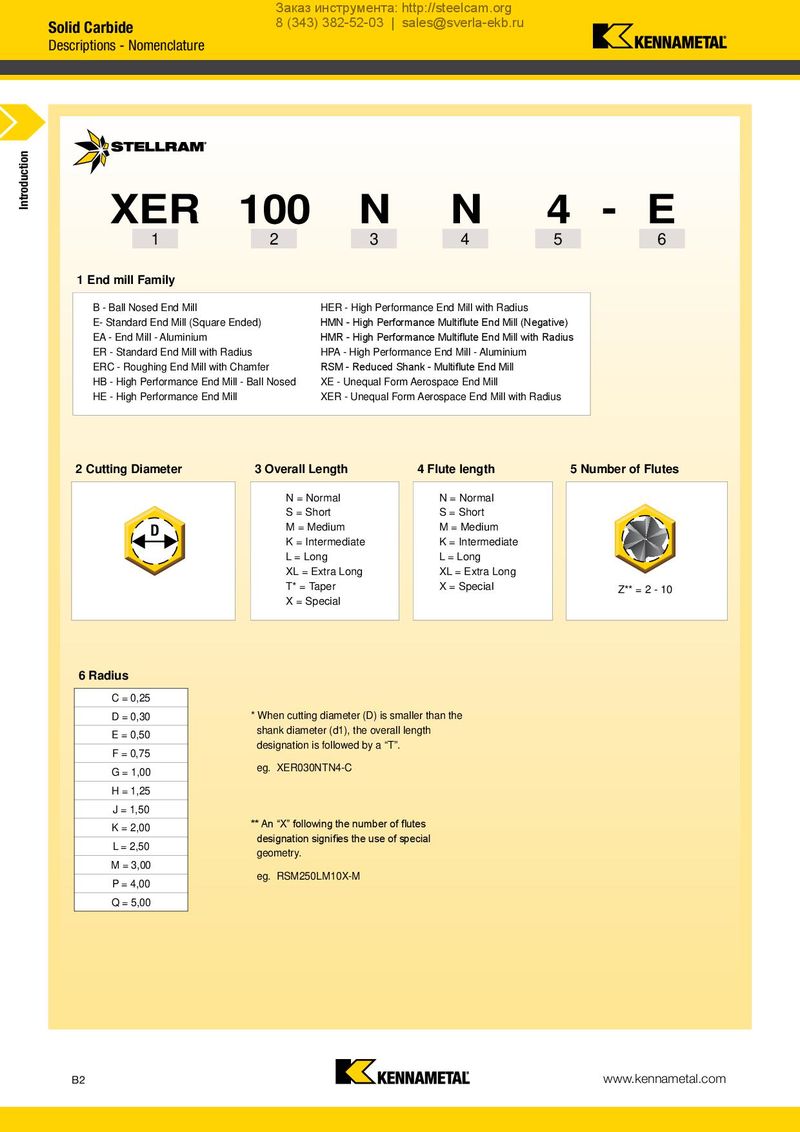
Descriptions - Nomenclature
| XER 100 | N | N | 4 | - | E | |||
| 1 | 2 | 3 | 4 | 5 | 6 |
1 End mill Family
| B - Ball Nosed End Mill | HER - High Performance End Mill with Radius |
| E- Standard End Mill (Square Ended) | HMN - High Performance Multiflute End Mill (Negative) |
| EA - End Mill - Aluminium | HMR - High Performance Multiflute End Mill with Radius |
| ER - Standard End Mill with Radius | HPA - High Performance End Mill - Aluminium |
| ERC - Roughing End Mill with Chamfer | RSM - Reduced Shank - Multiflute End Mill |
| HB - High Performance End Mill - Ball Nosed | XE - Unequal Form Aerospace End Mill |
| HE - High Performance End Mill | XER - Unequal Form Aerospace End Mill with Radius |
| 2 Cutting Diameter | 3 Overall Length | 4 Flute length | 5 Number of Flutes | ||
| N = Normal | N = Normal | ||||
| S = Short | S = Short |
| D | M = Medium | M = Medium | |
| K = Intermediate | K = Intermediate | ||
| L = Long | L = Long | ||
| XL = Extra Long | XL = Extra Long | ||
| T* = Taper | X = Special | Z** = 2 - 10 |
X = Special
6 Radius C = 0,25 D = 0,30 E = 0,50 F = 0,75 G = 1,00 H = 1,25 J = 1,50 K = 2,00 L = 2,50 M = 3,00 P = 4,00 Q = 5,00
* When cutting diameter (D) is smaller than the shank diameter (d1), the overall length designation is followed by a “T”. eg. XER030NTN4-C
** An “X” following the number of flutes designation signifies the use of special geometry. eg. RSM250LM10X-M