Каталог Stellram твердосплавные цельные фрезы - страница 22
Навигация
 Каталог Stellram фрез со сменными пластинами
 Каталог Stellram токарный инструмент
 Каталог Stellram высокопроизводительные фрезерные системы
 Каталог Stellram системы со сменными пластинами для фрезерования с высокими подачами
 Каталог Stellram материалы и сплавы
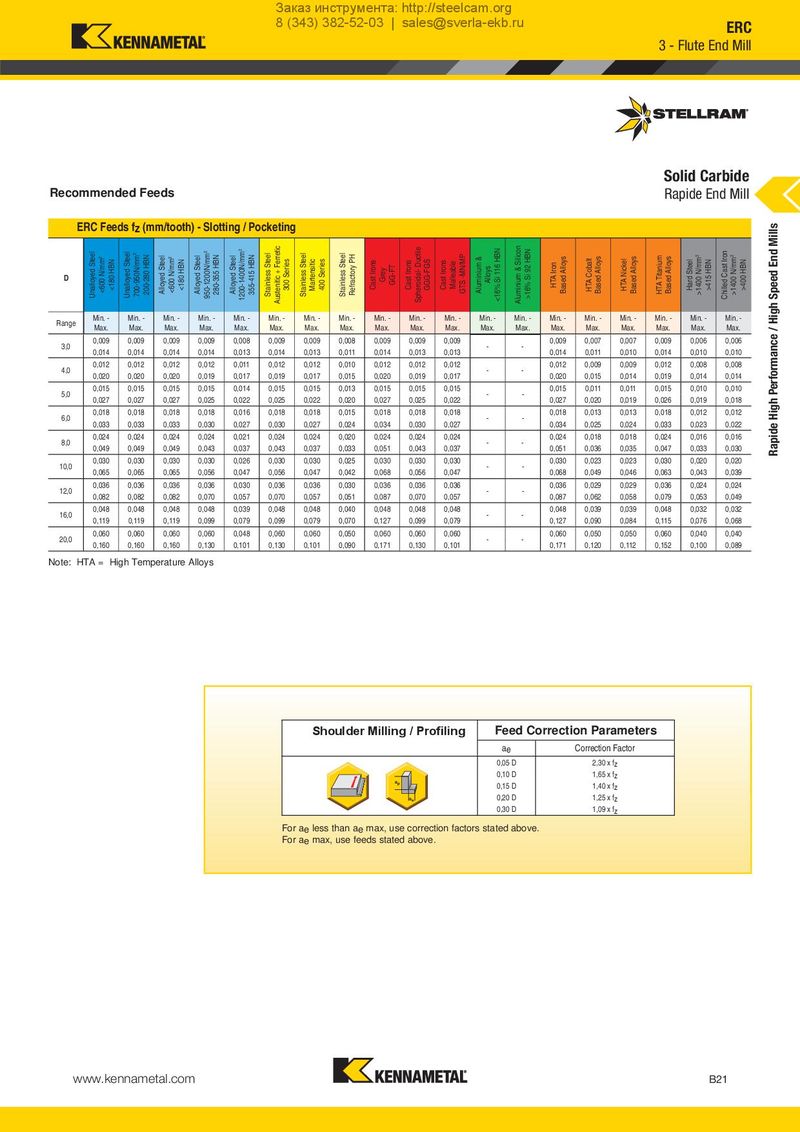
8 (343) 382-52-03 | sales@sverla-ekb.ru ERC
Solid Carbide
Recommended Feeds Rapide End Mill
| E D | RC Fee Unalloyed Steel | ds fz (m Unalloyed Steel 700-950N/mm2 200-280 HBN | m/tooth Alloyed Steel | ) - Slott Alloyed Steel 950-1200N/mm2 280-355 HBN | ing / P Alloyed Steel 1200-1400N/mm2 355-415 HBN | ocketing Stainless Steel Austenitic + Ferretic 300 Series | Stainless Steel Martensitic 400 Series | Stainless Steel Refractory PH | Cast Irons Grey GG-FT | Cast Irons Spheroidal- Ductile GGG-FGS | Cast Irons Malleable GTS -MN/MP | Aluminium & Alloys | Aluminium & Silicon >16% Si 92 HBN | HTA Iron Based Alloys | HTA Cobalt Based Alloys | HTA Nickel Based Alloys | HTA Titanium Based Alloys | Hard Steel >1400 N/mm2 >415 HBN | Chilled Cast Iron >1400 N/mm2 >400 HBN |
| Range | Min. - Max. | Min. - Max. | Min. - Max. | Min. - Max. | Min. - Max. | Min. - Max. | Min. - Max. | Min. - Max. | Min. - Max. | Min. - Max. | Min. - Max. | Min. - Max. | Min. - Max. | Min. - Max. | Min. - Max. | Min. - Max. | Min. - Max. | Min. - Max. | Min. - Max. |
| 30 | 0,009 | 0,009 | 0,009 | 0,009 | 0,008 | 0,009 | 0,009 | 0,008 | 0,009 | 0,009 | 0,009 | - | - | 0,009 | 0,007 | 0,007 | 0,009 | 0,006 | 0,006 |
| , | 0,014 | 0,014 | 0,014 | 0,014 | 0,013 | 0,014 | 0,013 | 0,011 | 0,014 | 0,013 | 0,013 | 0,014 | 0,011 | 0,010 | 0,014 | 0,010 | 0,010 | ||
| 4,0 | 0,012 0,020 | 0,012 0,020 | 0,012 0,020 | 0,012 0,019 | 0,011 0,017 | 0,012 0,019 | 0,012 0,017 | 0,010 0,015 | 0,012 0,020 | 0,012 0,019 | 0,012 0,017 | - | - | 0,012 0,020 | 0,009 0,015 | 0,009 0,014 | 0,012 0,019 | 0,008 0,014 | 0,008 0,014 |
| 50 | 0,015 | 0,015 | 0,015 | 0,015 | 0,014 | 0,015 | 0,015 | 0,013 | 0,015 | 0,015 | 0,015 | 0,015 | 0,011 | 0,011 | 0,015 | 0,010 | 0,010 | ||
| , | 0,027 | 0,027 | 0,027 | 0,025 | 0,022 | 0,025 | 0,022 | 0,020 | 0,027 | 0,025 | 0,022 | - | - | 0,027 | 0,020 | 0,019 | 0,026 | 0,019 | 0,018 |
| 0,018 | 0,018 | 0,018 | 0,018 | 0,016 | 0,018 | 0,018 | 0,015 | 0,018 | 0,018 | 0,018 | 0,018 | 0,013 | 0,013 | 0,018 | 0,012 | 0,012 | |||
| 6,0 | 0,033 | 0,033 | 0,033 | 0,030 | 0,027 | 0,030 | 0,027 | 0,024 | 0,034 | 0,030 | 0,027 | - | - | 0,034 | 0,025 | 0,024 | 0,033 | 0,023 | 0,022 |
| 80 | 0,024 | 0,024 | 0,024 | 0,024 | 0,021 | 0,024 | 0,024 | 0,020 | 0,024 | 0,024 | 0,024 | - | - | 0,024 | 0,018 | 0,018 | 0,024 | 0,016 | 0,016 |
| , | 0,049 | 0,049 | 0,049 | 0,043 | 0,037 | 0,043 | 0,037 | 0,033 | 0,051 | 0,043 | 0,037 | 0,051 | 0,036 | 0,035 | 0,047 | 0,033 | 0,030 | ||
| 100 | 0,030 | 0,030 | 0,030 | 0,030 | 0,026 | 0,030 | 0,030 | 0,025 | 0,030 | 0,030 | 0,030 | 0,030 | 0,023 | 0,023 | 0,030 | 0,020 | 0,020 | ||
| , | 0,065 | 0,065 | 0,065 | 0,056 | 0,047 | 0,056 | 0,047 | 0,042 | 0,068 | 0,056 | 0,047 | - | - | 0,068 | 0,049 | 0,046 | 0,063 | 0,043 | 0,039 |
| 0,036 | 0,036 | 0,036 | 0,036 | 0,030 | 0,036 | 0,036 | 0,030 | 0,036 | 0,036 | 0,036 | 0,036 | 0,029 | 0,029 | 0,036 | 0,024 | 0,024 | |||
| 12,0 | 0,082 | 0,082 | 0,082 | 0,070 | 0,057 | 0,070 | 0,057 | 0,051 | 0,087 | 0,070 | 0,057 | - | - | 0,087 | 0,062 | 0,058 | 0,079 | 0,053 | 0,049 |
| 0,048 | 0,048 | 0,048 | 0,048 | 0,039 | 0,048 | 0,048 | 0,040 | 0,048 | 0,048 | 0,048 | 0,048 | 0,039 | 0,039 | 0,048 | 0,032 | 0,032 | |||
| 16,0 | 0,119 | 0,119 | 0,119 | 0,099 | 0,079 | 0,099 | 0,079 | 0,070 | 0,127 | 0,099 | 0,079 | - | - | 0,127 | 0,090 | 0,084 | 0,115 | 0,076 | 0,068 |
| 200 | 0,060 | 0,060 | 0,060 | 0,060 | 0,048 | 0,060 | 0,060 | 0,050 | 0,060 | 0,060 | 0,060 | 0,060 | 0,050 | 0,050 | 0,060 | 0,040 | 0,040 | ||
| , | 0,160 | 0,160 | 0,160 | 0,130 | 0,101 | 0,130 | 0,101 | 0,090 | 0,171 | 0,130 | 0,101 | - | - | 0,171 | 0,120 | 0,112 | 0,152 | 0,100 | 0,089 |
Note: HTA = High Temperature Alloys
Shoulder Milling / Profiling Feed Correction Parameters
ae Correction Factor 0,05 D 2,30 x fz 0,10 D 1,65 x fz
ap 0,15 D 1,40 x fz
0,20 D 1,25 x fz ae 0,30 D 1,09 x fz For ae less than ae max, use correction factors stated above.
For ae max, use feeds stated above.