Каталог Stellram фрез со сменными пластинами - страница 292
Навигация
 Каталог Stellram твердосплавные цельные фрезы
 Каталог Stellram токарный инструмент
 Каталог Stellram системы со сменными пластинами для фрезерования с высокими подачами
 Каталог Stellram высокопроизводительные фрезерные системы
 Каталог Stellram материалы и сплавы
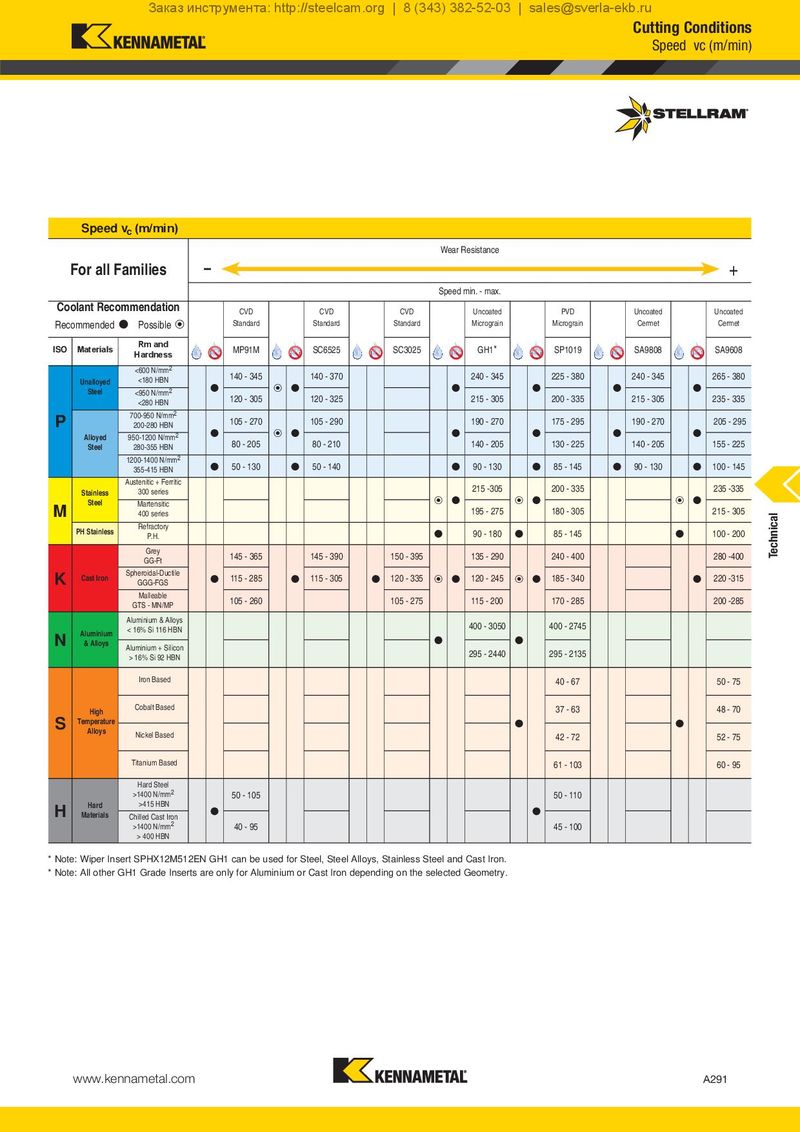
Cutting Conditions
Speed vc (m/min)
Speed vc (m/min)
| For all F | amilies | -- | Wear Resistance Speed min. - max. | + | |||||||
| Recommended Coolant Reco | Possible mmendation | CVD Standard | CVD Standard | CVD Standard | Uncoated Micrograin | PVD Micrograin | Uncoated Cermet | Uncoated Cermet | |||
| ISO Materials | Rm and Hardness | MP91M | SC6525 | SC3025 | GH1 | SP1019 | SA9808 | SA9608 | |||
| Unalloyed | 140 - 345 | 140 - 370 | 240 - 345 | 225 - 380 | | 240 - 345 | 265 - 380 | ||||
| Steel | 120 - 305 | 120 - 325 | 215 - 305 | 200 - 335 | 215 - 305 | 235 - 335 | |||||
| P | 700-950 N/mm2 200-280 HBN | 105 - 270 | 105 - 290 | 190 - 270 | 175 - 295 | | 190 - 270 | 205 - 295 | |||
| Alloyed Steel | 950-1200 N/mm2 280-355 HBN | 80 - 205 | 80 - 210 | 140 - 205 | 130 - 225 | 140 - 205 | 155 - 225 | ||||
| 1200-1400 N/mm2 355-415 HBN | 50 - 130 | 50 - 140 | 90 - 130 | 85 - 145 | | 90 - 130 | 100 - 145 | ||||
| Stainless | Austenitic + Ferritic 300 series | 215 -305 | | 200 - 335 | 235 -335 | ||||||
| M Steel | Martensitic 400 series | 195 - 275 | 180 - 305 | 215 - 305 | |||||||
| PH Stainless | Refractory P.H. | 90 - 180 | | 85 - 145 | | 100 - 200 | |||||
| Grey GG-Ft | 145 - 365 | 145 - 390 | 150 - 395 | 135 - 290 | 240 - 400 | 280 -400 | |||||
| K Cast Iron | Spheroidal-Ductile GGG-FGS | 115 - 285 | 115 - 305 | 120 - 335 | 120 - 245 | | 185 - 340 | 220 -315 | |||
| Malleable GTS - MN/MP | 105 - 260 | 105 - 275 | 115 - 200 | 170 - 285 | 200 -285 | ||||||
| N Aluminium | Aluminium & Alloys < 16% Si 116 HBN | 400 - 3050 | | 400 - 2745 | |||||||
| & Alloys | Aluminium + Silicon > 16% Si 92 HBN | 295 - 2440 | 295 - 2135 | ||||||||
| Iron Based | 40 - 67 | 50 - 75 | |||||||||
| S High Temperature | Cobalt Based | | 37 - 63 | 48 - 70 | |||||||
| Alloys | Nickel Based | 42 - 72 | 52 - 75 | ||||||||
| Titanium Based | 61 - 103 | 60 - 95 | |||||||||
| Hard | Hard Steel >1400 N/mm2 >415 HBN | 50 - 105 | 50 - 110 | ||||||||
| H Materials | Chilled Cast Iron >1400 N/mm2 > 400 HBN | 40 - 95 | 45 - 100 |
- Note: Wiper Insert SPHX12M512EN GH1 can be used for Steel, Steel Alloys, Stainless Steel and Cast Iron.
- Note: All other GH1 Grade Inserts are only for Aluminium or Cast Iron depending on the selected Geometry.