Каталог Stellram фрез со сменными пластинами - страница 252
Навигация
 Каталог Stellram твердосплавные цельные фрезы
 Каталог Stellram токарный инструмент
 Каталог Stellram системы со сменными пластинами для фрезерования с высокими подачами
 Каталог Stellram высокопроизводительные фрезерные системы
 Каталог Stellram материалы и сплавы
Profiling / Pocketing Milling Cutters
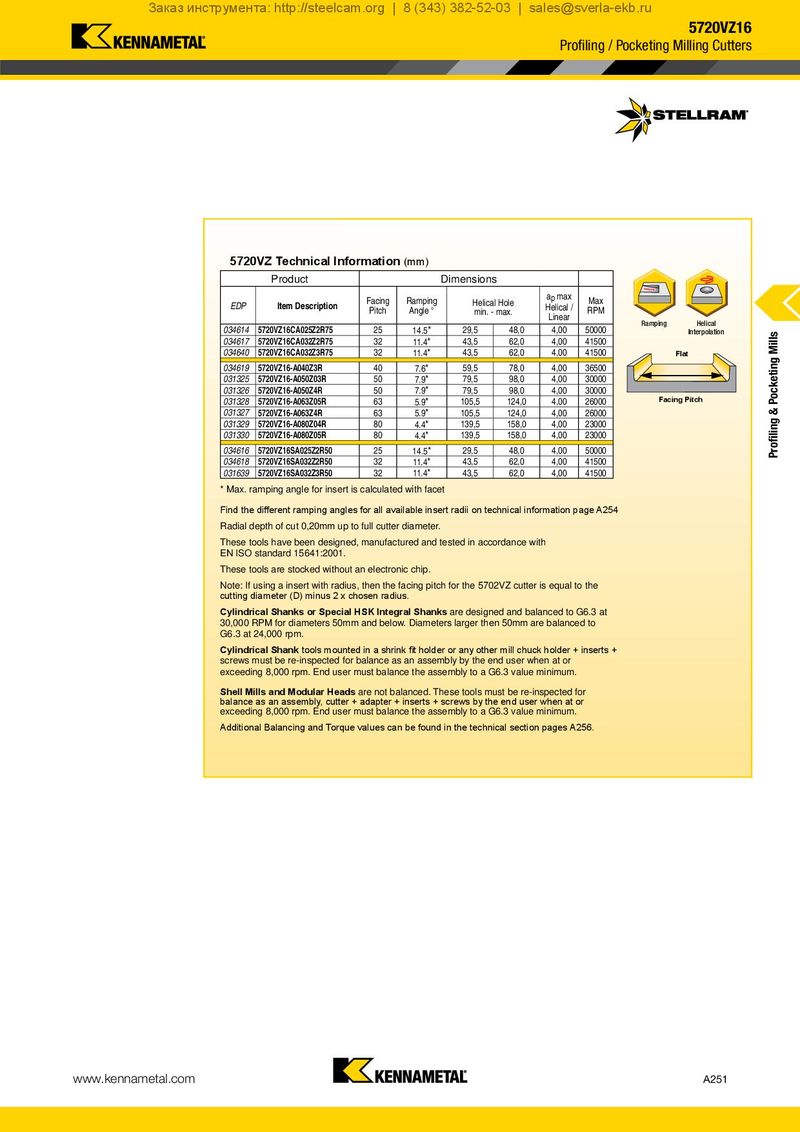
5720VZ Technical Information (mm)
Product Dimensions
Facing Ramping ap max Max
EDP Item Description Helical Hole Helical /
| Pitch | Angle ° | min. - max. | RPM | |
| Linear |
| 034614 | 5720VZ16CA025Z2R75 | 25 | 14.5* | 29,5 | 48,0 | 4,00 | Helical Ramping 50000 |
| Interpolation | |||||||
| 034617 | 5720VZ16CA032Z2R75 | 32 | 11.4* | 43,5 | 62,0 | 4,00 | 41500 |
| 034640 | 5720VZ16CA032Z3R75 | 32 | 11.4* | 43,5 | 62,0 | 4,00 | Flat 41500 |
| 034619 | 5720VZ16-A040Z3R | 40 | 7.6* | 59,5 | 78,0 | 4,00 | 36500 |
| 031325 | 5720VZ16-A050Z03R | 50 | 7.9* | 79,5 | 98,0 | 4,00 | 30000 |
| 031326 | 5720VZ16-A050Z4R | 50 | 7.9* | 79,5 | 98,0 | 4,00 | 30000 |
| 031328 | 5720VZ16-A063Z05R | 63 | 5.9* | 105,5 | 124,0 | 4,00 | Facing Pitch 26000 |
| 031327 | 5720VZ16-A063Z4R | 63 | 5.9* | 105,5 | 124,0 | 4,00 | 26000 |
| 031329 | 5720VZ16-A080Z04R | 80 | 4.4* | 139,5 | 158,0 | 4,00 | 23000 |
| 031330 | 5720VZ16-A080Z05R | 80 | 4.4* | 139,5 | 158,0 | 4,00 | 23000 |
| 034616 | 5720VZ16SA025Z2R50 | 25 | 14.5* | 29,5 | 48,0 | 4,00 | 50000 |
| 034618 | 5720VZ16SA032Z2R50 | 32 | 11.4* | 43,5 | 62,0 | 4,00 | 41500 |
| 031639 | 5720VZ16SA032Z3R50 | 32 | 11.4* | 43,5 | 62,0 | 4,00 | 41500 |
* Max. ramping angle for insert is calculated with facet Find the different ramping angles for all available insert radii on technical information page A254 Radial depth of cut 0,20mm up to full cutter diameter. These tools have been designed, manufactured and tested in accordance with
EN ISO standard 15641:2001. These tools are stocked without an electronic chip. Note: If using a insert with radius, then the facing pitch for the 5702VZ cutter is equal to the cutting diameter (D) minus 2 x chosen radius. Cylindrical Shanks or Special HSK Integral Shanks are designed and balanced to G6.3 at 30,000 RPM for diameters 50mm and below. Diameters larger then 50mm are balanced to G6.3 at 24,000 rpm. Cylindrical Shank tools mounted in a shrink fit holder or any other mill chuck holder + inserts + screws must be re-inspected for balance as an assembly by the end user when at or exceeding 8,000 rpm. End user must balance the assembly to a G6.3 value minimum. Shell Mills and Modular Heads are not balanced. These tools must be re-inspected for balance as an assembly, cutter + adapter + inserts + screws by the end user when at or exceeding 8,000 rpm. End user must balance the assembly to a G6.3 value minimum. Additional Balancing and Torque values can be found in the technical section pages A256.