Каталог Stellram фрез со сменными пластинами - страница 245
Навигация
 Каталог Stellram твердосплавные цельные фрезы
 Каталог Stellram токарный инструмент
 Каталог Stellram системы со сменными пластинами для фрезерования с высокими подачами
 Каталог Stellram высокопроизводительные фрезерные системы
 Каталог Stellram материалы и сплавы
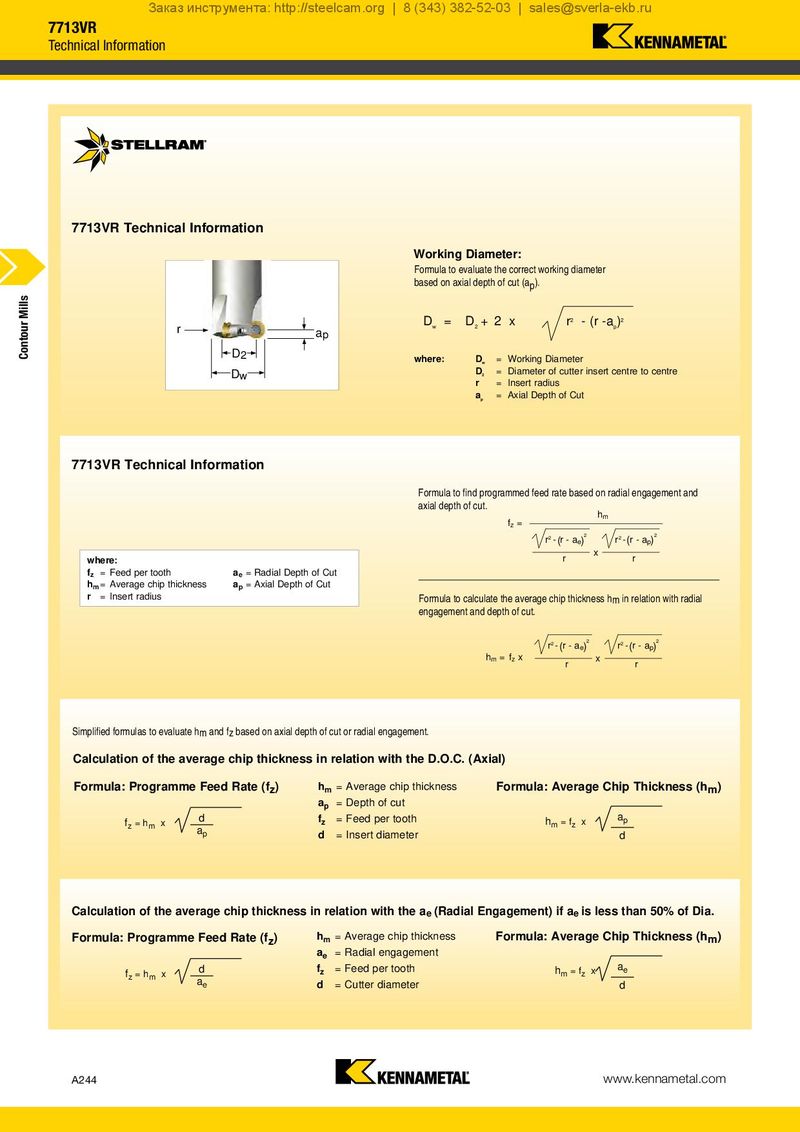
7713VR Technical Information
r a
p
D2
Dw
Working Diameter:
Formula to evaluate the correct working diameter
based on axial depth of cut (ap).
D = D + 2 x r2 - (r -a )2
w 2 p
where: D = Working Diameter w D = Diameter of cutter insert centre to centre 2 r = Insert radius a = Axial Depth of Cut p
7713VR Technical Information
where: f = Feed per tooth a = Radial Depth of Cut z e
h = Average chip thickness a = Axial Depth of Cut
m p r = Insert radius
Formula to find programmed feed rate based on radial engagement and
axial depth of cut. h m f = z
r 2 - r - a( )2 r 2 - r - a( )2
e p x r r
Formula to calculate the average chip thickness hm in relation with radial
engagement and depth of cut.
r - r - a( )2 r - r - a( )2
2 e 2 p
| h | = f | x | x | ||
| m | z | r | r |
Simplified formulas to evaluate hm and fz based on axial depth of cut or radial engagement.
Calculation of the average chip thickness in relation with the D.O.C. (Axial)
| Formula: Programme Feed Rate (fz) | h | = Average chip thickness | Formula: Average Chip Thickness (hm) |
| m | |||
| a = Depth of cut | |||
| p |
d f = Feed per tooth a
| f = h | x | z | h | = f x | p | ||
| z | m | a | m | z | |||
| p | d = Insert diameter | d |
Calculation of the average chip thickness in relation with the ae (Radial Engagement) if ae is less than 50% of Dia.
| Formula: Programme Feed Rate (f ) | h | = Average chip thickness | Formula: Average Chip Thickness (hm) | |
| z | m | |||
| a = Radial engagement | ||||
| e |
| d | f = Feed per tooth | h | a | ||||
| f = h | x | z | = f x | e | |||
| z | m | m | z |
a d = Cutter diameter e d