Каталог Stellram фрез со сменными пластинами - страница 234
Навигация
 Каталог Stellram твердосплавные цельные фрезы
 Каталог Stellram токарный инструмент
 Каталог Stellram системы со сменными пластинами для фрезерования с высокими подачами
 Каталог Stellram высокопроизводительные фрезерные системы
 Каталог Stellram материалы и сплавы
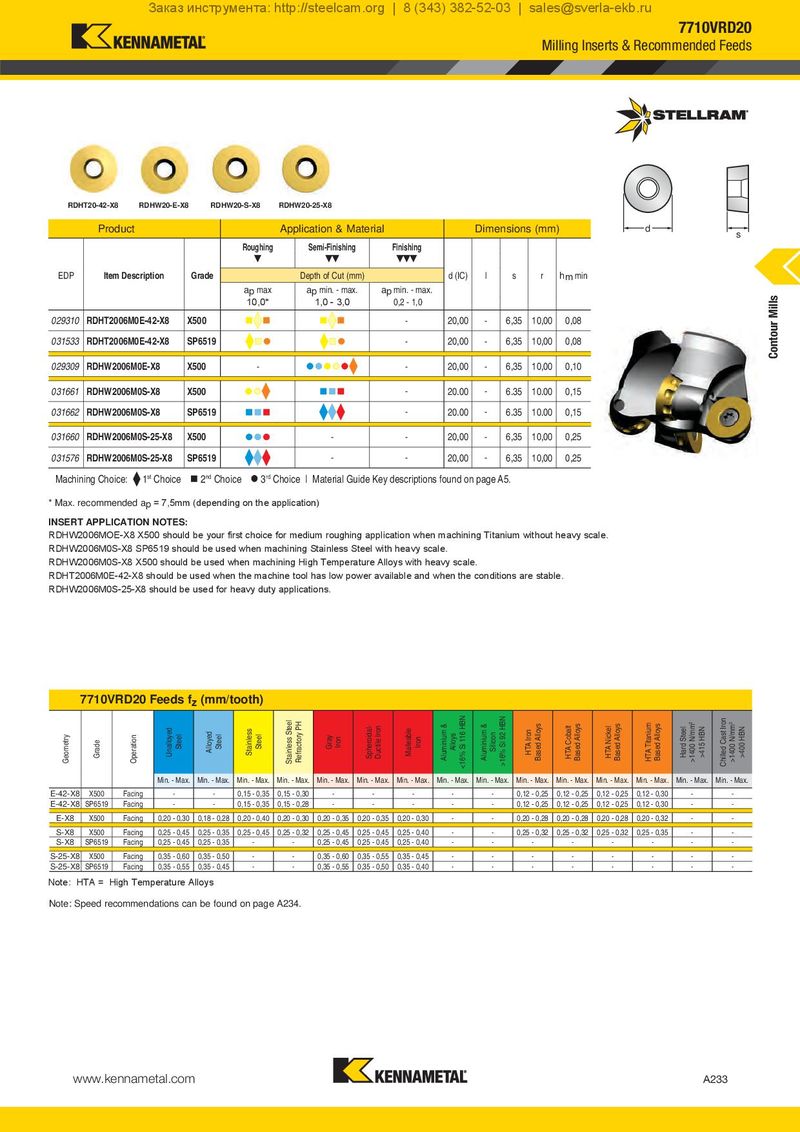
| RD | HT20-42-X8 RDHW20-E- | X8 RDH | W20-S-X8 RD | HW20-25-X8 | ||||||
| Product | A | pplication & Mate | rial | Dimensions | (mm | ) | d s | |||
| Roughing | Semi-Finishing | Finishing | ||||||||
| EDP | Item Description | Grade | Depth of Cut(mm) | d (IC) | l s | r | hmmin | |||
| apmax 10,0 | apmin. - max. 1,0 - 3,0 | apmin. - max. 0,2 - 1,0 | ||||||||
| 029310 | RDHT2006M0E-42-X8 | X500 | - | 20,00 | - 6,35 | 10,00 | 0,08 | |||
| 031533 | RDHT2006M0E-42-X8 | SP6519 | - | 20,00 | - 6,35 | 10,00 | 0,08 | |||
| 029309 | RDHW2006M0E-X8 | X500 | - | - | 20,00 | - 6,35 | 10,00 | 0,10 | ||
| 031661 | RDHW2006M0S-X8 | X500 | - | 20.00 | - 6.35 | 10.00 | 0,15 | |||
| 031662 | RDHW2006M0S-X8 | SP6519 | - | 20.00 | - 6.35 | 10.00 | 0,15 | |||
| 031660 | RDHW2006M0S-25-X8 | X500 | - | - | 20,00 | - 6,35 | 10,00 | 0,25 | ||
| 031576 | RDHW2006M0S-25-X8 | SP6519 | - | - | 20,00 | - 6,35 | 10,00 | 0,25 |
Machining Choice: 1st Choice 2nd Choice 3rd Choice | Material Guide Key descriptions found on page A5. * Max. recommended ap = 7,5mm (depending on the application)
INSERT APPLICATION NOTES: RDHW2006MOE-X8 X500 should be your first choice for medium roughing application when machining Titanium without heavy scale. RDHW2006M0S-X8 SP6519 should be used when machining Stainless Steel with heavy scale. RDHW2006M0S-X8 X500 should be used when machining High Temperature Alloys with heavy scale. RDHT2006M0E-42-X8 should be used when the machine tool has low power available and when the conditions are stable. RDHW2006M0S-25-X8 should be used for heavy duty applications.
| 7 | 710V | RD20 | Feeds f | z (mm/t | ooth) | ||||||||||||
| Geometry | Grade | Operation | Unalloyed Steel | Alloyed Steel | Stainless Steel | Stainless Steel Refractory PH | Gray Iron | Spheroidal- Ductile Iron | Malleable Iron | Aluminium & Alloys | Aluminium & Silicon >16% Si 92 HBN | HTA Iron Based Alloys | HTA Cobalt Based Alloys | HTA Nickel Based Alloys | HTA Titanium Based Alloys | Hard Steel >1400 N/mm2 >415 HBN | Chilled Cast Iron >1400 N/mm2 >400 HBN |
| Min. - Max. | Min. - Max. | Min. - Max. | Min. - Max. | Min. - Max. | Min. - Max. | Min. - Max. | Min. - Max. | Min. - Max. | Min. - Max. | Min. - Max. | Min. - Max. | Min. - Max. | Min. - Max. | Min. - Max. | |||
| E-42-X8 | X500 | Facing | - | - | 0,15 - 0,35 | 0,15 - 0,30 | - | - | - | - | - | 0,12 - 0,25 | 0,12 - 0,25 | 0,12 - 0,25 | 0,12 - 0,30 | - | - |
| E-42-X8 | SP6519 | Facing | - | - | 0,15-0,35 | 0,15-0,28 | - | - | - | - | - | 0,12 -0,25 | 0,12 -0,25 | 0,12 -0,25 | 0,12 -0,30 | - | - |
| E-X8 | X500 | Facing | 0,20-0,30 | 0,18-0,28 | 0,20-0,40 | 0,20-0,30 | 0,20-0,35 | 0,20-0,35 | 0,20-0,30 | - | - | 0,20-0,28 | 0,20-0,28 | 0,20-0,28 | 0,20-0,32 | - | - |
| S-X8 | X500 | Facing | 0,25-0,45 | 0,25-0,35 | 0,25-0,45 | 0,25-0,32 | 0,25-0,45 | 0,25-0,45 | 0,25-0,40 | - | - | 0,25-0,32 | 0,25-0,32 | 0,25-0,32 | 0,25-0,35 | - | - |
| S-X8 | SP6519 | Facing | 0,25-0,45 | 0,25-0,35 | - | - | 0,25-0,45 | 0,25-0,45 | 0,25-0,40 | - | - | - | - | - | - | - | - |
| S-25-X8 | X500 | Facing | 0,35-0,60 | 0,35-0,50 | - | - | 0,35-0,60 | 0,35-0,55 | 0,35-0,45 | - | - | - | - | - | - | - | - |
| S-25-X8 | SP6519 | Facing | 0,35 - 0,55 | 0,35 - 0,45 | - | - | 0,35 - 0,55 | 0,35 - 0,50 | 0,35 - 0,40 | - | - | - | - | - | - | - | - |
Note: HTA = High Temperature Alloys Note: Speed recommendations can be found on page A234.