Каталог Stellram фрез со сменными пластинами - страница 199
Навигация
 Каталог Stellram твердосплавные цельные фрезы
 Каталог Stellram токарный инструмент
 Каталог Stellram системы со сменными пластинами для фрезерования с высокими подачами
 Каталог Stellram высокопроизводительные фрезерные системы
 Каталог Stellram материалы и сплавы
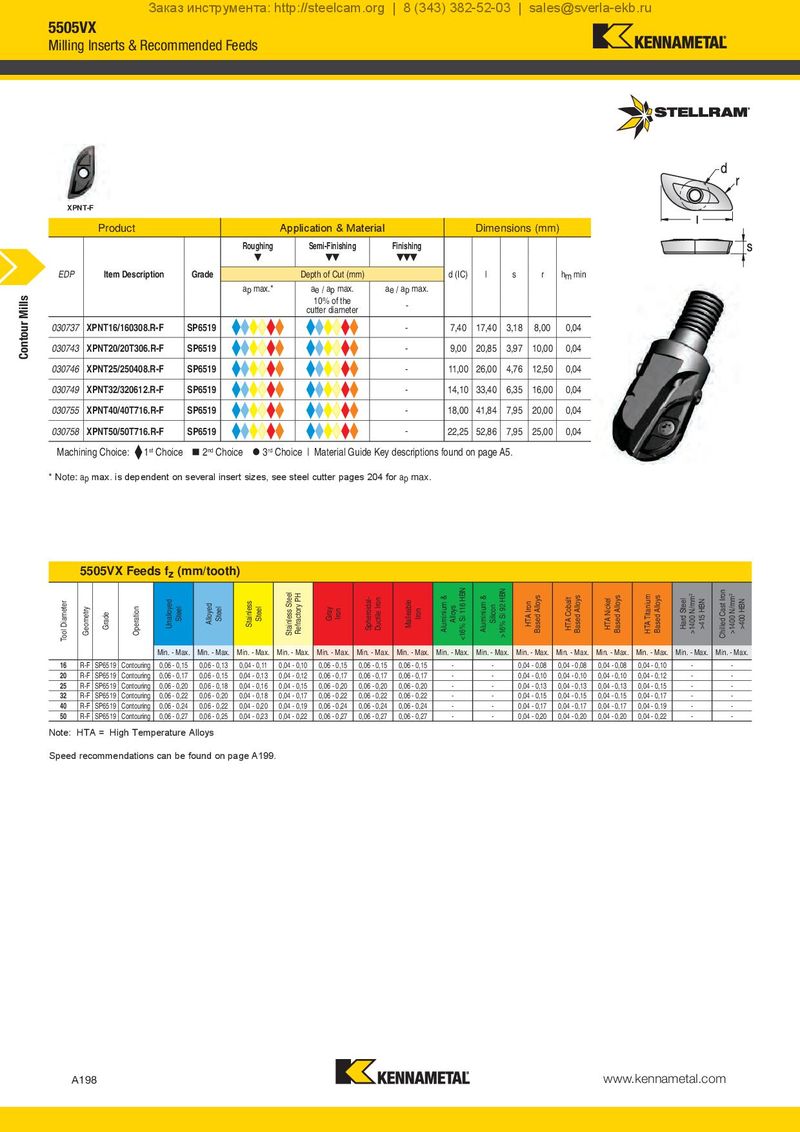
XPNT-F
Product Application & Material Dimensions (mm)
Roughing Semi-Finishing Finishing
EDP Item Description Grade Depth of Cut (mm) d (IC) l s r hm min
| ap max.* | ae / ap max. | ae / ap max. | |
| 10% of the | - | ||
| cutter diameter |
| 030737 | XPNT16/160308.R-F | SP6519 | - | 0,04 7,40 17,40 3,18 8,00 |
| 030743 | XPNT20/20T306.R-F | SP6519 | - | 9,00 20,85 3,97 10,00 0,04 |
| 030746 | XPNT25/250408.R-F | SP6519 | - | 11,00 26,00 4,76 12,50 0,04 |
| 030749 | XPNT32/320612.R-F | SP6519 | - | 14,10 33,40 6,35 16,00 0,04 |
| 030755 | XPNT40/40T716.R-F | SP6519 | - | 18,00 41,84 7,95 20,00 0,04 |
| 030758 | XPNT50/50T716.R-F | SP6519 | - | 22,25 52,86 7,95 25,00 0,04 |
Machining Choice: 1st Choice 2nd Choice 3rd Choice | Material Guide Key descriptions found on page A5. * Note: ap max. is dependent on several insert sizes, see steel cutter pages 204 for ap max.
5505VX Feeds fz (mm/tooth)
Alloyed Steel Gray Iron Spheroidal- Ductile Iron Hard Steel >1400 N/mm Stainless Steel Refractory PH Chilled Cast Iron >1400 N/mm Min. - Max. Min. - Max. Min. - Max. Min. - Max. Min. - Max. Min. - Max. Min. - Max. Min. - Max. Min. - Max. Min. - Max. Min. - Max. Min. - Max. Min. - Max. Min. - Max. Min. - Max.
| 16 | R-F SP6519 | Contouring | 0,06 - 0,15 | 0,06 - 0,13 | 0,04 - 0,11 | 0,04 - 0,10 | 0,06 - 0,15 | 0,06 - 0,15 | 0,06 - 0,15 | - | - | 0,04 - 0,08 | 0,04 - 0,08 | 0,04 - 0,08 | 0,04 - 0,10 | - | - |
| 20 | R-F SP6519 | Contouring | 0,06 - 0,17 | 0,06 - 0,15 | 0,04 - 0,13 | 0,04 - 0,12 | 0,06 - 0,17 | 0,06 - 0,17 | 0,06 - 0,17 | - | - | 0,04 - 0,10 | 0,04 - 0,10 | 0,04 - 0,10 | 0,04 - 0,12 | - | - |
| 25 | R-F SP6519 | Contouring | 0,06 - 0,20 | 0,06 - 0,18 | 0,04 - 0,16 | 0,04 - 0,15 | 0,06 - 0,20 | 0,06 - 0,20 | 0,06 - 0,20 | - | - | 0,04 - 0,13 | 0,04 - 0,13 | 0,04 - 0,13 | 0,04 - 0,15 | - | - |
| 32 | R-F SP6519 | Contouring | 0,06 - 0,22 | 0,06 - 0,20 | 0,04 - 0,18 | 0,04 - 0,17 | 0,06 - 0,22 | 0,06 - 0,22 | 0,06 - 0,22 | - | - | 0,04 - 0,15 | 0,04 - 0,15 | 0,04 - 0,15 | 0,04 - 0,17 | - | - |
| 40 | R-F SP6519 | Contouring | 0,06 - 0,24 | 0,06 - 0,22 | 0,04 - 0,20 | 0,04 - 0,19 | 0,06 - 0,24 | 0,06 - 0,24 | 0,06 - 0,24 | - | - | 0,04 - 0,17 | 0,04 - 0,17 | 0,04 - 0,17 | 0,04 - 0,19 | - | - |
| 50 | R-F SP6519 | Contouring | 0,06 - 0,27 | 0,06 - 0,25 | 0,04 - 0,23 | 0,04 - 0,22 | 0,06 - 0,27 | 0,06 - 0,27 | 0,06 - 0,27 | - | - | 0,04 - 0,20 | 0,04 - 0,20 | 0,04 - 0,20 | 0,04 - 0,22 | - | - |
Note: HTA = High Temperature Alloys Speed recommendations can be found on page A199.