Каталог Stellram фрез со сменными пластинами - страница 195
Навигация
 Каталог Stellram твердосплавные цельные фрезы
 Каталог Stellram токарный инструмент
 Каталог Stellram системы со сменными пластинами для фрезерования с высокими подачами
 Каталог Stellram высокопроизводительные фрезерные системы
 Каталог Stellram материалы и сплавы
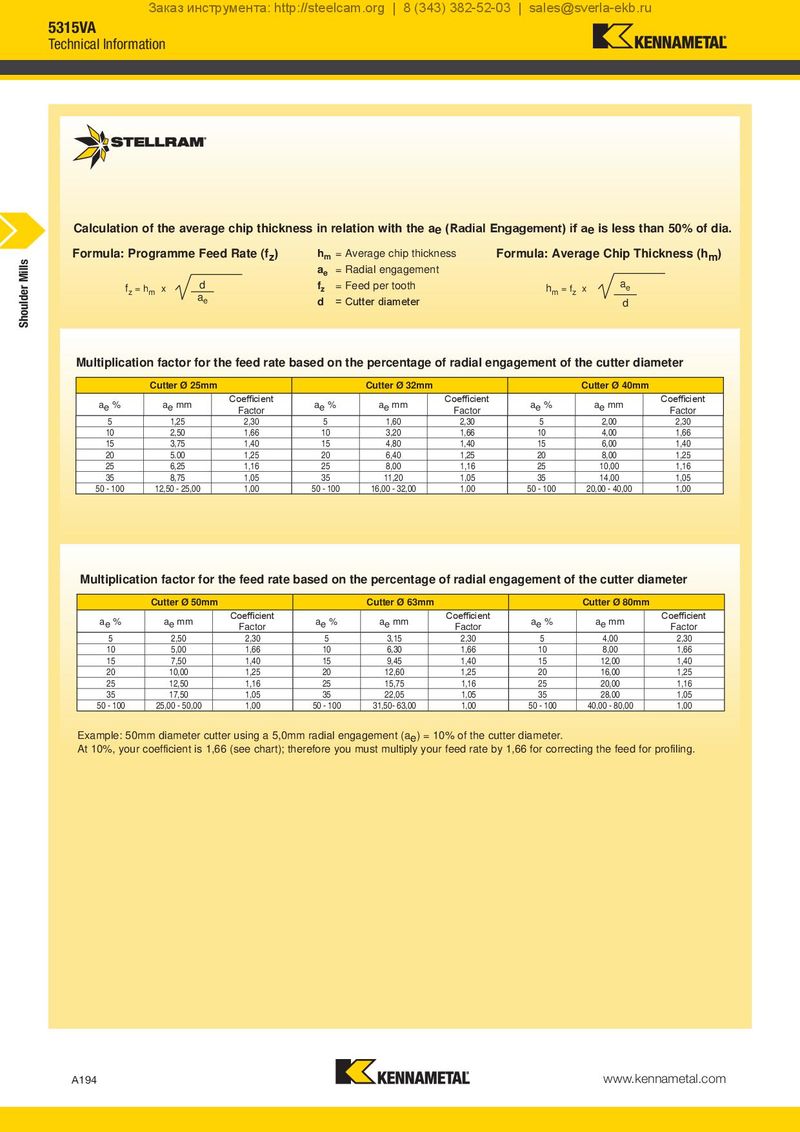
Calculation of the average chip thickness in relation with the ae (Radial Engagement) if ae is less than 50% of dia.
| Formula: Programme Feed Rate (f ) | h | = Average chip thickness | Formula: Average Chip Thickness (h | ) | |
| z | m | m | |||
| a = Radial engagement | |||||
| e |
d f = Feed per tooth a
| f = h | x | z | h | = f x | e | |||
| z | m | m | z | |||||
| a | = Cutter diameter | |||||||
| e | d | d |
Multiplication factor for the feed rate based on the percentage of radial engagement of the cutter diameter
| Cutter Ø 25mm | i | Cutter Ø 32mm | i | Cutter Ø 40m | m i | |||
| ae % | ae mm | Coefficient Factor | ae % | ae mm | Coefficient Factor | ae % | ae mm | Coefficient Factor |
| 5 | 1,25 | 2,30 | 5 | 1,60 | 2,30 | 5 | 2,00 | 2,30 |
| 10 | 2,50 | 1,66 | 10 | 3,20 | 1,66 | 10 | 4,00 | 1,66 |
| 15 | 3,75 | 1,40 | 15 | 4,80 | 1,40 | 15 | 6,00 | 1,40 |
| 20 | 5.00 | 1,25 | 20 | 6,40 | 1,25 | 20 | 8,00 | 1,25 |
| 25 | 6,25 | 1,16 | 25 | 8,00 | 1,16 | 25 | 10,00 | 1,16 |
| 35 | 8,75 | 1,05 | 35 | 11,20 | 1,05 | 35 | 14,00 | 1,05 |
| 50-100 | 12,50-25,00 | 1,00 | 50-100 | 16,00-32,00 | 1,00 | 50-100 | 20,00-40,00 | 1,00 |
Multiplication factor for the feed rate based on the percentage of radial engagement of the cutter diameter
| Cutter Ø 50mm | Cutter Ø 63mm | Cutter Ø 80mm | ||||||
| ae % | ae mm | Coefficient Factor | ae % | ae mm | Coefficient Factor | ae % | ae mm | Coefficient Factor |
| 5 | 2,50 | 2,30 | 5 | 3,15 | 2,30 | 5 | 4,00 | 2,30 |
| 10 | 5,00 | 1,66 | 10 | 6,30 | 1,66 | 10 | 8,00 | 1,66 |
| 15 | 7,50 | 1,40 | 15 | 9,45 | 1,40 | 15 | 12,00 | 1,40 |
| 20 | 10,00 | 1,25 | 20 | 12,60 | 1,25 | 20 | 16,00 | 1,25 |
| 25 | 12,50 | 1,16 | 25 | 15,75 | 1,16 | 25 | 20,00 | 1,16 |
| 35 | 17,50 | 1,05 | 35 | 22,05 | 1,05 | 35 | 28,00 | 1,05 |
| 50-100 | 25,00-50,00 | 1,00 | 50-100 | 31,50-63,00 | 1,00 | 50-100 | 40,00-80,00 | 1,00 |
Example: 50mm diameter cutter using a 5,0mm radial engagement (ae) = 10% of the cutter diameter. At 10%, your coefficient is 1,66 (see chart); therefore you must multiply your feed rate by 1,66 for correcting the feed for profiling.