Каталог Stellram фрез со сменными пластинами - страница 106
Навигация
 Каталог Stellram твердосплавные цельные фрезы
 Каталог Stellram токарный инструмент
 Каталог Stellram системы со сменными пластинами для фрезерования с высокими подачами
 Каталог Stellram высокопроизводительные фрезерные системы
 Каталог Stellram материалы и сплавы
7745VSE
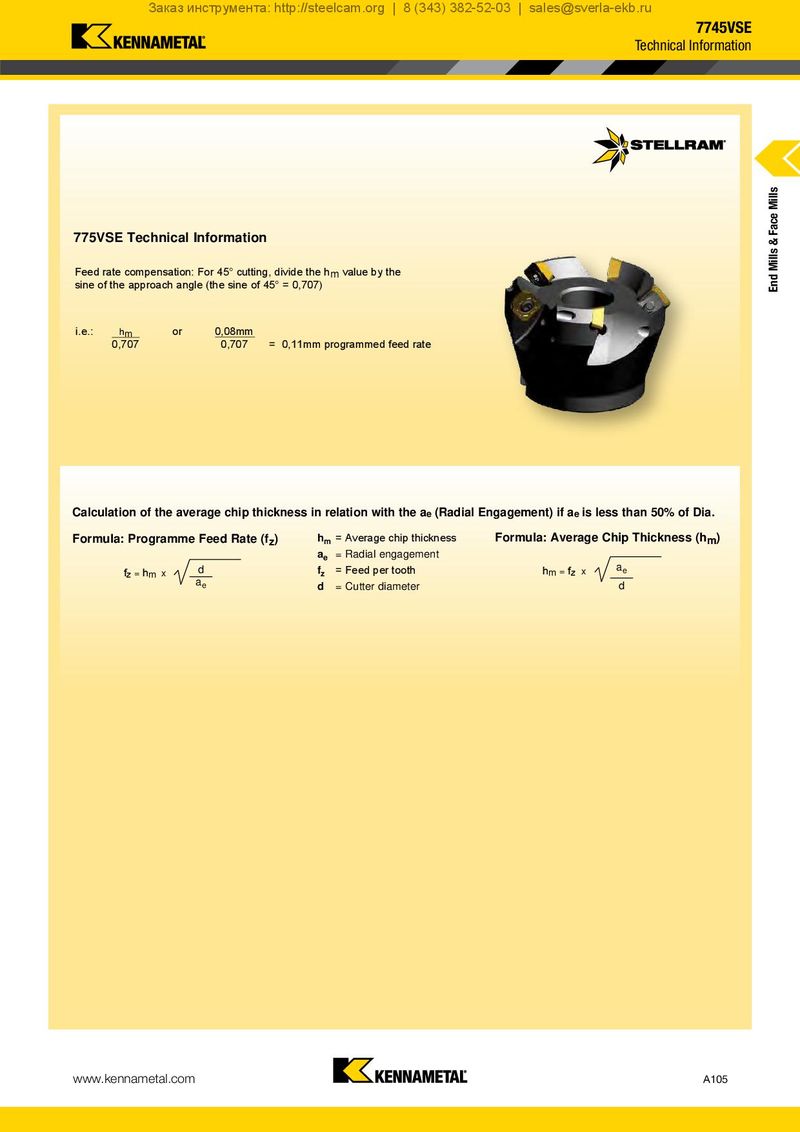
775VSE Technical Information
Feed rate compensation: For 45° cutting, divide the h value by the m sine of the approach angle (the sine of 45° = 0,707)
i.e.: h or 0,08mm m
0,707 0,707 = 0,11mm programmed feed rate
Calculation of the average chip thickness in relation with the ae (Radial Engagement) if ae is less than 50% of Dia.
| Formula: Programme Feed Rate (f ) | h | = Average chip thickness | Formula: Average Chip Thickness (h | ) | |
| z | m | m | |||
| a = Radial engagement | |||||
| e |
| f | h | d | f = Feed per tooth | h | fz | a |
| z = | m x | m = | x | e |
z a d e d = Cutter diameter