Каталог Stellram фрез со сменными пластинами - страница 103
Навигация
 Каталог Stellram твердосплавные цельные фрезы
 Каталог Stellram токарный инструмент
 Каталог Stellram системы со сменными пластинами для фрезерования с высокими подачами
 Каталог Stellram высокопроизводительные фрезерные системы
 Каталог Stellram материалы и сплавы
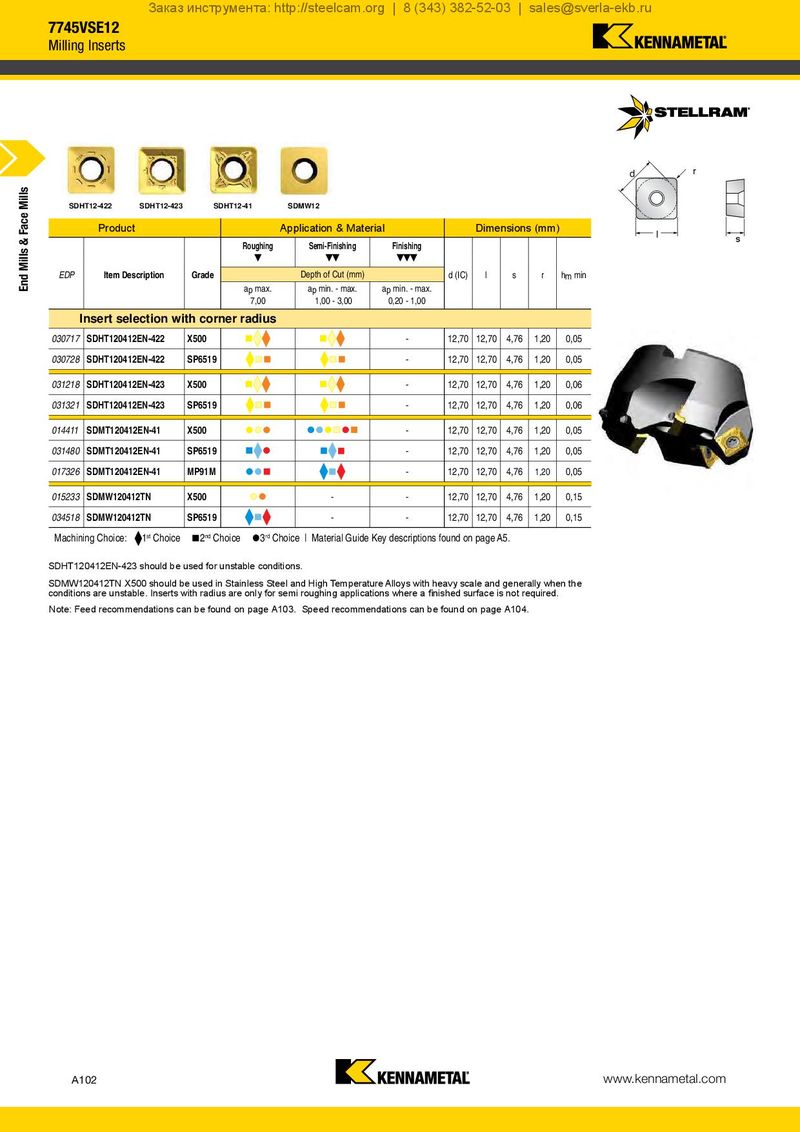
| SD | HT12-422 SDHT12-4 | 23 SD | HT12-41 | SDMW12 | d r | ||||||
| Product | A | pplication & Mate | rial | Dime | nsions | (mm | ) | l s | |||
| Roughing | Semi-Finishing | Finishing | |||||||||
| EDP | Item Description | Grade | Depth of Cut(mm) | d (IC) | l | s | r | hm min | |||
| ap max. 7,00 | ap min. - max. 1,00 - 3,00 | ap min. - max. 0,20 - 1,00 | |||||||||
| Insert selection w | ith corn | er radius | |||||||||
| 030717 | SDHT120412EN-422 | X500 | - | 12,70 | 12,70 | 4,76 | 1,20 | 0,05 | |||
| 030728 | SDHT120412EN-422 | SP6519 | - | 12,70 | 12,70 | 4,76 | 1,20 | 0,05 | |||
| 031218 | SDHT120412EN-423 | X500 | - | 12,70 | 12,70 | 4,76 | 1,20 | 0,06 | |||
| 031321 | SDHT120412EN-423 | SP6519 | - | 12,70 | 12,70 | 4,76 | 1,20 | 0,06 | |||
| 014411 | SDMT120412EN-41 | X500 | - | 12,70 | 12,70 | 4,76 | 1,20 | 0,05 | |||
| 031480 | SDMT120412EN-41 | SP6519 | - | 12,70 | 12,70 | 4,76 | 1,20 | 0,05 | |||
| 017326 | SDMT120412EN-41 | MP91M | - | 12,70 | 12,70 | 4,76 | 1,20 | 0,05 | |||
| 015233 | SDMW120412TN | X500 | - | - | 12,70 | 12,70 | 4,76 | 1,20 | 0,15 | ||
| 034518 | SDMW120412TN | SP6519 | - | - | 12,70 | 12,70 | 4,76 | 1,20 | 0,15 |
Machining Choice: 1st Choice 2nd Choice 3rd Choice | Material Guide Key descriptions found on page A5. SDHT120412EN-423 should be used for unstable conditions. SDMW120412TN X500 should be used in Stainless Steel and High Temperature Alloys with heavy scale and generally when the conditions are unstable. Inserts with radius are only for semi roughing applications where a finished surface is not required. Note: Feed recommendations can be found on page A103. Speed recommendations can be found on page A104.