Общий каталог SGS 2018 - страница 59
Навигация
 Каталог SGS шестизубые фрезы T-carb
 Каталог SGS микро инструмент 2021
 Каталог SGS фрезы для алюминия S-carb
 Каталог SGS высокопроизводительные черновые фрезы
 Каталог SGS инструмент для обработки алюминия
 Общий каталог SGS 2015 на русском
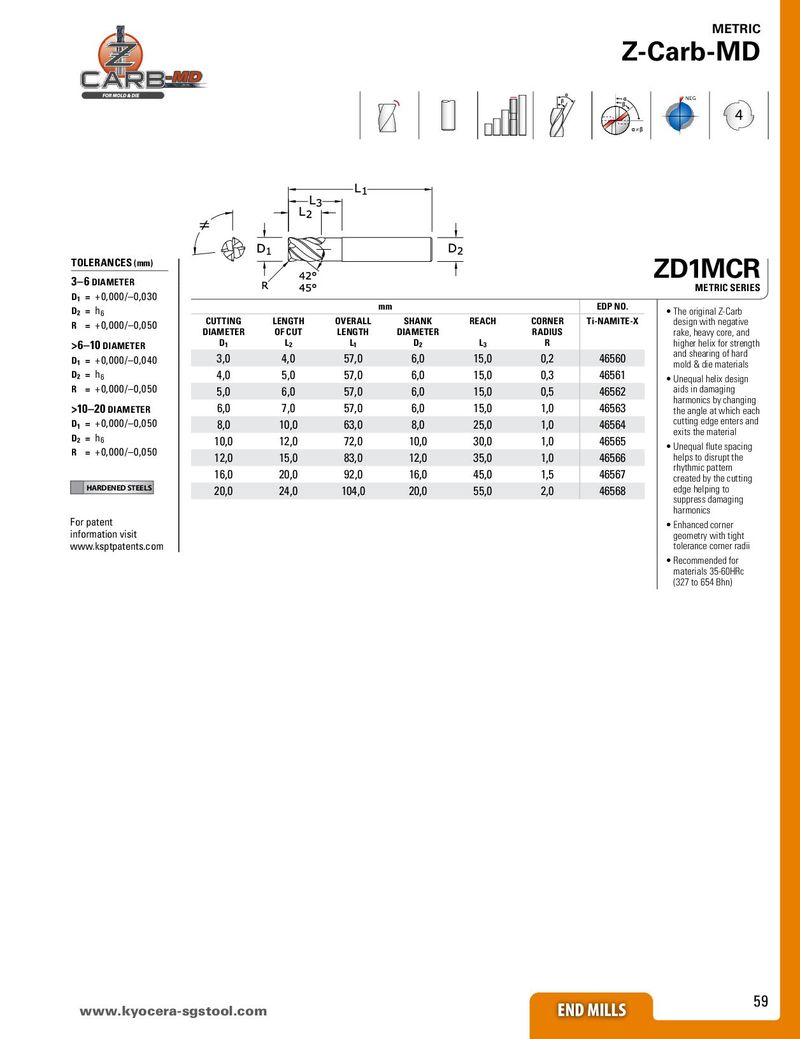
METRIC
Z-Carb-MD
NEG
4
≠
TOLERANCES (mm)
3–6 DIAMETER
ZD1MCR METRIC SERIES
D1 = +0,000/–0,030
D2 = h6 mm EDP NO. • The original Z-Carb
R = +0,000/–0,050 CUTTING LENGTH OVERALL SHANK REACH CORNER Ti-NAMITE-X design with negative
DIAMETER OF CUT LENGTH DIAMETER RADIUS rake, heavy core, and
>6–10 DIAMETER D1 L2 L1 D2 L3 R higher helix for strength
and shearing of hard
D1 = +0,000/–0,040 3,0 4,0 57,0 6,0 15,0 0,2 46560 mold & die materials
D2 = h6 4,0 5,0 57,0 6,0 15,0 0,3 46561 • Unequal helix design
R = +0,000/–0,050 5,0 6,0 57,0 6,0 15,0 0,5 46562 aids in damaging
harmonics by changing
>10–20 DIAMETER 6,0 7,0 57,0 6,0 15,0 1,0 46563 the angle at which each
D1 = +0,000/–0,050 8,0 10,0 63,0 8,0 25,0 1,0 46564 cutting edge enters and
exits the material
D2 = h6 10,0 12,0 72,0 10,0 30,0 1,0 46565 • Unequal flute spacing
R = +0,000/–0,050
12,0 15,0 83,0 12,0 35,0 1,0 46566 helps to disrupt the
rhythmic pattern
16,0 20,0 92,0 16,0 45,0 1,5 46567 created by the cutting
HARDENED STEELS
20,0 24,0 104,0 20,0 55,0 2,0 46568 edge helping to
suppress damaging
harmonics
For patent • Enhanced corner
information visit geometry with tight
www.ksptpatents.com tolerance corner radii
• Recommended for
materials 35-60HRc
(327 to 654 Bhn)
59
END MILLS
www.kyocera-sgstool.com END MILLS