Общий каталог SGS 2018 - страница 42
Навигация
 Каталог SGS шестизубые фрезы T-carb
 Каталог SGS микро инструмент 2021
 Каталог SGS фрезы для алюминия S-carb
 Каталог SGS высокопроизводительные черновые фрезы
 Каталог SGS инструмент для обработки алюминия
 Общий каталог SGS 2015 на русском
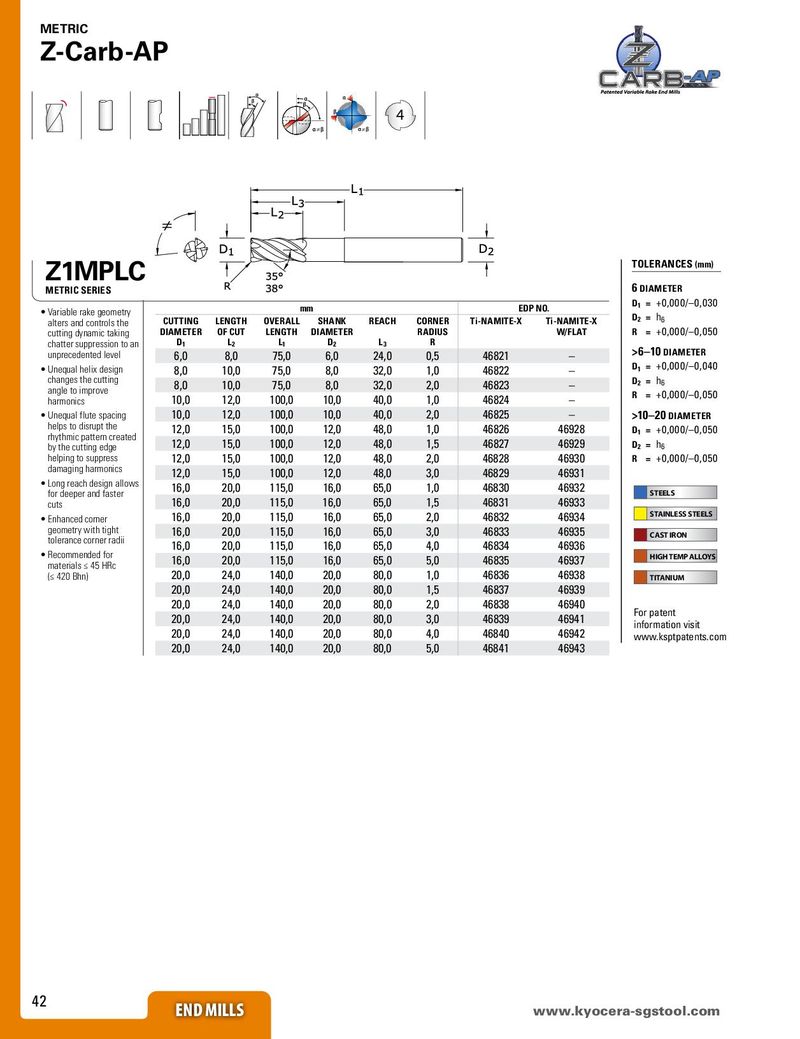
METRIC
Z-Carb-AP
4
≠ ≠
Z1MPLC TOLERANCES (mm)
6 DIAMETER
METRIC SERIES
D1 = +0,000/–0,030
• Variable rake geometry mm EDP NO.
CUTTING LENGTH OVERALL SHANK REACH CORNER Ti-NAMITE-X Ti-NAMITE-X D2 = h6
alters and controls the
cutting dynamic taking DIAMETER OF CUT LENGTH DIAMETER RADIUS W/FLAT R = +0,000/–0,050
chatter suppression to an D1 L2 L1 D2 L3 R
unprecedented level 6,0 8,0 75,0 6,0 24,0 0,5 46821 – >6–10 DIAMETER
D1 = +0,000/–0,040
• Unequal helix design 8,0 10,0 75,0 8,0 32,0 1,0 46822 –
changes the cutting D2 = h6
angle to improve 8,0 10,0 75,0 8,0 32,0 2,0 46823 –
R = +0,000/–0,050
harmonics 10,0 12,0 100,0 10,0 40,0 1,0 46824 –
• Unequal flute spacing 10,0 12,0 100,0 10,0 40,0 2,0 46825 – >10–20 DIAMETER
helps to disrupt the 12,0 15,0 100,0 12,0 48,0 1,0 46826 46928 D1 = +0,000/–0,050
rhythmic pattern created
by the cutting edge 12,0 15,0 100,0 12,0 48,0 1,5 46827 46929 D2 = h6
helping to suppress 12,0 15,0 100,0 12,0 48,0 2,0 46828 46930 R = +0,000/–0,050
damaging harmonics
12,0 15,0 100,0 12,0 48,0 3,0 46829 46931
• Long reach design allows
for deeper and faster
16,0 20,0 115,0 16,0 65,0 1,0 46830 46932 STEELS
cuts 16,0 20,0 115,0 16,0 65,0 1,5 46831 46933
• Enhanced corner 16,0 20,0 115,0 16,0 65,0 2,0 46832 46934 STAINLESS STEELS
geometry with tight 16,0 20,0 115,0 16,0 65,0 3,0 46833 46935 CAST IRON
tolerance corner radii
16,0 20,0 115,0 16,0 65,0 4,0 46834 46936
• Recommended for HIGH TEMP ALLOYS
materials ≤ 45 HRc 16,0 20,0 115,0 16,0 65,0 5,0 46835 46937
(≤ 420 Bhn) 20,0 24,0 140,0 20,0 80,0 1,0 46836 46938 TITANIUM
20,0 24,0 140,0 20,0 80,0 1,5 46837 46939
20,0 24,0 140,0 20,0 80,0 2,0 46838 46940
For patent
20,0 24,0 140,0 20,0 80,0 3,0 46839 46941 information visit
20,0 24,0 140,0 20,0 80,0 4,0 46840 46942 www.ksptpatents.com
20,0 24,0 140,0 20,0 80,0 5,0 46841 46943
42
END MILLS END MILLS
www.kyocera-sgstool.com