Общий каталог SGS 2018 - страница 21
Навигация
 Каталог SGS шестизубые фрезы T-carb
 Каталог SGS микро инструмент 2021
 Каталог SGS фрезы для алюминия S-carb
 Каталог SGS высокопроизводительные черновые фрезы
 Каталог SGS инструмент для обработки алюминия
 Общий каталог SGS 2015 на русском
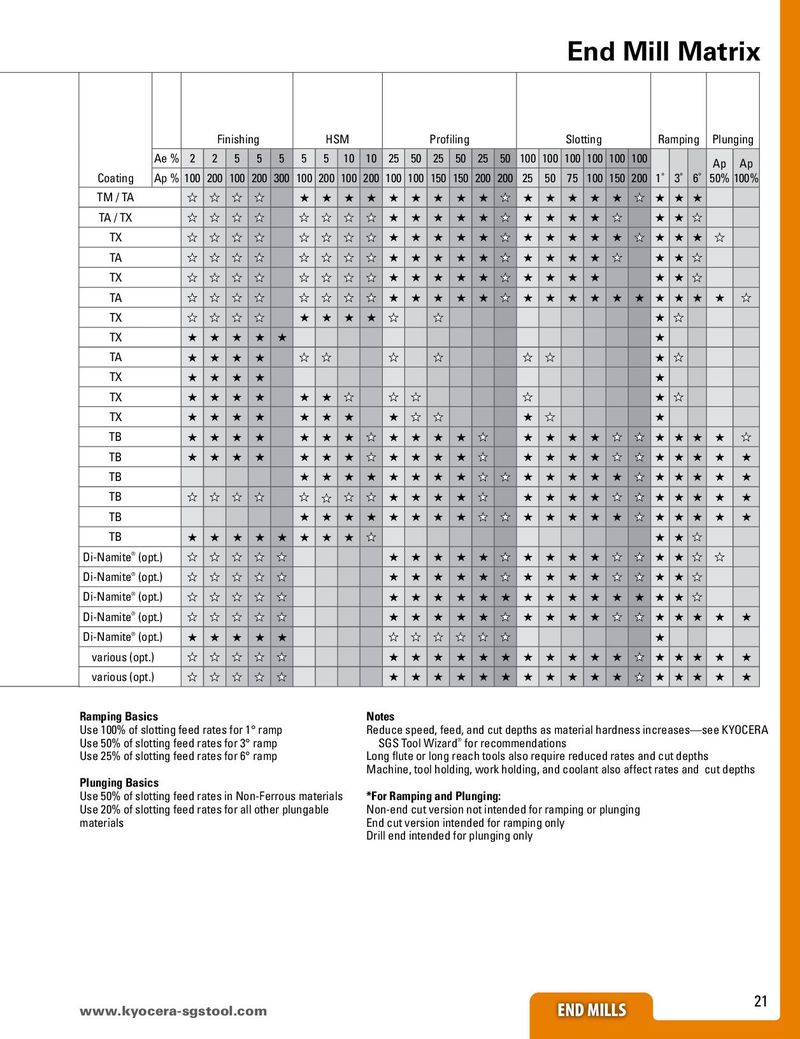
End Mill Matrix
Material
| Fi | nishi | ng | H | SM | Pro | fili | ng | Slot | ting | R | a | mp | ing | Plun | ging | |||||||||||||
| Ae % | 2 | 2 | 5 | 5 | 5 | 5 | 5 | 10 | 10 | 25 | 50 | 25 | 50 | 25 50 | 100 | 100 | 100 | 100 | 1 | 00 | 100 | Ap | Ap | |||||
| Coating Ap % | 100 | 200 | 100 | 200 | 300 | 100 | 200 | 100 | 200 | 100 | 100 | 150 | 1 | 50 | 200 200 | 25 | 50 | 75 | 100 | 1 | 50 | 200 | 1˚ | 3˚ | 6˚ | 50% | 100% | |
| TM / TA | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | |||||||||||
| TA / TX | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | |||||||||||||||||
| TX | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | |||||||||||||||
| TA | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | |||||||||||||||||
| TX | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | |||||||||||||||||
| TA | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | |||||||||||||
| TX | ★ | ★ | ★ | ★ | ★ | |||||||||||||||||||||||
| TX | ★ | ★ | ★ | ★ | ★ | ★ | ||||||||||||||||||||||
| TA | ★ | ★ | ★ | ★ | ★ | |||||||||||||||||||||||
| TX | ★ | ★ | ★ | ★ | ★ | |||||||||||||||||||||||
| TX | ★ | ★ | ★ | ★ | ★ | ★ | ★ | |||||||||||||||||||||
| TX | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ||||||||||||||||||
| TB | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | |||||||||
| TB | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ||||||||
| TB | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ||||||||||
| TB | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | |||||||||||||||
| TB | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ||||||||||
| TB | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ||||||||||||||||||
| Di-Namite ®(opt.) | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | |||||||||||||||||
| Di-Namite ®(opt.) | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | |||||||||||||||||
| Di-Namite ®(opt.) | ★ | ★ | ★ | ★ | ★ ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | |||||||||||||||
| Di-Namite ®(opt.) | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ||||||||||||||
| Di-Namite ®(opt.) | ★ | ★ | ★ | ★ | ★ | ★ | ||||||||||||||||||||||
| various (opt.) | ★ | ★ | ★ | ★ | ★ ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | |||||||||||||
| various (opt.) | ★ | ★ | ★ | ★ | ★ ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ | ★ |
Ramping Basics Notes Use 100% of slotting feed rates for 1° ramp Reduce speed, feed, and cut depths as material hardness increases—see KYOCERA Use 50% of slotting feed rates for 3° ramp SGS Tool Wizard® for recommendations
| Use 25% of slotting feed rates for 6° ramp | Long flute or long reach tools also require reduced rates and cut depths |
| Machine, tool holding, work holding, and coolant also affect rates and cut depths | |
| Plunging Basics | |
| Use 50% of slotting feed rates in Non-Ferrous materials | *For Ramping and Plunging: |
| Use 20% of slotting feed rates for all other plungable | Non-end cut version not intended for ramping or plunging |
| materials | End cut version intended for ramping only |
Drill end intended for plunging only