Общий каталог SGS 2018 - страница 115
Навигация
 Каталог SGS шестизубые фрезы T-carb
 Каталог SGS микро инструмент 2021
 Каталог SGS фрезы для алюминия S-carb
 Каталог SGS высокопроизводительные черновые фрезы
 Каталог SGS инструмент для обработки алюминия
 Общий каталог SGS 2015 на русском
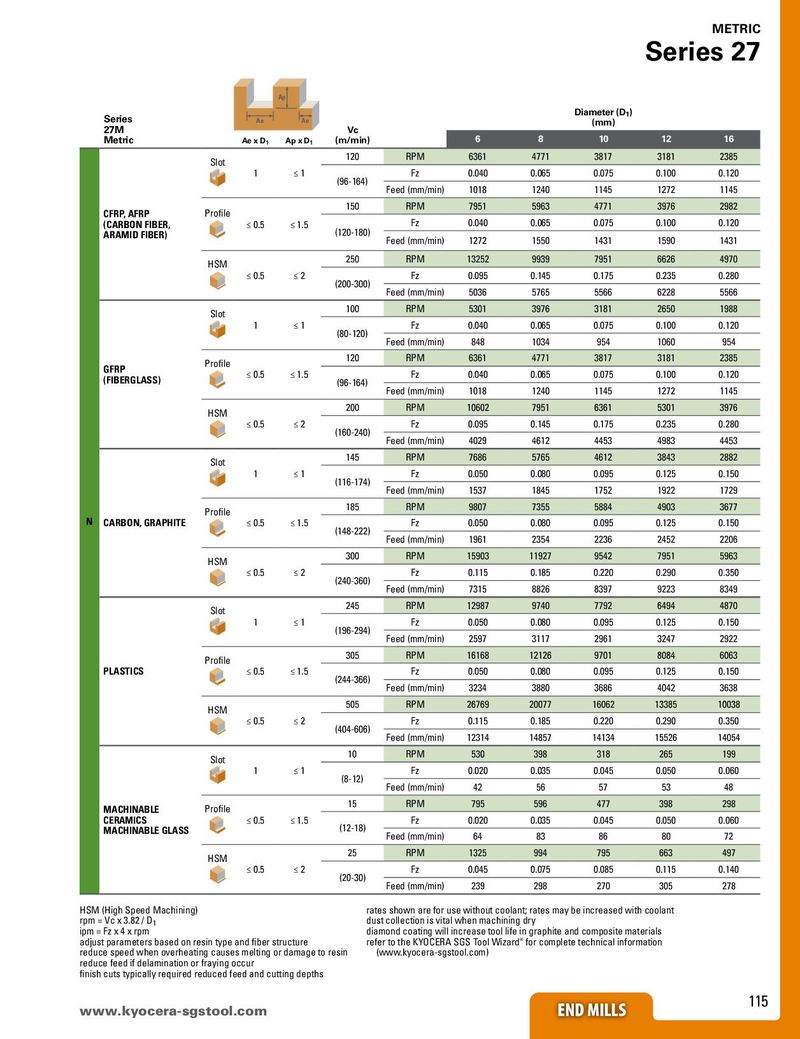
| Series 27M | Ae | Ap Ae | Vc | Diameter (D1) (mm) | ||||||
| Metric | Ae x D1 | Ap x D1 | (m/min) | 6 | 8 | 10 | 12 | 16 | ||
| Slot | 120 | RPM | 6361 | 4771 | 3817 | 3181 | 2385 | |||
| 1 | ≤ 1 | Fz | 0.040 | 0.065 | 0.075 | 0.100 | 0.120 | |||
| (96-164) | Feed (mm/min) | 1018 | 1240 | 1145 | 1272 | 1145 | ||||
| CFRP AFRP | Profile | 150 | RPM | 7951 | 5963 | 4771 | 3976 | 2982 | ||
| , (CARBON FIBER, | ≤ 0.5 | ≤ 1.5 | Fz | 0.040 | 0.065 | 0.075 | 0.100 | 0.120 | ||
| ARAMID FIBER) | (120-180) | Feed (mm/min) | 1272 | 1550 | 1431 | 1590 | 1431 | |||
| HSM | 250 | RPM | 13252 | 9939 | 7951 | 6626 | 4970 | |||
| ≤ 0.5 | ≤ 2 | (200-300) | Fz | 0.095 | 0.145 | 0.175 | 0.235 | 0.280 | ||
| Feed (mm/min) | 5036 | 5765 | 5566 | 6228 | 5566 | |||||
| Slot | 100 | RPM | 5301 | 3976 | 3181 | 2650 | 1988 | |||
| 1 | ≤ 1 | Fz | 0.040 | 0.065 | 0.075 | 0.100 | 0.120 | |||
| (80-120) | Feed (mm/min) | 848 | 1034 | 954 | 1060 | 954 | ||||
| Profile | 120 | RPM | 6361 | 4771 | 3817 | 3181 | 2385 | |||
| GFRP (FIBERGLASS) | ≤ 0.5 | ≤ 1.5 | (96164) | Fz | 0.040 | 0.065 | 0.075 | 0.100 | 0.120 | |
| - | Feed (mm/min) | 1018 | 1240 | 1145 | 1272 | 1145 | ||||
| HSM | 200 | RPM | 10602 | 7951 | 6361 | 5301 | 3976 | |||
| ≤ 0.5 | ≤ 2 | Fz | 0.095 | 0.145 | 0.175 | 0.235 | 0.280 | |||
| (160-240) | Feed (mm/min) | 4029 | 4612 | 4453 | 4983 | 4453 | ||||
| Slot | 145 | RPM | 7686 | 5765 | 4612 | 3843 | 2882 | |||
| 1 | ≤ 1 | Fz | 0.050 | 0.080 | 0.095 | 0.125 | 0.150 | |||
| (116-174) | Feed (mm/min) | 1537 | 1845 | 1752 | 1922 | 1729 | ||||
| Profile | 185 | RPM | 9807 | 7355 | 5884 | 4903 | 3677 | |||
| N CARBON, GRAPHITE | ≤ 0.5 | ≤ 1.5 | (148222) | Fz | 0.050 | 0.080 | 0.095 | 0.125 | 0.150 | |
| - | Feed (mm/min) | 1961 | 2354 | 2236 | 2452 | 2206 | ||||
| HSM | 300 | RPM | 15903 | 11927 | 9542 | 7951 | 5963 | |||
| ≤ 0.5 | ≤ 2 | (240-360) | Fz | 0.115 | 0.185 | 0.220 | 0.290 | 0.350 | ||
| Feed (mm/min) | 7315 | 8826 | 8397 | 9223 | 8349 | |||||
| Slot | 245 | RPM | 12987 | 9740 | 7792 | 6494 | 4870 | |||
| 1 | ≤ 1 | (196294) | Fz | 0.050 | 0.080 | 0.095 | 0.125 | 0.150 | ||
| - | Feed (mm/min) | 2597 | 3117 | 2961 | 3247 | 2922 | ||||
| Profile | 305 | RPM | 16168 | 12126 | 9701 | 8084 | 6063 | |||
| PLASTICS | ≤ 0.5 | ≤ 1.5 | 244366 | Fz | 0.050 | 0.080 | 0.095 | 0.125 | 0.150 | |
| (-) | Feed (mm/min) | 3234 | 3880 | 3686 | 4042 | 3638 | ||||
| HSM | 505 | RPM | 26769 | 20077 | 16062 | 13385 | 10038 | |||
| ≤ 0.5 | ≤ 2 | Fz | 0.115 | 0.185 | 0.220 | 0.290 | 0.350 | |||
| (404-606) | Feed (mm/min) | 12314 | 14857 | 14134 | 15526 | 14054 | ||||
| Slot | 10 | RPM | 530 | 398 | 318 | 265 | 199 | |||
| 1 | ≤ 1 | Fz | 0.020 | 0.035 | 0.045 | 0.050 | 0.060 | |||
| (8-12) | Feed (mm/min) | 42 | 56 | 57 | 53 | 48 | ||||
| MACHINABLE | Profile | 15 | RPM | 795 | 596 | 477 | 398 | 298 | ||
| CERAMICS | ≤ 0.5 | ≤ 1.5 | Fz | 0.020 | 0.035 | 0.045 | 0.050 | 0.060 | ||
| MACHINABLE GLASS | (12-18) | Feed (mm/min) | 64 | 83 | 86 | 80 | 72 | |||
| HSM | 25 | RPM | 1325 | 994 | 795 | 663 | 497 | |||
| ≤ 0.5 | ≤ 2 | Fz | 0.045 | 0.075 | 0.085 | 0.115 | 0.140 | |||
| (20-30) | Feed (mm/min) | 239 | 298 | 270 | 305 | 278 |
| HSM (High Speed Machining) | rates shown are for use without coolant; rates may be increased with coolant |
| rpm = Vc x 3.82 / D | dust collection is vital when machining dry |
| 1 | |
| ipm = Fz x 4 x rpm | diamond coating will increase tool life in graphite and composite materials |
| adjust parameters based on resin type and fiber structure | refer to the KYOCERA SGS Tool Wizard® for complete technical information |
| reduce speed when overheating causes melting or damage to resin | (www.kyocera-sgstool.com) |
reduce feed if delamination or fraying occur finish cuts typically required reduced feed and cutting depths