Каталог SGS инструмент для обработки алюминия - страница 49
Навигация
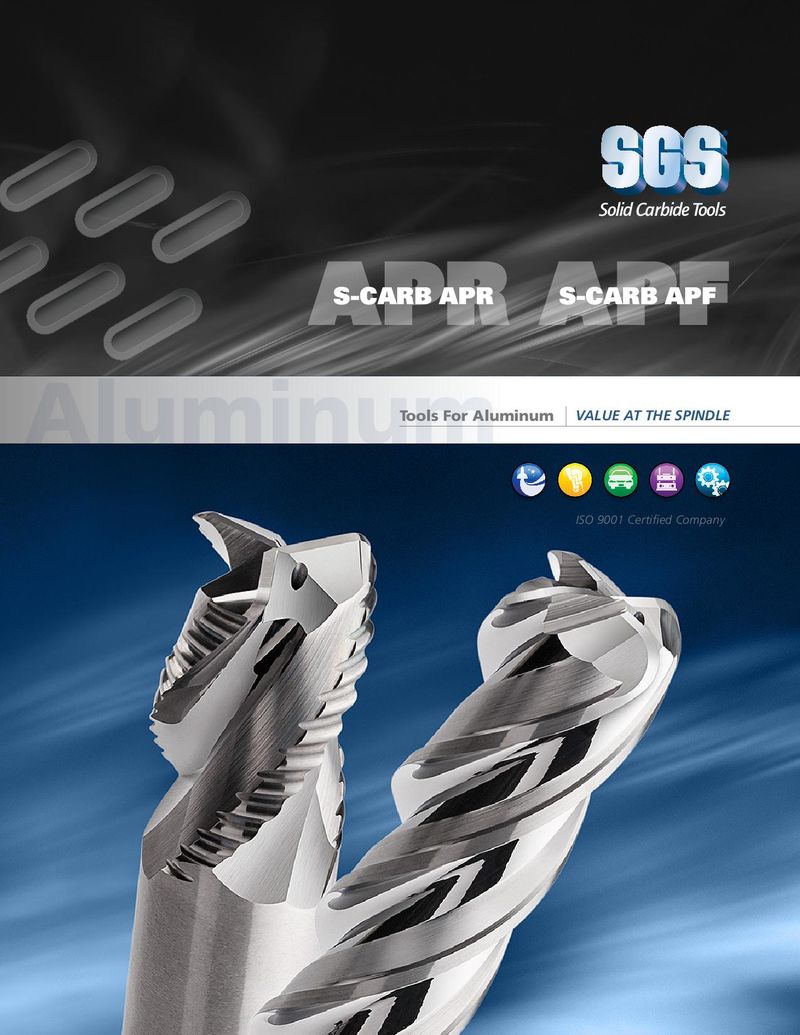 Каталог SGS фрезы для алюминия S-carb
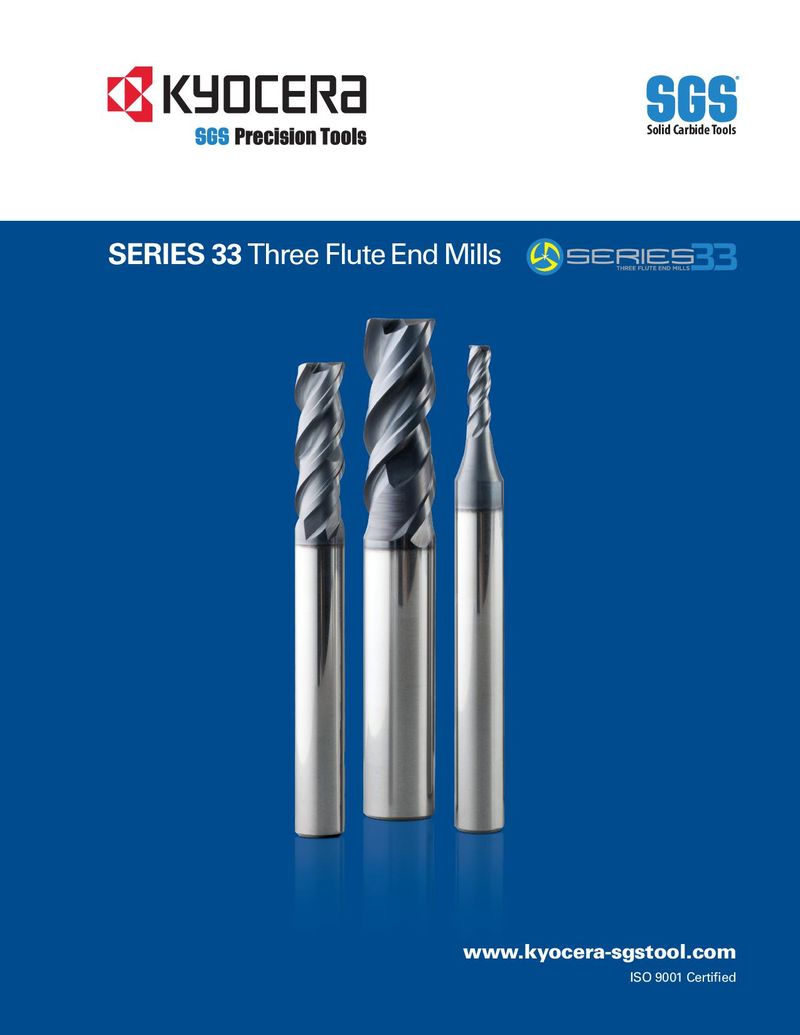 Каталог SGS фрезы для труднообрабатываемых материалов Series 33
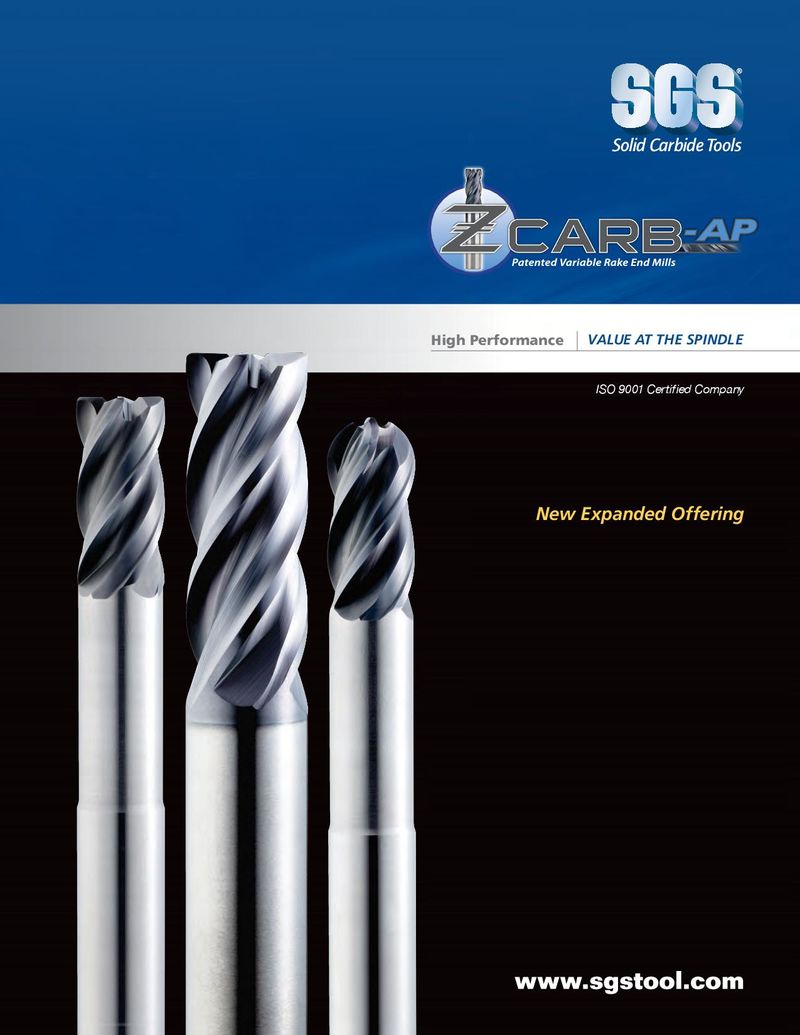 Каталог SGS фрезы с переменным углом спирали Z-carb
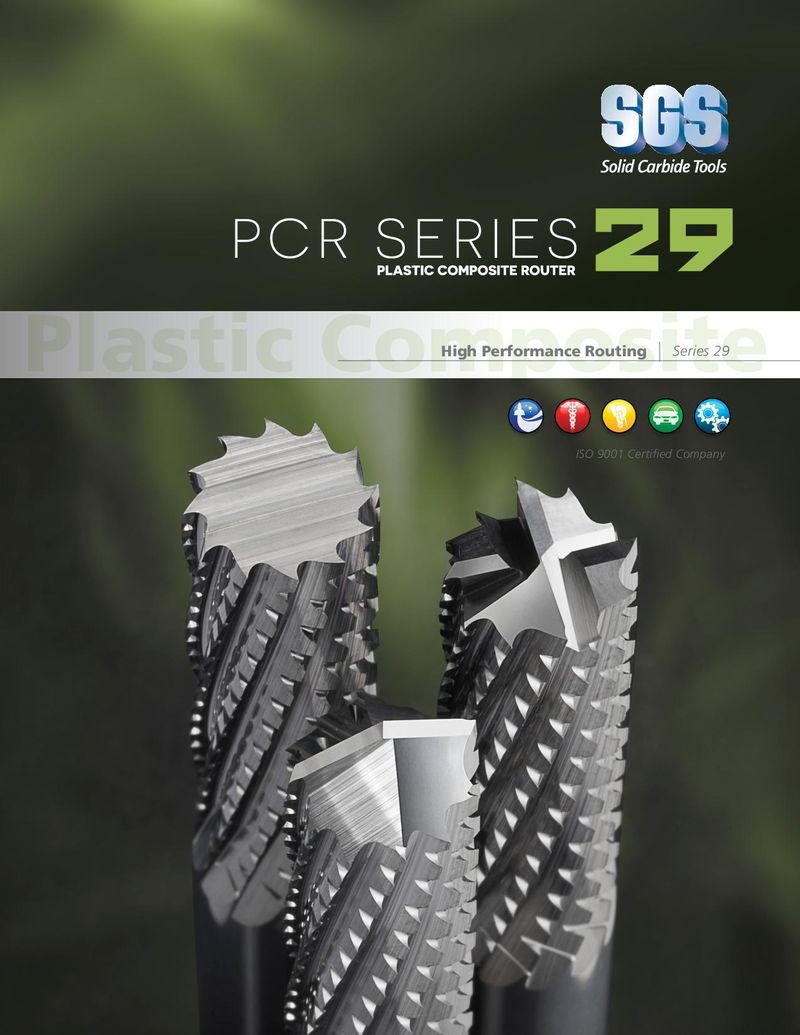 Каталог SGS фрезы для обработки пластика PCR series
 Каталог SGS микро инструмент 2021
 Каталог SGS шестизубые фрезы T-carb
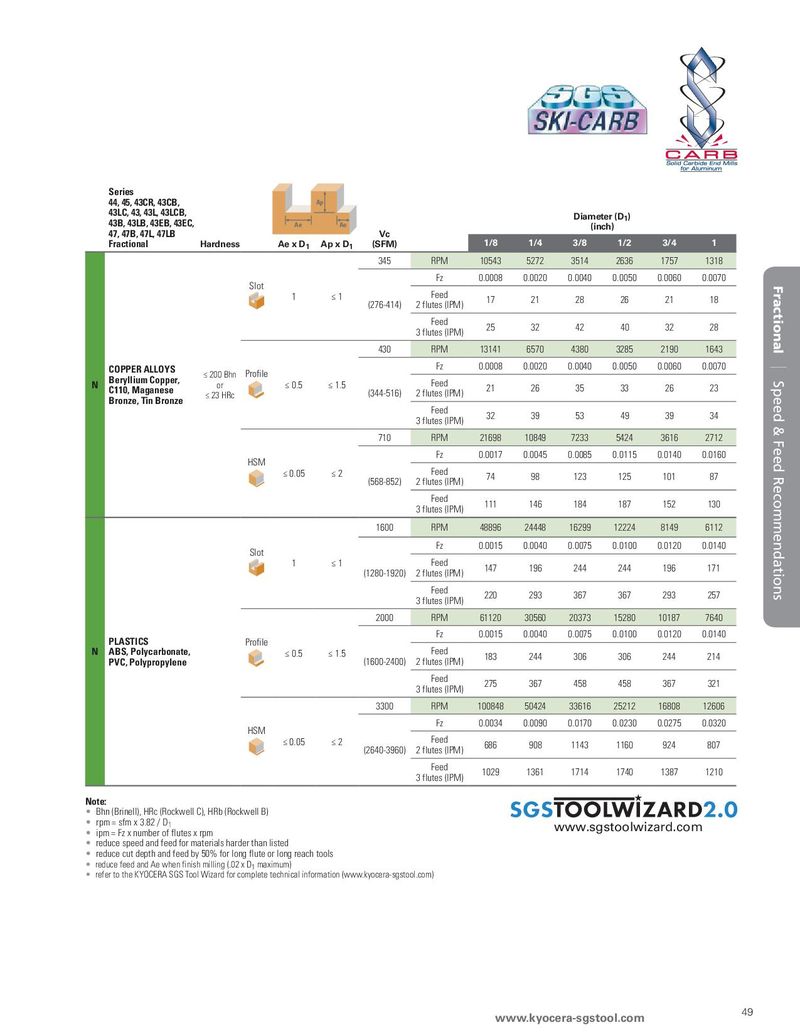
Series 44, 45, 43CR, 43CB, Ap 43LC, 43, 43L, 43LCB, Diameter (D ) 43B, 43LB, 43EB, 43EC, 1
| Ae | Ae | (inch) | ||
| 47, 47B, 47L, 47LB | Vc |
| ApxD AexD Hardness Fractional (SFM) | 1/8 | 1/4 | 3/8 | 1/2 | 3/4 | 1 | |
| 1 1 | |||||||
| 345 | RPM | 10543 | 5272 | 3514 | 2636 | 1757 | 1318 |
| Fz | 0.0008 | 0.0020 | 0.0040 | 0.0050 | 0.0060 | 0.0070 | |
| Slot | |||||||
| ≤ 1 1 | Feed | 17 | 21 | 28 | 26 | 21 | 18 |
| (276-414) | 2 flutes (IPM) | ||||||
| Feed | 25 | 32 | 42 | 40 | 32 | 28 | |
| 3 flutes (IPM) | |||||||
| 430 | RPM | 13141 | 6570 | 4380 | 3285 | 2190 | 1643 |
| COPPER ALLOYS | Fz | 0.0008 | 0.0020 | 0.0040 | 0.0050 | 0.0060 | 0.0070 |
- 200 Bhn Profile
N Beryllium Copper, Feed
C110, Maganese or 0.5 1.5 21 26 35 33 26 23
| ≤ 23 HRc | (344-516) | 2 flutes (IPM) | |
| Bronze, Tin Bronze |
| Feed | 32 | 39 | 53 | 49 | 39 | 34 | ||
| 3 flutes (IPM) | ||||||||
| 710 | RPM | 21698 | 10849 | 7233 | 5424 | 3616 | 2712 | |
| Fz | 0.0017 | 0.0045 | 0.0085 | 0.0115 | 0.0140 | 0.0160 |
HSM
- 0.05
- 2 Feed 74 98 123 125 101 87
(568-852) 2 flutes (IPM)
| Feed | 111 | 146 | 184 | 187 | 152 | 130 | |
| 3 flutes (IPM) | |||||||
| 1600 | RPM | 48896 | 24448 | 16299 | 12224 | 8149 | 6112 |
| Fz | 0.0015 | 0.0040 | 0.0075 | 0.0100 | 0.0120 | 0.0140 | |
| Slot | |||||||
| ≤ 1 1 | Feed | 147 | 196 | 244 | 244 | 196 | 171 |
| (1280-1920) 2 flutes (IPM) | |||||||
| Feed | 220 | 293 | 367 | 367 | 293 | 257 | |
| 3 flutes (IPM) | |||||||
| 2000 | RPM | 61120 | 30560 | 20373 | 15280 | 10187 | 7640 |
| Fz | 0.0015 | 0.0040 | 0.0075 | 0.0100 | 0.0120 | 0.0140 | |
| Profile PLASTICS | |||||||
| ≤ 1.5 ≤ 0.5 ABS, Polycarbonate, N | Feed | 183 | 244 | 306 | 306 | 244 | 214 |
PVC, Polypropylene (1600-2400) 2 flutes (IPM)
| Feed | 275 | 367 | 458 | 458 | 367 | 321 | ||
| 3 flutes (IPM) | ||||||||
| 3300 | RPM | 100848 | 50424 | 33616 | 25212 | 16808 | 12606 | |
| Fz | 0.0034 | 0.0090 | 0.0170 | 0.0230 | 0.0275 | 0.0320 |
HSM
- 0.05
- 2 Feed 686 908 1143 1160 924 807
(2640-3960) 2 flutes (IPM)
Feed 1029 1361 1714 1740 1387 1210
3 flutes (IPM) Note:
- Bhn (Brinell), HRc (Rockwell C), HRb (Rockwell B)
- rpm = sfm x 3.82 / D1 www.sgstoolwizard.com
- ipm = Fz x number of flutes x rpm
- reduce speed and feed for materials harder than listed
- reduce cut depth and feed by 50% for long flute or long reach tools
- reduce feed and Ae when finish milling (.02 x D1 maximum)
- refer to the KYOCERA SGS Tool Wizard for complete technical information (www.kyocera-sgstool.com)