Общий каталог Osawa 2021 - страница 172
Навигация
 Общий каталог Osawa 2018
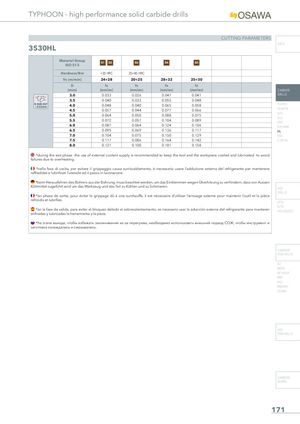
TYPHOON - high performance solid carbide drills
CUTTING PARAMETERS
| Material Group ISO 513 | S1 S2 | S3 | S4 | S5 | |
| Hardness/Rm | 35÷45 HRC | ||||
| Vc (m/min) | 24÷28 | 20÷25 | 28÷32 | 25÷30 | |
| D (mm) | fn (mm/rev) | fn (mm/rev) | fn (mm/rev) | fn (mm/rev) | |
| 3.0 | 0.033 | 0.026 | 0.047 | 0.041 | |
| 3.5 | 0.040 | 0.033 | 0.055 | 0.048 | |
| Ø RUN OUT | 4.0 | 0.048 | 0.040 | 0.065 | 0.058 |
| 4.5 | 0.057 | 0.044 | 0.077 | 0.066 | |
| 5.0 | 0.064 | 0.050 | 0.088 | 0.075 | |
| 5.5 | 0.072 | 0.057 | 0.104 | 0.089 | |
| 6.0 | 0.087 | 0.064 | 0.124 | 0.106 | |
| 6.5 | 0.095 | 0.069 | 0.136 | 0.117 | |
| 7.0 | 0.104 | 0.075 | 0.150 | 0.129 | |
| 7.5 | 0.117 | 0.086 | 0.164 | 0.142 | |
| 8.0 | 0.121 | 0.100 | 0.181 | 0.158 |
INFO
SUH ALH HRC SUH MINI
*during the exit phase the use of external coolant supply is recommended to keep the tool and the workpiece cooled and lubricated to avoid failures due to overheating. *nella fase di uscita, per evitare il grippaggio causa surriscaldamento, è necessario usare l’adduzione esterna del refrigerante per mantenere raff reddati e lubrifi cati l’utensile ed il pezzo in lavorazione. *beim Herausfahren des Bohrers aus der Bohrung, muss beachtet werden, um das Einklemmen wegen Überhitzung zu verhindern, dass von Aussen Kühlmittel zugeführt wird um das Werkzeug und das Teil zu Kühlen und zu Schmieren. *en phase de sortie, pour éviter le grippage dû à une surchauff e, il est nécessaire d’utiliser l’arrosage externe pour maintenir l’outil et la pièce refroidis et lubrifi és. *en la fase de salida, para evitar el bloqueo debido al sobrecalentamiento, es necesario usar la aducción externa del refrigerante para mantener enfriadas y lubricadas la herramienta y la pieza. *hа этапе выхода, чтобы избежать заклинивания из-за перегрева, необходимо использовать внешний подвод СОЖ, чтобы инструмент и заготовка охлаждались и смазывались.
HSS DRILLS
LFTA SUTA HSS-HSS/CO
CARBIDE END-MILLS
G2 MDTA HF VH/UP MEF ALU MEX/MH UH/MH
HSS END-MILLS
CARBIDE BURRS