Общий каталог Osawa 2021 - страница 111
Навигация
 Общий каталог Osawa 2018
TYPHOON SUH MINI HIGH PERFORMANCE - MINIATURE SHORT AND LONG INFO
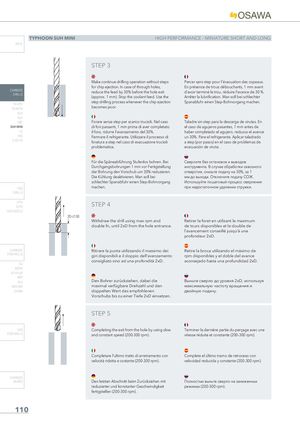
STEP 3
Make continue drilling operation without steps Percer sans step pour l'évacuation des copeaux. for chip ejection. In case of through holes, En présence de trous débouchants, 1 mm avant
CARBIDE reduce the feed by 30% before the hole exit d’avoir terminé le trou, réduire l’avance de 30 %.
DRILLS (approx. 1 mm). Stop the coolant feed. Use the Arrêter la lubrification. Man soll bei schlechter step drilling process whenever the chip ejection Spanabfuhr einen Step-Bohrvorgang machen. PU-HPU
becomes poor. TA-4HTA SUH ALH
| HRC | Forare senza step per scarico trucioli. Nel caso | Taladre sin step para la descarga de virutas. En | |
| SUH MINI | di fori passanti, 1 mm prima di aver completato | el caso de agujeros pasantes, 1 mm antes de | |
| HL | il foro, ridurre l’avanzamento del 30%. | haber completado el agujero, reduzca el avance | |
| HSD | Fermare il refrigerante. Utilizzare il processo di | un 30%. Pare el refrigerante. Aplicar taladrado | |
| C-SD-TA | foratura a step nel caso di evacuazione trucioli | a step (por pasos) en el caso de problemas de |
problematica. evacuación de viruta.
HSS DRILLS LFTA SUTA HSS-HSS/CO
2D÷2.5D
| Für die Späneabführung Stufenlos bohren. Bei | Сверлите без остановок и выводов |
| Durchgangsbohrungen 1 mm vor Fertigstellung | инструмента. В случае обработки сквозного |
| der Bohrung den Vorschub um 30% reduzieren. | отверстия, снизьте подачу на 30%, за 1 |
| Die Kühlung deaktivieren. Man soll bei | мм до выхода. Отключите подачу СОЖ. |
| schlechter Spanabfuhr einen Step-Bohrvorgang | Используйте пошаговый процесс сверления |
| machen. | при недостаточном удалении стружки. |
STEP 4
| Withdraw the drill using max rpm and | Retirer le foret en utilisant le maximum |
| double fn, until 2xD from the hole entrance. | de tours disponibles et le double de |
l’avancement conseillé jusqu’à une profondeur 2xD.
| CARBIDE | Ritirare la punta utilizzando il massimo dei | Retire la broca utilizando el máximo de |
| END-MILLS | giri disponibili e il doppio dell’avanzamento | rpm disponibles y el doble del avance |
consigliato sino ad una profondità 2xD. aconsejado hasta una profundidad 2xD. G2 MDTA HF VH/UP
MEF Den Bohrer zurückziehen, dabei die Выньте сверло до уровня 2хD, используя ALU
| MEX/MH | maximal verfügbare Drehzahl und den | максимальную частоту вращения и |
| UH/MH | doppelten Wert des empfohlenen | двойную подачу. |
Vorschubs bis zu einer Tiefe 2xD einsetzen.
STEP 5
| HSS | Completing the exit from the hole by using slow | Terminer la dernière partie du perçage avec une | |
| END-MILLS | and constant speed (200-300 rpm). | vitesse réduite et constante (200-300 rpm). |
Completare l’ultimo tratto di arretramento con Complete el último tramo de retroceso con velocità ridotta e costante (200-300 rpm). velocidad reducida y constante (200-300 rpm).
CARBIDE
BURRS Den letzten Abschnitt beim Zurückziehen mit Полностью выньте сверло на заниженных
reduzierter und konstanter Geschwindigkeit режимах (200-300 rpm). fertigstellen (200-300 rpm).