Основной каталог Kyocera 2016-2017 - страница 77
Навигация
 Каталог Kyocera фрезы MFH для высокоскоростной обработки
 Каталог Kyocera фрезы MEC высокопроизводительные концевые и торцевые фрезы
 Каталог микроинструмента Kyocera 2015-2016
 Каталог Kyocera высокоэффективные сверла со сменными пластинами DRV
 Каталог Kyocera пластины TQ для нарезания резьбы c прессованным стружколомом
 Каталог Kyocera высокопроизводительные модульные сверла DRA
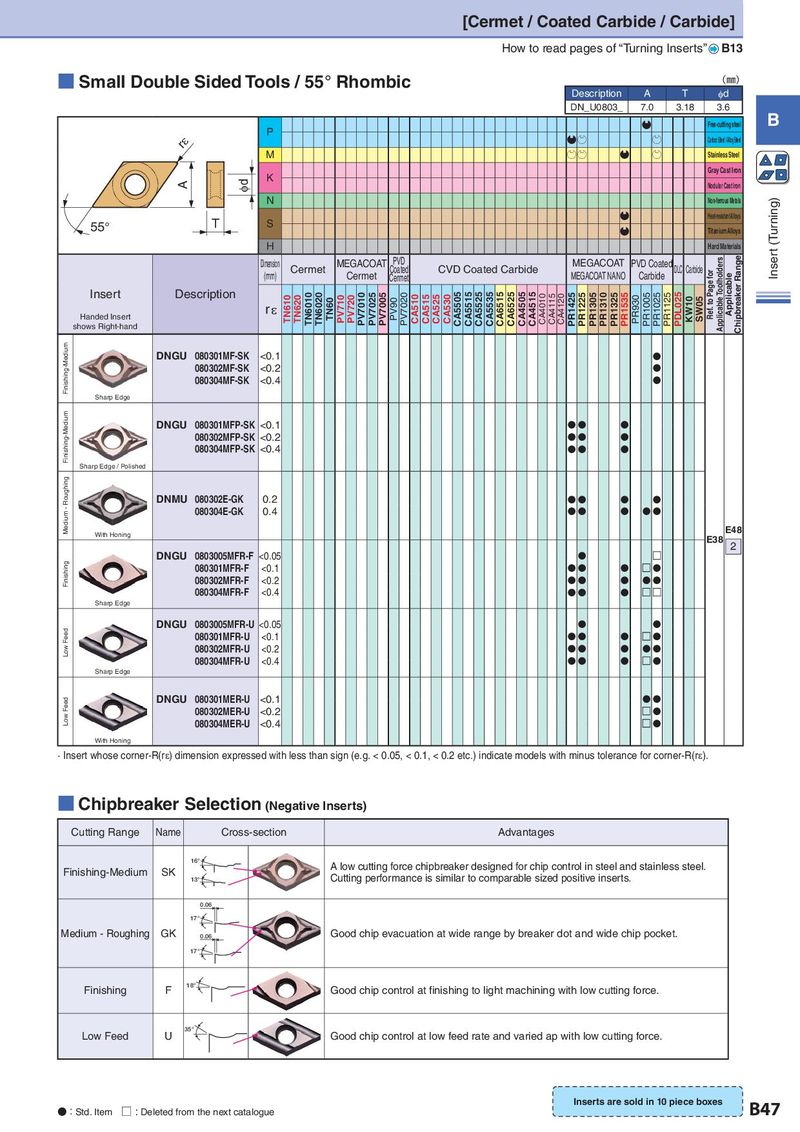
- Small Double Sided Tools / 55° Rhombic (㎜)
| Description | A | T | φd | |
| DN_U0803_ | 7.0 | 3.18 | B 3.6 | |
| Q | Free-cutting steel | |||
| P | ||||
| rH | QP | P | Carbon Steel / Alloy Steel | |
| M | PP | Q P | Stainless Steel |
Gray Cast Iron K Nodular Cast Iron N Non-ferrous Metals
Q Heat-resistant Alloys
| 55q | T | S | ||
| Q | Titanium Alloys | |||
| H | Hard Materials |
| Dimension | PVD | MEGACOAT | PVD Coated | |||
| Cermet MEGACOAT Coated | CVD Coated Carbide | |||||
| (mm) | Cermet | Cermet | MEGACOAT NANO | Carbide DLC Carbide | ||
| Insert | Description | |||||
| re | ||||||
| Handed Insert | TN610 TN620 | PV710 PV720 | PV90 PV7020 | CA510 CA515 CA525 CA530 | KW10 SW05 PR930 PR1005 PR1025 PR1125 |
| TN6010 TN6020 TN60 | PV7010 PV7025 PV7005 | CA5505 CA5515 CA5525 CA5535 CA6515 CA6525 CA4505 CA4515 | CA4010 CA4115 CA4120 | PR1425 PR1225 PR1305 PR1310 PR1325 | |
| shows Right-hand |
| DNGU 080301MF-SK | <0.1 | N | ||
| 080302MF-SK | <0.2 | N | ||
| 080304MF-SK | <0.4 | N | ||
| Sharp Edge |
| DNGU 080301MFP-SK <0.1 | N N | N | |||
| 080302MFP-SK <0.2 | N N | N | |||
| 080304MFP-SK <0.4 | N N | N | |||
| Sharp Edge / Polished | |||||
| DNMU 080302E-GK | 0.2 | N N | N | N | |
| 080304E-GK | 0.4 | N N | N | N N | |
| E48 | |||||
| With Honing | E38 | ||||
| 2 | |||||
| DNGU 0803005MFR-F <0.05 | N | U | |||
| 080301MFR-F | <0.1 | N N | N | U N | |
| 080302MFR-F | <0.2 | N N | N | N N | |
| 080304MFR-F | <0.4 | N N | N | U U | |
| Sharp Edge | |||||
| DNGU 0803005MFR-U <0.05 | N | N | |||
| 080301MFR-U | <0.1 | N N | N | U N | |
| 080302MFR-U | <0.2 | N N | N | N N | |
| 080304MFR-U | <0.4 | N N | N | U N | |
| Sharp Edge | |||||
| DNGU 080301MER-U | <0.1 | N N | |||
| 080302MER-U | <0.2 | U N | |||
| 080304MER-U | <0.4 | U N |
With Honing
- Insert whose corner-R(re) dimension expressed with less than sign (e.g. < 0.05, < 0.1, < 0.2 etc.) indicate models with minus tolerance for corner-R(re).
- Chipbreaker Selection
(Negative Inserts)
Cutting Range Name Cross-section Advantages
16° A low cutting force chipbreaker designed for chip control in steel and stainless steel. Finishing-Medium SK Cutting performance is similar to comparable sized positive inserts. 13°
0.06 17° Medium - Roughing GK Good chip evacuation at wide range by breaker dot and wide chip pocket. 0.06 17°
Finishing F 18° Good chip control at finishing to light machining with low cutting force.
Low Feed U 35° Good chip control at low feed rate and varied ap with low cutting force.