Каталог Iscar вращающийся инструмент 2017 - страница 83
Навигация
 Каталог Iscar токарные пластины ISO 2022
 Каталог Iscar инструмент для фрезерования
 Каталог Iscar решения для глубокого сверления
 Каталог Iscar полирующие фрезы
 Новые режущие инструменты Iscar 2026
 Каталог Iscar новые продукты 2018
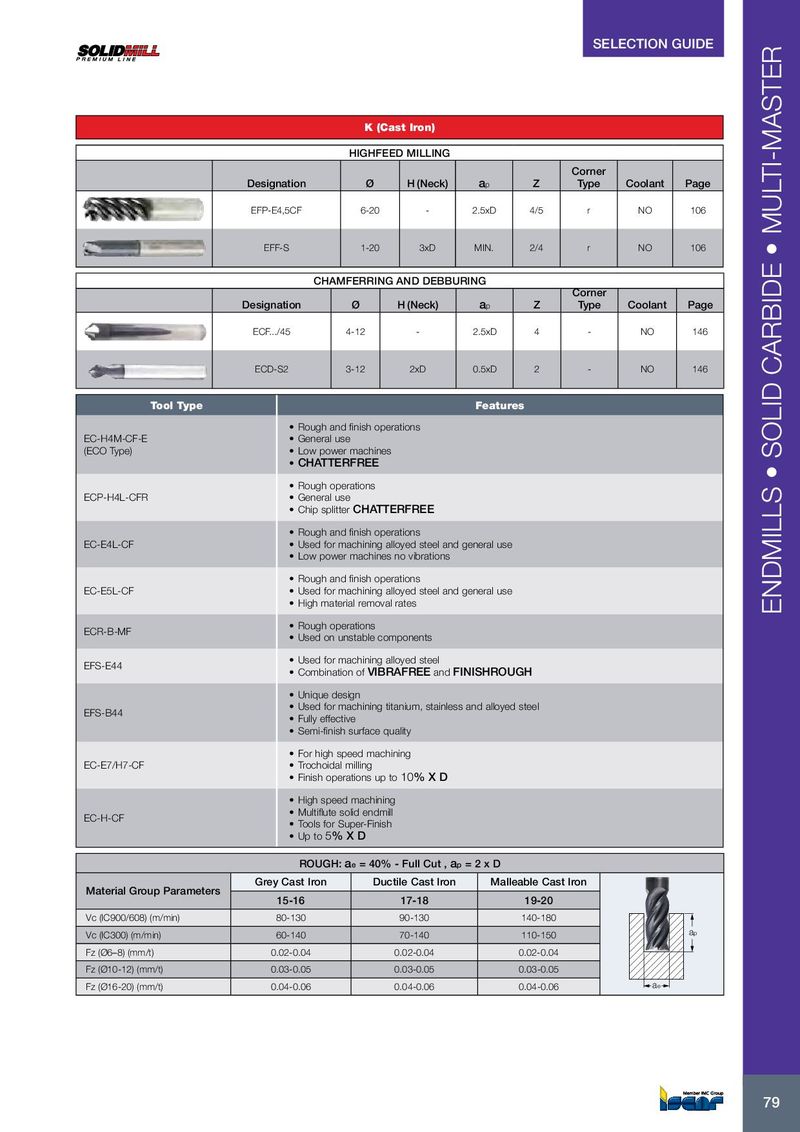
| K (C HIGHFE | ast Iron) ED MILLING | Corner | |||||
| Designation Ø | H (Neck) | ap | Z | Type | Coolant | Page | |
| EFP-E4,5CF 6-20 | - | 2.5xD | 4/5 | r | NO | 106 | |
| EFF-S 1-20 | 3xD | MIN. | 2/4 | r | NO | 106 | |
| CHAMFERRIN | G AND DEBBU | RING | Corner | ||||
| Designation Ø | H (Neck) | ap | Z | Type | Coolant | Page | |
| ECF.../45 4-12 | - | 2.5xD | 4 | - | NO | 146 | |
| ECD-S2 3-12 | 2xD | 0.5xD | 2 | - | NO | 146 | |
| Tool Type | Feature | s | |||||
| EC-H4M-CF-E (ECO Type) | • Rough and finish ope • General use • Low power machine •CHATTERFREE | rations s | |||||
| ECP-H4L-CFR | • Rough operations • General use • Chip splitterCHATT | ERFREE | |||||
| EC-E4L-CF | • Rough and finish ope • Used for machining a • Low power machine | rations lloyed steel and s no vibrations | general use | ||||
| EC-E5L-CF | • Rough and finish ope • Used for machining a • High material remova | rations lloyed steel and l rates | general use | ||||
| ECR-B-MF | • Rough operations • Used on unstable co | mponents | |||||
| EFS-E44 | • Used for machining a • Combination ofVIB | lloyed steel RAFREEandF | INISHROU | GH | |||
| EFS-B44 | • Unique design • Used for machining t • Fully effective • Semi-finish surface q | itanium, stainles uality | s and alloyed | steel | |||
| EC-E7/H7-CF | • For high speed mach • Trochoidal milling • Finish operations up | ining to10% X D | |||||
| EC-H-CF | • High speed machinin • Multiflute solid endmi • Tools for Super-Finis • Up to5% X D ROUGH:ae= 40% | g ll h - Full Cut ,ap | = 2 x D | ||||
| Material Grou Parameters | Du Grey Cast Iron | ctile Cast Iron | Malle | able Cas | t Iron | ||
| p | 15-16 | 17-18 | 19-20 | ||||
| Vc (IC900/608) (m/min) | 80-130 | 90-130 | 140-180 | ||||
| Vc (IC300) (m/min) | 60-140 | 70-140 | 110-150 | ap | |||
| Fz (Ø6–8) (mm/t) | 0.02-0.04 | 0.02-0.04 | 0.02-0.04 | ||||
| Fz (Ø10-12) (mm/t) | 0.03-0.05 | 0.03-0.05 | 0.03-0.05 | ||||
| Fz (Ø16-20) (mm/t) | 0.04-0.06 | 0.04-0.06 | 0.04-0.06 | ae |