Каталог Iscar токарный инструмент 2017 - страница 294
Навигация
 Каталог Iscar резьбонарезные фрезы
 Каталог Iscar инструмент для обработки алюминиевых колёс
 Каталог Iscar державки и пластины для нарезания резьбы 2022
 Каталог Iscar расточные системы 2022
 Каталог Iscar высокоточные развертки и метчики 2022
 Токарные инструменты Iscar (часть 2) 2026
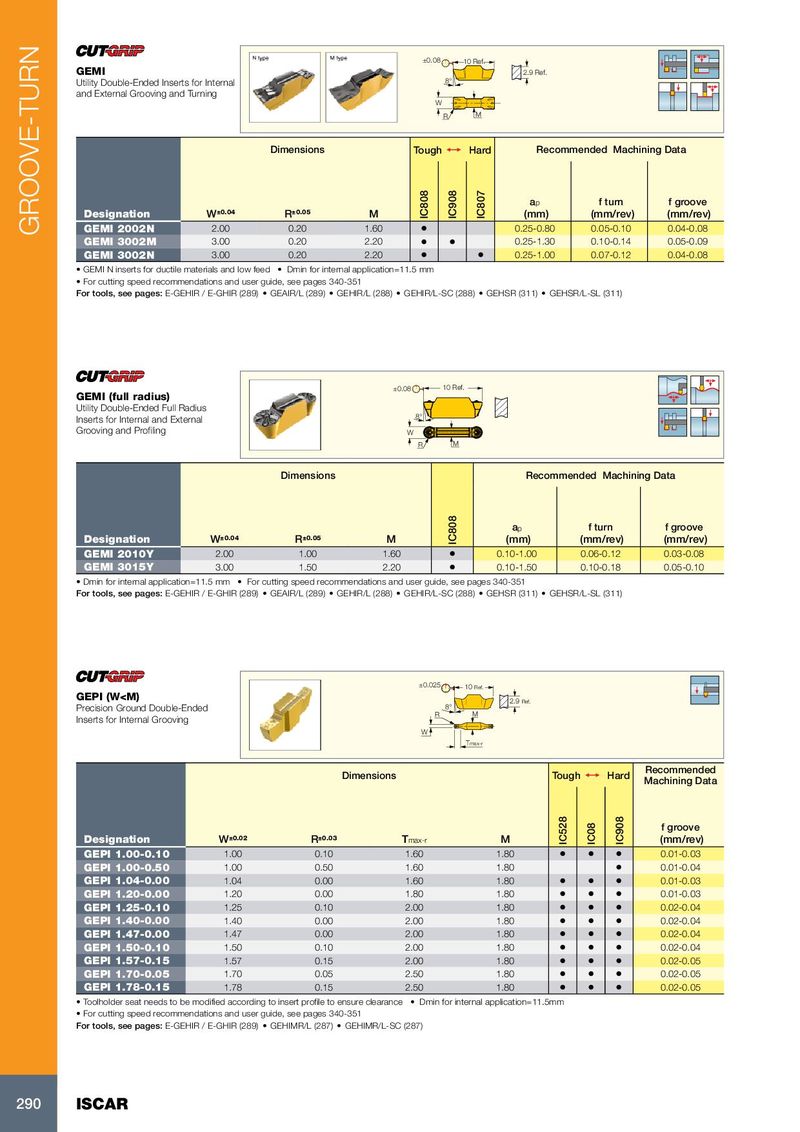
GROOVE-TURN
±0.08 10 Ref.
GEMI 2.9 Ref.
Utility Double-Ended Inserts for Internal 8°
and External Grooving and Turning
W
R M
Dimensions Tough 1 Hard Recommended Machining Data
IC808
IC908
IC807
ap f turn f groove
Designation W±0.04 R±0.05 M (mm) (mm/rev) (mm/rev)
GEMI 2002N 2.00 0.20 1.60 • 0.25-0.80 0.05-0.10 0.04-0.08
GEMI 3002M 3.00 0.20 2.20 • • 0.25-1.30 0.10-0.14 0.05-0.09
GEMI 3002N 3.00 0.20 2.20 • • 0.25-1.00 0.07-0.12 0.04-0.08
• GEMI N inserts for ductile materials and low feed • Dmin for internal application=11.5 mm
• For cutting speed recommendations and user guide, see pages 340-351
For tools, see pages: E-GEHIR / E-GHIR (289) • GEAIR/L (289) • GEHIR/L (288) • GEHIR/L-SC (288) • GEHSR (311) • GEHSR/L-SL (311)
±0.08 10 Ref.
GEMI (full radius)
Utility Double-Ended Full Radius
8°
Inserts for Internal and External
Grooving and Profiling W
R M
Dimensions Recommended Machining Data
IC808
ap f turn f groove
Designation W±0.04 R±0.05 M (mm) (mm/rev) (mm/rev)
GEMI 2010Y 2.00 1.00 1.60 • 0.10-1.00 0.06-0.12 0.03-0.08
GEMI 3015Y 3.00 1.50 2.20 • 0.10-1.50 0.10-0.18 0.05-0.10
• Dmin for internal application=11.5 mm • For cutting speed recommendations and user guide, see pages 340-351
For tools, see pages: E-GEHIR / E-GHIR (289) • GEAIR/L (289) • GEHIR/L (288) • GEHIR/L-SC (288) • GEHSR (311) • GEHSR/L-SL (311)
±0.025 10 Ref.
GEPI (W<M) 2.9 Ref.
Precision Ground Double-Ended 8°
R M
Inserts for Internal Grooving
W
Tmax-r
Recommended
Dimensions Tough 1 Hard
Machining Data
IC528
IC908
f groove
IC08
Designation W±0.02 R±0.03 Tmax-r M (mm/rev)
GEPI 1.00-0.10 1.00 0.10 1.60 1.80 • • • 0.01-0.03
GEPI 1.00-0.50 1.00 0.50 1.60 1.80 • 0.01-0.04
GEPI 1.04-0.00 1.04 0.00 1.60 1.80 • • • 0.01-0.03
GEPI 1.20-0.00 1.20 0.00 1.80 1.80 • • • 0.01-0.03
GEPI 1.25-0.10 1.25 0.10 2.00 1.80 • • • 0.02-0.04
GEPI 1.40-0.00 1.40 0.00 2.00 1.80 • • • 0.02-0.04
GEPI 1.47-0.00 1.47 0.00 2.00 1.80 • • • 0.02-0.04
GEPI 1.50-0.10 1.50 0.10 2.00 1.80 • • • 0.02-0.04
GEPI 1.57-0.15 1.57 0.15 2.00 1.80 • • • 0.02-0.05
GEPI 1.70-0.05 1.70 0.05 2.50 1.80 • • • 0.02-0.05
GEPI 1.78-0.15 1.78 0.15 2.50 1.80 • • • 0.02-0.05
• Toolholder seat needs to be modified according to insert profile to ensure clearance • Dmin for internal application=11.5mm
• For cutting speed recommendations and user guide, see pages 340-351
For tools, see pages: E-GEHIR / E-GHIR (289) • GEHIMR/L (287) • GEHIMR/L-SC (287)
290 ISCAR
±0.08 10 Ref.
GEMI 2.9 Ref.
Utility Double-Ended Inserts for Internal 8°
and External Grooving and Turning
W
R M
Dimensions Tough 1 Hard Recommended Machining Data
IC808
IC908
IC807
ap f turn f groove
Designation W±0.04 R±0.05 M (mm) (mm/rev) (mm/rev)
GEMI 2002N 2.00 0.20 1.60 • 0.25-0.80 0.05-0.10 0.04-0.08
GEMI 3002M 3.00 0.20 2.20 • • 0.25-1.30 0.10-0.14 0.05-0.09
GEMI 3002N 3.00 0.20 2.20 • • 0.25-1.00 0.07-0.12 0.04-0.08
• GEMI N inserts for ductile materials and low feed • Dmin for internal application=11.5 mm
• For cutting speed recommendations and user guide, see pages 340-351
For tools, see pages: E-GEHIR / E-GHIR (289) • GEAIR/L (289) • GEHIR/L (288) • GEHIR/L-SC (288) • GEHSR (311) • GEHSR/L-SL (311)
±0.08 10 Ref.
GEMI (full radius)
Utility Double-Ended Full Radius
8°
Inserts for Internal and External
Grooving and Profiling W
R M
Dimensions Recommended Machining Data
IC808
ap f turn f groove
Designation W±0.04 R±0.05 M (mm) (mm/rev) (mm/rev)
GEMI 2010Y 2.00 1.00 1.60 • 0.10-1.00 0.06-0.12 0.03-0.08
GEMI 3015Y 3.00 1.50 2.20 • 0.10-1.50 0.10-0.18 0.05-0.10
• Dmin for internal application=11.5 mm • For cutting speed recommendations and user guide, see pages 340-351
For tools, see pages: E-GEHIR / E-GHIR (289) • GEAIR/L (289) • GEHIR/L (288) • GEHIR/L-SC (288) • GEHSR (311) • GEHSR/L-SL (311)
±0.025 10 Ref.
GEPI (W<M) 2.9 Ref.
Precision Ground Double-Ended 8°
R M
Inserts for Internal Grooving
W
Tmax-r
Recommended
Dimensions Tough 1 Hard
Machining Data
IC528
IC908
f groove
IC08
Designation W±0.02 R±0.03 Tmax-r M (mm/rev)
GEPI 1.00-0.10 1.00 0.10 1.60 1.80 • • • 0.01-0.03
GEPI 1.00-0.50 1.00 0.50 1.60 1.80 • 0.01-0.04
GEPI 1.04-0.00 1.04 0.00 1.60 1.80 • • • 0.01-0.03
GEPI 1.20-0.00 1.20 0.00 1.80 1.80 • • • 0.01-0.03
GEPI 1.25-0.10 1.25 0.10 2.00 1.80 • • • 0.02-0.04
GEPI 1.40-0.00 1.40 0.00 2.00 1.80 • • • 0.02-0.04
GEPI 1.47-0.00 1.47 0.00 2.00 1.80 • • • 0.02-0.04
GEPI 1.50-0.10 1.50 0.10 2.00 1.80 • • • 0.02-0.04
GEPI 1.57-0.15 1.57 0.15 2.00 1.80 • • • 0.02-0.05
GEPI 1.70-0.05 1.70 0.05 2.50 1.80 • • • 0.02-0.05
GEPI 1.78-0.15 1.78 0.15 2.50 1.80 • • • 0.02-0.05
• Toolholder seat needs to be modified according to insert profile to ensure clearance • Dmin for internal application=11.5mm
• For cutting speed recommendations and user guide, see pages 340-351
For tools, see pages: E-GEHIR / E-GHIR (289) • GEHIMR/L (287) • GEHIMR/L-SC (287)
290 ISCAR