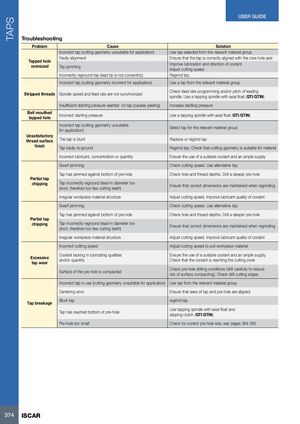
| Problem | Cause | Solution |
| Incorrect tap (cutting geometry unsuitable for application) | Use tap selected from the relevant material group |
| Tapped hole | Faulty alignment | Ensure that the tap is correctly aligned with the core hole axis |
| oversized | Tap jamming | Improve lubrication and direction of coolant Adjust cutting speed |
| Incorrectlyreground tap (lead tipis not concentric) | Regrind tap |
| Incorrect tap (cutting geometry incorrect for application) | Use a tap from the relevant material group |
| Stripped threads | Spindle speed and feed rate are not synchronized | Check feed rate programming and/or pitch of leading spindle. Use a tapping spindle with axial float (GTI/GTIN) |
| Insufficient starting pressure exerted on tap (causes peeling) | Increase starting pressure |
| Bell mouthed tapped hole | Incorrect starting pressure | Use a tapping spindle with axial float (GTI/GTIN) |
| Incorrect tap (cutting geometry unsuitable for application) | Select tap for the relevant material group |
| Unsatisfactory thread surface | The tap is blunt | Replace or regrind tap |
| finish | Tap badly re-ground | Regrind tap. Check that cutting geometry is suitable for material |
| Incorrect lubricant, concentration or quantity | Ensure the use of a suitable coolant and an ample supply |
| Swarf jamming | Check cutting speed. Use alternative tap |
| Partial tap | Tap has jammed against bottom of pre-hole | Check hole and thread depths. Drill a deeper pre-hole |
| chipping | Tap incorrectly reground (lead-in diameter too short, therefore too few cutting teeth) | Ensure that correct dimensions are maintained when regrinding |
| Irregular workpiece material structure | Adjust cutting speed. Improve lubricant quality of coolant |
| Swarf jamming | Check cutting speed. Use alternative tap |
| Partial tap | Tap has jammed against bottom of pre-hole | Check hole and thread depths. Drill a deeper pre-hole |
| chipping | Tap incorrectly reground (lead-in diameter too short, therefore too few cutting teeth) | Ensure that correct dimensions are maintained when regrinding |
| Irregular workpiece material structure | Adjust cutting speed. Improve lubricant quality of coolant |
| Incorrect cutting speed | Adjust cutting speed to suit workpiece material |
| Excessive tap wear | Coolant lacking in lubricating qualities and/or quantity | Ensure the use of a suitable coolant and an ample supply. Check that the coolant is reaching the cutting zone |
| Surface of the pre-hole is compacted | Check pre-hole drilling conditions (drill carefully to reduce risk of surface compacting). Check drill cutting edges |
| Incorrect tap in use (cutting geometry unsuitable for application) | Use tap from the relevant material group |
| Centering error | Ensure that axes of tap and pre-hole are aligned |
| Tap breakage | Blunt tap | regrind tap |
| Tap has reached bottom of pre-hole | Use tapping spindle with axial float and slipping clutch (GTI/GTIN) |
| Pre-hole too small | Check for correct pre-hole size, see pages 364-365 |
 Токарные инструменты Iscar (часть 2) 2026
 Каталог Iscar инструмент для обработки отверстий
 Каталог Iscar державки и пластины для нарезания резьбы 2022
 Каталог Iscar крепление инструмента
 Каталог Iscar токарные пластины ISO 2022
 Руководство Iscar режущий инструмент в производстве штампов и пресс-форм