Каталог Iscar высокоточные развертки и метчики 2022 - страница 10
Навигация
 Токарные инструменты Iscar (часть 2) 2026
 Каталог Iscar инструмент для обработки отверстий
 Каталог Iscar державки и пластины для нарезания резьбы 2022
 Каталог Iscar крепление инструмента
 Каталог Iscar токарные пластины ISO 2022
 Руководство Iscar режущий инструмент в производстве штампов и пресс-форм
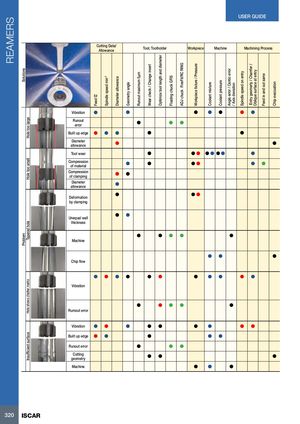
| Solutions | Cut Al Feed fZ | ting Da lowanc Spindle speed min-1 | ta/ e Diameter allowance | Geometry angle | Runout maximum 5µm | Tool; To Wear check / Change insert | olholde Optimize tool length and diameter | r Floating chuck GFIS | ADJ chuck FineFit/RC RING | Workpiece Workpiece fixture / Pressure | Coolant mixture | Machin Coolant pressure | e Angle error / Centic error / Axis deviation | M Spindle speed on entry | achining Entry geomerty / Chamfer / Oblique surface at entry | Proce Feed in and out same | ss Chip evacuation | |
| Vibration | • | • | • | • | • | • | • | |||||||||||
| oo large | Runout error | • | • | • | ||||||||||||||
| Hole t | Built up edge | • | • | • | • | • | ||||||||||||
| Diameter allowance | • | • | ||||||||||||||||
| l | Tool wear | • | •• | •• | •• | • | ||||||||||||
| o smal | Compression of material | • | • | •• | • | • | ||||||||||||
| Hole to | Compression of clamping | • | • | |||||||||||||||
| Diameter allowance | • | |||||||||||||||||
| Deformation by clamping | • | •• | ||||||||||||||||
| hole | Unequal wall thickness | • | • | |||||||||||||||
| Problem Tapered | Machine | • | • | • | • | • | ||||||||||||
| Chip flow | • | • | • | |||||||||||||||
| chatter marks | Vibration | • | • | • | • | • | • | • | • | • | • | • | ||||||
| Hole shows | Rumout error | • | • | • | • | • | ||||||||||||
| Vibration | • | • | • | • | • | • | • | • | • | |||||||||
| rface | Built up edge | • | • | • | • | • | ||||||||||||
| cient su | Runout error | • | • | • | ||||||||||||||
| Insuffi | Cutting geometry | • | • | • | ||||||||||||||
| Machine | • | • | • |