Каталог Iscar сверла со сменной режущей частью 2022 - страница 135
Навигация
 Каталог Iscar монолитные фрезы 2022
 Каталог Iscar токарный инструмент
 Каталог Iscar инструмент для мелкоразмерной обработки
 Каталог Iscar токарный инструмент для нарезания канавок
 Каталог Iscar полирующие фрезы
 Каталог Iscar дисковые фрезы и фрезерные пластины 2022
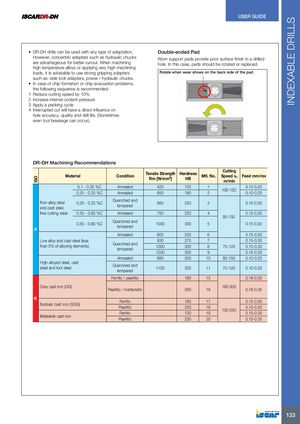
- DR-DH drills can be used with any type of adaptation. Double-ended Pad However, concentric adapters such as hydraulic chucks Worn support pads provide poor surface finish in a drilled are advantageous for better runout. When machining hole. In this case, pads should be rotated or replaced. high temperature alloys or applying very high machining loads, it is advisable to use strong gripping adapters Rotate when wear shows on the back side of the pad such as: side lock adapters, power / hydraulic chucks.
- In case of chip formation or chip evacuation problems, the following sequence is recommended:
1 Reduce cutting speed by 10% 2 Increase internal coolant pressure 3 Apply a pecking cycle 4 Interrupted cut will have a direct influence on hole accuracy, quality and drill life. (Sometimes even tool breakage can occur).
DR-DH Machining Recommendations
| ISO Material | Condition | Tensile Strength Rm [N/mm2] | Hardness HB | Mtl. No. | Cutting Speed vc m/min | Feed mm/rev |
| 0.1 - 0.25 %C | Annealed | 420 | 125 | 1 | 100150 | 0.10-0.25 |
| 0.25 - 0.25 %C | Annealed | 650 | 190 | 2 | - | 0.10-0.25 |
| Non-alloy steel and cast steel, 0.25 - 0.25 %C | Quenched and tempered | 850 | 250 | 3 | 0.15-0.30 | |
| free cutting steel 0.55 - 0.80 %C | Annealed | 750 | 220 | 4 | 80150 | 0.15-0.30 |
| P 0.55 - 0.80 %C | Quenched and tempered | 1000 | 300 | 5 | - | 0.15-0.30 |
| Annealed | 600 | 200 | 6 | 0.15-0.30 | ||
| Low alloy and cast steel (less | 930 | 275 | 7 | 0.15-0.30 | ||
| than 5% of alloying elements) | Quenched and temered | 1000 | 300 | 8 | 70-120 | 0.15-0.30 |
| p | 1200 | 350 | 9 | 0.15-0.30 | ||
| Annealed | 680 | 200 | 10 | 80-150 | 0.10-0.25 | |
| High alloyed steel, cast steel and tool steel | Quenched and tempered | 1100 | 325 | 11 | 70-120 | 0.10-0.25 |
| Ferritic / pearlitic | 180 | 15 | 0.18-0.35 | |||
| Grey cast iron (GG) | Pearlitic / martensitic | 260 | 16 | 180-300 | 0.18-0.35 | |
| K Nl i GGG | Ferritic | 160 | 17 | 0.15-0.30 | ||
| oduar cast ron () | Pearlitic | 250 | 18 | 150250 | 0.15-0.30 | |
| Ferritic | 130 | 19 | - | 0.15-0.35 | ||
| Malleable cast iron | Pearlitic | 230 | 20 | 0.15-0.35 |