Каталог Iscar сверла со сменной режущей частью 2022 - страница 130
Навигация
 Каталог Iscar монолитные фрезы 2022
 Каталог Iscar токарный инструмент
 Каталог Iscar инструмент для мелкоразмерной обработки
 Каталог Iscar токарный инструмент для нарезания канавок
 Каталог Iscar полирующие фрезы
 Каталог Iscar дисковые фрезы и фрезерные пластины 2022
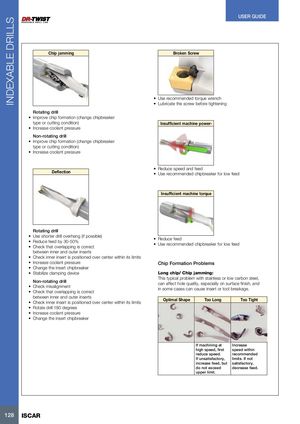
Chip jamming Broken Screw
Rotating drill
- Improve chip formation (change chipbreaker type or cutting condition)
- Increase coolant pressure Non-rotating drill
- Improve chip formation (change chipbreaker type or cutting condition)
- Increase coolant pressure
Deflection
- Use recommended torque wrench
- Lubricate the screw before tightening
Insufficient machine power-
- Reduce speed and feed
- Use recommended chipbreaker for low feed
Insufficient machine torque
Rotating drill
- Use shorter drill overhang (if possible)
- Reduce feed by 30-50%
- Check that overlapping is correct between inner and outer inserts
- Check inner insert is positioned over center within its limits
- Increase coolant pressure
- Change the insert chipbreaker
- Stabilize clamping device Non-rotating drill
- Check misalignment
- Check that overlapping is correct between inner and outer inserts
- Check inner insert is positioned over center within its limits
- Rotate drill 180 degrees
- Increase coolant pressure
- Change the insert chipbreaker
- Reduce feed
- Use recommended chipbreaker for low feed
Chip Formation Problems
Long chip/ Chip jamming: This typical problem with stainless or low carbon steel, can affect hole quality, especially on surface finish, and in some cases can cause insert or tool breakage.
Optimal Shape Too Long Too Tight
| If machining at | Increase |
| high speed, first | speed within |
| reduce speed. | recommended |
| If unsatisfactory, | limits. If not |
| increase feed, but | satisfactory, |
| do not exceed | decrease feed. |
upper limit.