Каталог Iscar сверла ружейные и для глубокого сверления 2022 - страница 94
Навигация
 Каталог Iscar новые продукты 2018
 Каталог Iscar полирующие фрезы
 Каталог Iscar инструмент для фрезерования
 Каталог Iscar инструмент для нарезания резьбы
 Каталог Iscar токарные державки ISO 2022
 Фрезерные инструменты Iscar 2026
Coolant
Successful deep hole drilling is achieved by an STS - Double tube system optimal combination of the tool, the machine and
| Workpiece | Outer | Double tube | |
| the coolant. Coolant plays an essential role in | tube | connector | |
| material |
| achieving secure and cost-efficient deep hole drilling | Drill | Guide | ||
| operations. Therefore, it is very important to choose | head | bush | Inner | Chip |
| the correct type of coolant and use it appropriately. | tube | box |
Coolant Coolant plays an essential role in lubricating tools, cooling cutting edges, chips and guide pads, as well as evacuating chips when drilling. It also improves No need for sealing
tool life, surface finish and cutting accuracy when continuously supplied during the machining process. Coolant unit A coolant unit is also important to obtain 1 Lubrication the best effect from the coolant. Lubrication of cutting edges and guide pads is necessary in deep hole drilling. For efficient lubrication, 1 Coolant pressure and volume should
| it is recommended to use EP (Extreme Pressure) | be fixed and continuous. | |
| additives which contain sulfur or chlorine. | ||
| An ideal coolant unit should be able to set any valve of | ||
| coolant pressure and volume and monitor the condition | ||
| 2 Temperature reduction | with gauges. A system that can detect trapped chips | |
| The ability to cool down the cutting edge and | by a pressure gauge and the screw pumps with | |
| chips depends on such characteristics as | an inverter controller are both recommended. | |
| thermal conductivity and relative heat. Coolant | ||
| with good cooling ability increases tool life, but | 2 Coolant temperature should be maintained. | |
| water-soluble coolant is not preferred in deep | ||
| Coolant is heated by factors, such as: | ||
| hole drilling because it reduces effectiveness. If | ||
| water-soluble coolant is used, the recommended | • Cutting edge | |
| concentration is 10% (dilution rate 1/10) or more. | • Friction on guide pad |
- Contact time of heated chips and coolant
| 3 Chip evacuation | • Pump |
| Maintaining coolant temperature is important to | |
| Coolant helps push chips through the back end of the | keeping stable cutting conditions, chip formation |
| boring bar (for STS) or inner tube (for DTS) until the chips | and cutting accuracy. The temperature should |
| are separated from the workpiece in general cutting | be lower than 40°C (100°F) for EP additives to |
| conditions. The flow and the pressure of coolant are | provide sufficient lubrication. Therefore, the coolant |
| also important in order to control chip evacuation. | temperature should be kept between 30 - 40°C |
| STS - Single tube system (90 - 100°F) throughout the cutting operation. | |
| Workpiece | |
| material | 3 Filtering Oil |
| Guide |
bush pressure Unwanted particles are contained in coolant after the
Drill Drill head Bar Chip
tube Sealing cutting operations, thus filtration is necessary to remove
head rest box
them. The filter size should be selected carefully to catch particles but not EP additives. Filter size depends on the coolant, but around 10 - 20 μm is generally suggested. For iron-based workpieces, a magnetic separator is helpful
as it decreases the frequency of filter maintenance.
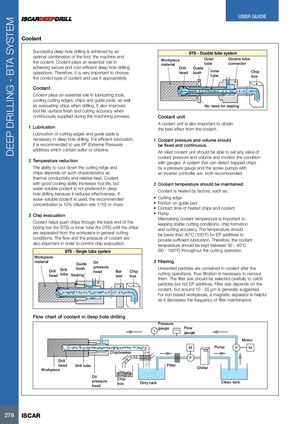
Flow chart of coolant in deep hole drilling
Pressure gauge Flow gauge Motor
| M | Pump | P | M | ||
| Chipbreaker | |||||
| P | |||||
| Drill |
| head | Drill tube | Filter | ||||
| Workpiece | Chiller | |||||
| Oil | ||||||
| pressure | Chip |
box Dirty tank Clean tank
head