Каталог Iscar сверла ружейные и для глубокого сверления 2022 - страница 86
Навигация
 Каталог Iscar новые продукты 2018
 Каталог Iscar полирующие фрезы
 Каталог Iscar инструмент для фрезерования
 Каталог Iscar инструмент для нарезания резьбы
 Каталог Iscar токарные державки ISO 2022
 Фрезерные инструменты Iscar 2026
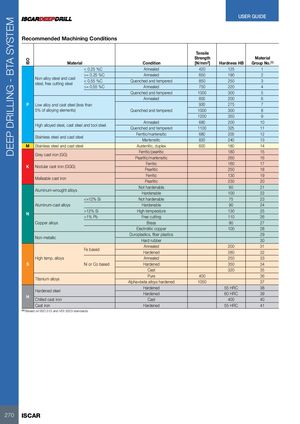
Recommended Machining Conditions
| ISO | Materia | l | Condition | Tensile Strength [N/mm2] | Hardness HB | Material Group No.(1) |
| < 0.25 %C | Annealed | 420 | 125 | 1 | ||
| Non-allo steel and cast | >= 0.25 %C | Annealed | 650 | 190 | 2 | |
| y tl f tti tl | < 0.55 %C | Quenched and tempered | 850 | 250 | 3 | |
| see, ree cung see | >= 0.55 %C | Annealed | 750 | 220 | 4 | |
| Quenched and tempered | 1000 | 300 | 5 | |||
| Annealed | 600 | 200 | 6 | |||
| P | Low alloy and cast steel (le | ss than | 930 | 275 | 7 | |
| 5% of alloying elements) | Quenched and tempered | 1000 | 300 | 8 | ||
| 1200 | 350 | 9 | ||||
| Annealed | 680 | 200 | 10 | |||
| High alloyed steel, cast ste | l and tool steel | Quenched and tempered | 1100 | 325 | 11 | |
| Stainless steel and cast ste | el | Ferritic/martensitic | 680 | 200 | 12 | |
| Martensitic | 820 | 240 | 13 | |||
| M | Stainless steel and cast ste | el | Austenitic,duplex | 600 | 180 | 14 |
| Gr t irn (GG) | Ferritic/pearlitic | 180 | 15 | |||
| ey cas o | Pearlitic/martensitic | 260 | 16 | |||
| K | Ndlr t irn (GGG) | Ferritic | 160 | 17 | ||
| oua cas o | Pearlitic | 250 | 18 | |||
| Mllbl t i | Ferritic | 130 | 19 | |||
| aeae cas ron | Pearlitic | 230 | 20 | |||
| Alih ll | Not hardenable | 60 | 21 | |||
| umnum-wrougt aoys | Hardenable | 100 | 22 | |||
| Not hardenable | 75 | 23 | ||||
| Aluminum-cast alloys | Hardenable | 90 | 24 | |||
| N | >12% Si | High temperature | 130 | 25 | ||
| >1% Pb | Free cutting | 110 | 26 | |||
| Copper alloys | Brass | 90 | 27 | |||
| Electrolitic copper | 100 | 28 | ||||
| Nlli | Duroplastics,fiberplastics | 29 | ||||
| on-metac | Hard rubber | 30 | ||||
| F bd | Annealed | 200 | 31 | |||
| e ase | Hardened | 280 | 32 | |||
| High temp. alloys | Annealed | 250 | 33 | |||
| S | Ni or Co based | Hardened | 350 | 34 | ||
| Cast | 320 | 35 | ||||
| Pure | 400 | 36 | ||||
| Titanium alloys | Alpha+beta alloys hardened | 1050 | 37 | |||
| Hdd tl | Hardened | 55 HRC | 38 | |||
| H | arene see | Hardened | 60 HRC | 39 | ||
| Chilled cast iron | Cast | 400 | 40 | |||
| Cast iron | Hardened | 55 HRC | 41 |
(1) Based on ISO 513 and VDI 3323 standards