Каталог Iscar сверла ружейные и для глубокого сверления 2022 - страница 32
Навигация
 Каталог Iscar новые продукты 2018
 Каталог Iscar полирующие фрезы
 Каталог Iscar инструмент для фрезерования
 Каталог Iscar инструмент для нарезания резьбы
 Каталог Iscar токарные державки ISO 2022
 Фрезерные инструменты Iscar 2026
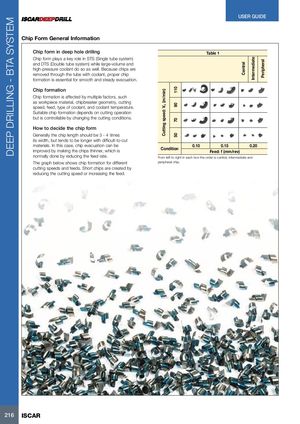
Chip Form General Information
Chip form in deep hole drilling Table 1 Chip form plays a key role in STS (Single tube system) and DTS (Double tube system) while large-volume and high-pressure coolant do so as well. Because chips are removed through the tube with coolant, proper chip formation is essential for smooth and steady evacuation.
Chip formation
Chip formation is affected by multiple factors, such as workpiece material, chipbreaker geometry, cutting speed, feed, type of coolant, and coolant temperature. Suitable chip formation depends on cutting operation but is controllable by changing the cutting conditions.
How to decide the chip form
Generally the chip length should be 3 - 4 times its width, but tends to be longer with difficult-to-cut
materials. In this case, chip evacuation can be 0.10 0.15 0.20
improved by making the chips thinner, which is Condition Feed: f (mm/rev) normally done by reducing the feed rate. From left to right in each box the order is central, intermediate and
The graph below shows chip formation for different peripheral chip. cutting speeds and feeds. Short chips are created by reducing the cutting speed or increasing the feed.