Каталог Iscar сверла ружейные и для глубокого сверления 2022 - страница 12
Навигация
 Каталог Iscar новые продукты 2018
 Каталог Iscar полирующие фрезы
 Каталог Iscar инструмент для фрезерования
 Каталог Iscar инструмент для нарезания резьбы
 Каталог Iscar токарные державки ISO 2022
 Фрезерные инструменты Iscar 2026
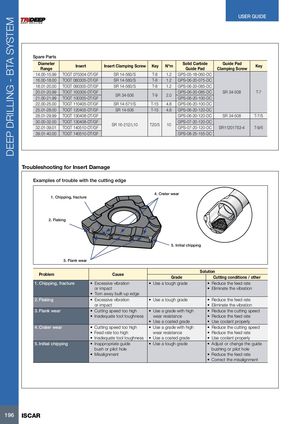
Spare Parts
| Diameter Range | Insert | Insert Clamping Screw | Key | Nm | Solid Carbide Guide Pad | Guide Pad Clamping Screw | Key |
| 14.00-15.99 | TOGT 070304-DT/GF | SR 14-560/S | T-8 | 1.2 | GPS-05-18-060-DC | ||
| 16.00-18.00 | TOGT 080305-DT/GF | SR 14-560/S | T-8 | 1.2 | GPS-06-20-075-DC | ||
| 18.01-20.00 | TOGT 090305-DT/GF | SR 14-560/S | T-8 | 1.2 | GPS-06-20-085-DC | ||
| 20.01-20.99 | TOGT 100305-DT/GF | SR 34506 | T9 | 20 | GPS-06-20-085-DC | SR 34-508 | T-7 |
| 21.00-21.99 | TOGT 100305-DT/GF | - | - | . | GPS-06-20-100-DC | ||
| 22.00-25.00 | TOGT 110405-DT/GF | SR 14-571/S | T-15 | 4.8 | GPS-06-20-100-DC | ||
| 25.01-28.00 | TOGT 120405-DT/GF | SR 14-506 | T-15 | 4.8 | GPS-06-20-120-DC | ||
| 28.01-29.99 | TOGT 130408-DT/GF | GPS-06-20-120-DC | SR 34-508 | T-7/5 | |||
| 30.00-32.00 | TOGT 130408-DT/GF | SR 16212/L10 | T20/5 | 10 | GPS-07-20-120-DC | ||
| 32.01-39.01 | TOGT 140510-DT/GF | - | GPS-07-20-120-DC | SR11201753-4 | T-9/5 | ||
| 39.01-40.00 | TOGT 140510-DT/GF | GPS-08-25-155-DC |
Troubleshooting for Insert Damage
Examples of trouble with the cutting edge
4. Crater wear 1. Chipping, fracture
2. Flaking
5. Initial chipping
3. Flank wear
| Solution | |||
| Problem | Cause | Grade | Cutting conditions / other |
| 1. Chipping, fracture | • Excessive vibration or impact • Torn awaybuilt-upedge | • Use a tough grade | • Reduce the feed rate • Eliminate the vibration |
| 2. Flaking | • Excessive vibration or impact | • Use a tough grade | • Reduce the feed rate • Eliminate the vibration |
| 3. Flank wear | • Cutting speed too high • Inadequate tool toughness | • Use a grade with high wear resistance • Use a coatedgrade | • Reduce the cutting speed • Reduce the feed rate • Use coolantproperly |
| 4. Crater wear | • Cutting speed too high • Feed rate too high • Inadequate tool toughness | • Use a grade with high wear resistance • Use a coatedgrade | • Reduce the cutting speed • Reduce the feed rate • Use coolantproperly |
| 5. Initial chipping | • Inappropriate guide bush or pilot hole • Misalignment | • Use a tough grade | • Adjust or change the guide bushing or pilot hole • Reduce the feed rate • Correct the misalignment |