Каталог Iscar отрезка 2022 - страница 32
Навигация
 Токарные инструменты Iscar (часть 1) 2026
 Каталог Iscar монолитные фрезы 2022
 Инструменты для обработки отверстий Iscar 2026
 Каталог Iscar резьбонарезные фрезы
 Каталог Iscar расточные системы
 Каталог Iscar токарный инструмент 2017
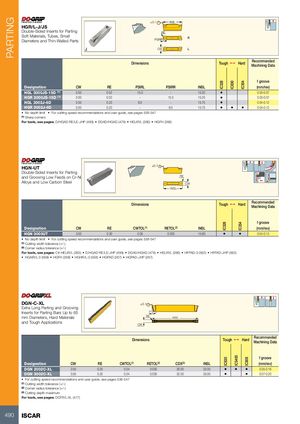
PARTING
±0.1 lNSL
HGR/L-J/JS
Double-Sided Inserts for Parting RE
Soft Materials, Tubes, Small R
PSIRR
Diameters and Thin-Walled Parts
CW L
Recommended
Dimensions Tough 1 Hard
Machining Data
f groove
IC328
IC830
IC354
Designation CW RE PSIRL PSIRR INSL (mm/rev)
HGL 3000JS-15D (1) 3.00 0.02 15.0 - 15.20 • 0.03-0.07
HGR 3000JS-15D (1) 3.00 0.02 - 15.0 15.20 • 0.03-0.07
HGL 3002J-6D 3.00 0.20 6.0 - 15.70 • 0.04-0.12
HGR 3002J-6D 3.00 0.20 - 6.0 15.70 • • • 0.04-0.12
• No depth limit • For cutting speed recommendations and user guide, see pages 538-547
(1) Sharp corners
For tools, see pages: D/HGAD RE/LE-JHP (499) • DGAD/HGAD (479) • HELIR/L (266) • HGFH (268)
±0.1
HGN-UT
Double-Sided Inserts for Parting
and Grooving Low Feeds on Cr-Ni RE
Alloys and Low Carbon Steel CW
INSL
Recommended
Dimensions Tough 1 Hard
Machining Data
IC328 f groove
IC354
Designation CW RE CWTOL(1) RETOL(2) INSL (mm/rev)
HGN 3003UT 3.00 0.30 0.05 0.030 15.80 • • 0.04-0.13
• No depth limit • For cutting speed recommendations and user guide, see pages 538-547
(1) Cutting width tolerance (+/-)
(2) Corner radius tolerance (+/-)
For tools, see pages: C#-HELIR/L (265) • D/HGAD RE/LE-JHP (499) • DGAD/HGAD (479) • HELIR/L (266) • HFPAD-3 (562) • HFPAD-JHP (562)
• HGAIR/L-3 (568) • HGFH (268) • HGHR/L-3 (558) • HGPAD (267) • HGPAD-JHP (267)
DGN-C-XL ±0.1
Extra Long Parting and Grooving
Inserts for Parting Bars Up to 65 7°
RE
mm Diameters, Hard Materials INSL
and Tough Applications CW
Recommended
Dimensions Tough 1 Hard
Machining Data
f groove
IC5400
IC830
IC808
Designation CW RE CWTOL(1) RETOL(2) CDX(3) INSL (mm/rev)
DGN 2002C-XL 2.05 0.20 0.04 0.030 30.00 32.00 • • • 0.05-0.16
DGN 3002C-XL 3.00 0.20 0.04 0.030 32.50 35.00 • • 0.07-0.20
• For cutting speed recommendations and user guide, see pages 538-547
(1) Cutting width tolerance (+/-)
(2) Corner radius tolerance (+/-)
(3) Cutting depth maximum
For tools, see pages: DGTR/L-XL (477)
490 ISCAR
±0.1 lNSL
HGR/L-J/JS
Double-Sided Inserts for Parting RE
Soft Materials, Tubes, Small R
PSIRR
Diameters and Thin-Walled Parts
CW L
Recommended
Dimensions Tough 1 Hard
Machining Data
f groove
IC328
IC830
IC354
Designation CW RE PSIRL PSIRR INSL (mm/rev)
HGL 3000JS-15D (1) 3.00 0.02 15.0 - 15.20 • 0.03-0.07
HGR 3000JS-15D (1) 3.00 0.02 - 15.0 15.20 • 0.03-0.07
HGL 3002J-6D 3.00 0.20 6.0 - 15.70 • 0.04-0.12
HGR 3002J-6D 3.00 0.20 - 6.0 15.70 • • • 0.04-0.12
• No depth limit • For cutting speed recommendations and user guide, see pages 538-547
(1) Sharp corners
For tools, see pages: D/HGAD RE/LE-JHP (499) • DGAD/HGAD (479) • HELIR/L (266) • HGFH (268)
±0.1
HGN-UT
Double-Sided Inserts for Parting
and Grooving Low Feeds on Cr-Ni RE
Alloys and Low Carbon Steel CW
INSL
Recommended
Dimensions Tough 1 Hard
Machining Data
IC328 f groove
IC354
Designation CW RE CWTOL(1) RETOL(2) INSL (mm/rev)
HGN 3003UT 3.00 0.30 0.05 0.030 15.80 • • 0.04-0.13
• No depth limit • For cutting speed recommendations and user guide, see pages 538-547
(1) Cutting width tolerance (+/-)
(2) Corner radius tolerance (+/-)
For tools, see pages: C#-HELIR/L (265) • D/HGAD RE/LE-JHP (499) • DGAD/HGAD (479) • HELIR/L (266) • HFPAD-3 (562) • HFPAD-JHP (562)
• HGAIR/L-3 (568) • HGFH (268) • HGHR/L-3 (558) • HGPAD (267) • HGPAD-JHP (267)
DGN-C-XL ±0.1
Extra Long Parting and Grooving
Inserts for Parting Bars Up to 65 7°
RE
mm Diameters, Hard Materials INSL
and Tough Applications CW
Recommended
Dimensions Tough 1 Hard
Machining Data
f groove
IC5400
IC830
IC808
Designation CW RE CWTOL(1) RETOL(2) CDX(3) INSL (mm/rev)
DGN 2002C-XL 2.05 0.20 0.04 0.030 30.00 32.00 • • • 0.05-0.16
DGN 3002C-XL 3.00 0.20 0.04 0.030 32.50 35.00 • • 0.07-0.20
• For cutting speed recommendations and user guide, see pages 538-547
(1) Cutting width tolerance (+/-)
(2) Corner radius tolerance (+/-)
(3) Cutting depth maximum
For tools, see pages: DGTR/L-XL (477)
490 ISCAR