Каталог Iscar обработка канавок 2022 - страница 99
Навигация
 Каталог Iscar монолитные концевые фрезы и система multi-master
 Фрезерные инструменты Iscar 2026
 Каталог Iscar сверла ружейные и для глубокого сверления 2022
 Каталог Iscar токарные державки ISO 2022
 Каталог Iscar инструмент для обработки алюминиевых колёс
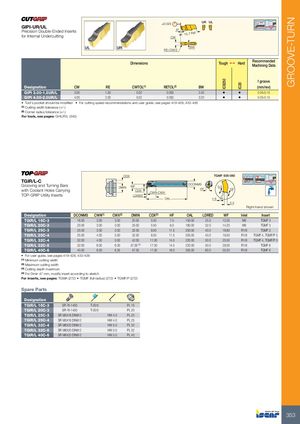
±0.025 UR UL
GIPI-UR/UL
for Internal Undercutting 15.7 Ref. CW BW RE=CW/2
Recommended
Dimensions Tough 1 Hard Machining Data
f groove
| Designation | CW | RE | CWTOL(1) | RETOL(2) | BW | (mm/rev) | |||
| GIPI 3.00-1.5UR/L | 3.00 | 1.50 | 0.02 | 0.050 | 2.40 | • | • | 0.05-0.15 | |
| GIPI 4.00-2.0UR/L | 4.00 | 2.00 | 0.02 | 0.050 | 3.20 | • | • | 0.05-0.15 |
- Tool's pocket should be modified
- For cutting speed recommendations and user guide, see pages 419-428, 432-436
(1) Cutting width tolerance (+/-) (2) Corner radius tolerance (+/-)
For tools, see pages: GHIUR/L (345)
| TGIR/L-C Grooving and Turning Bars | CD DMIN | WF X | DCONM | S T | 0.5 ° GMF 635-080 | ||||||
| with Coolant Holes Carrying TOP-GRIP Utility Inserts | CDX LDRED | CWN-CW | X OAL | HF 1.6 | 5.5 19 | Rig | ht-hand shown | ||||
| Designation | DCONMS | CWN(1) | CWX(2) | DMIN | CDX(3) | HF | OAL | LDRED | WF | Inlet | Insert |
| TGIR/L 16C-3 | 16.00 | 3.00 | 3.00 | 20.50 | 5.50 | 7.5 | 150.00 | 25.0 | 12.00 | M6 | TGMF 3 |
| TGIR/L 20C-3 | 20.00 | 3.00 | 3.00 | 25.00 | 5.50 | 9.0 | 180.00 | 32.0 | 14.20 | M6 | TGMF 3 |
| TGIR/L 25C-3 | 25.00 | 3.00 | 3.00 | 32.00 | 8.00 | 11.5 | 200.00 | 40.0 | 18.80 | R1/8 | TGMF 3 |
| TGIR/L 25C-4 | 25.00 | 4.00 | 5.00 | 32.50 | 8.50 | 11.5 | 200.00 | 40.0 | 19.50 | R1/8 | TGMF 4, TGMF/P 5 |
| TGIR/L 32C-4 | 32.00 | 4.00 | 5.00 | 42.00 | 11.00 | 14.5 | 220.00 | 50.0 | 25.50 | R1/8 | TGMF 4, TGMF/P 5 |
| TGIR/L 32C-6 | 32.00 | 6.00 | 6.35 | 57.00(4) | 17.50 | 14.5 | 220.00 | 50.0 | 29.00 | R1/8 | TGMF 6 |
| TGIR/L 40C-6 | 40.00 | 6.00 | 6.35 | 57.00 | 17.50 | 18.0 | 300.00 | 60.0 | 35.20 | R1/8 | TGMF 6 |
- For user guide, see pages 419-428, 432-436
(1) Minimum cutting width (2) Maximum cutting width (3) Cutting depth maximum (4) For Dmin 47 mm, modify insert according to sketch
For inserts, see pages: TGMA (272) TGMF (full radius) (272) TGMF/P (272)
Spare Parts
| Designation | ||||
| TGIR/L 16C-3 | SR 76-1400 | T-20/5 | PL 16 | |
| TGIR/L 20C-3 | SR 76-1400 | T-20/5 | PL 20 | |
| TGIR/L 25C-3 | SR M5X16 DIN912 | HW 4.0 | PL 25 | |
| TGIR/L 25C-4 | SR M5X16 DIN912 | HW 4.0 | PL 25 | |
| TGIR/L 32C-4 | SR M6X20 DIN912 | HW 5.0 | PL 32 | |
| TGIR/L 32C-6 | SR M6X20 DIN912 | HW 5.0 | PL 32 | |
| TGIR/L 40C-6 | SR M6X25 DIN912 | HW 5.0 | PL 40 |