Каталог Iscar монолитные фрезы 2022 - страница 71
Навигация
 Каталог Iscar торцевые фрезы 2022
 Каталог Iscar инструмент для нарезания резьбы
 Каталог Iscar новые продукты 2018
 Каталог Iscar инструмент для токарной обработки
 Каталог Iscar инструмент для обработки алюминиевых колёс
 Фрезерные инструменты Iscar 2026
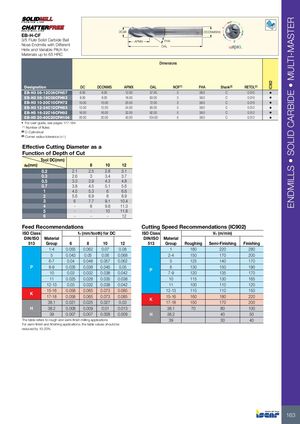
EB-H-CF 3/5 Flute Solid Carbide Ball Nose Endmills with Different Helix and Variable Pitch for Materials up to 65 HRC
APMX
λ α
FHA β α#β#λ OAL
Dimensions
| Designation | DC | DCONMS | APMX | OAL | NOF(1) | FHA | Shank(2) | RETOL(3) | IC902 |
| EB-H3 06-12C06CFH57 | 6.00 | 6.00 | 12.00 | 57.00 | 3 | 38.0 | C | 0.010 | • |
| EB-H3 08-16C08CFH63 | 8.00 | 8.00 | 16.00 | 63.00 | 3 | 38.0 | C | 0.010 | • |
| EB-H3 10-20C10CFH72 | 10.00 | 10.00 | 20.00 | 72.00 | 3 | 38.0 | C | 0.010 | • |
| EB-H3 12-24C12CFH83 | 12.00 | 12.00 | 24.00 | 83.00 | 3 | 38.0 | C | 0.012 | • |
| EB-H5 16-32C16CFH92 | 16.00 | 16.00 | 32.00 | 92.00 | 5 | 38.0 | C | 0.012 | • |
| EB-H5 20-40C20CFH104 | 20.00 | 20.00 | 40.00 | 104.00 | 5 | 38.0 | C | 0.012 | • |
- For user guide, see pages 177-184 (1) Number of flutes
(2) C-Cylindrical (3) Corner radius tolerance (+/-)
Effective Cutting Diameter as a
Function of Depth of Cut
| Tool DC(mm) ap(mm) | 8 | 10 | 12 | |
| 0.2 | 2.1 | 2.5 | 2.8 | 3.1 |
| 0.3 | 2.6 | 3 | 3.4 | 3.7 |
| 0.5 | 3.3 | 3.9 | 4.3 | 4.8 |
| 0.7 | 3.8 | 4.5 | 5.1 | 5.6 |
| 1 | 4.5 | 5.3 | 6 | 6.6 |
| 2 | 5.6 | 6.9 | 8 | 8.9 |
| 3 | 6 | 7.7 | 9.1 | 10.4 |
| 4 | - | 8 | 9.8 | 11.3 |
| 5 | - | - | 10 | 11.8 |
| 6 | - | - | - | 12 |
Feed Recommendations Cutting Speed Recommendations (IC902)
| ISO Class | f | z (mm/too | th) for DC | ||
| DIN/ISO | Material | ||||
| 513 | Group | 6 | 8 | 10 | 12 |
| 1-4 | 0.055 | 0.062 | 0.07 | 0.08 | |
| 5 | 0.043 | 0.05 | 0.06 | 0.068 | |
| 6-7 | 0.04 | 0.048 | 0.057 | 0.062 | |
| P | 8-9 | 0.035 | 0.038 | 0.045 | 0.05 |
| 10 | 0.03 | 0.032 | 0.038 | 0.042 | |
| 11 | 0.025 | 0.028 | 0.035 | 0.038 | |
| 12-13 | 0.03 | 0.032 | 0.038 | 0.042 | |
| K | 15-16 | 0.058 | 0.065 | 0.073 | 0.085 |
| 17-18 | 0.058 | 0.065 | 0.073 | 0.085 | |
| 38.1 | 0.021 | 0.025 | 0.027 | 0.03 | |
| H | 38.2 | 0.008 | 0.009 | 0.01 | 0.013 |
| 39 | 0.007 | 0.007 | 0.008 | 0.009 |
| ISO Class | Vc (m/min) | |||
| DIN/ISO 513 | Material Group | Roughing | Semi-Finishing | Finishing |
| 1 | 180 | 220 | 280 | |
| 2-4 | 150 | 170 | 200 | |
| 5 | 125 | 140 | 170 | |
| P | 6 | 130 | 150 | 190 |
| 7-9 | 120 | 135 | 170 | |
| 10 | 115 | 130 | 165 | |
| 11 | 100 | 110 | 120 | |
| 12-13 | 110 | 110 | 150 | |
| K | 15-16 | 160 | 180 | 220 |
| 17-18 | 150 | 170 | 200 | |
| 38.1 | 70 | 80 | 100 | |
| H | 38.2 | 40 | 50 | |
| 39 | 30 | 40 |
For semi-finish and finishing applications, the table values should be reduced by 10-20%