Каталог Iscar монолитные фрезы 2022 - страница 30
Навигация
 Каталог Iscar торцевые фрезы 2022
 Каталог Iscar инструмент для нарезания резьбы
 Каталог Iscar новые продукты 2018
 Каталог Iscar инструмент для токарной обработки
 Каталог Iscar инструмент для обработки алюминиевых колёс
 Фрезерные инструменты Iscar 2026
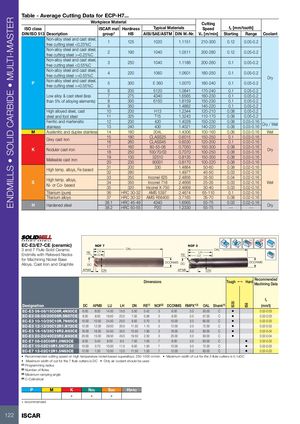
Table - Average Cutting Data for ECP-H7...
| Wor | kpiece Mat | erial | Cutting | ||||||
| ISO class | ISCAR mat | Hardness | Typical Ma | terials | Speed | fz [m | m/tooth] | ||
| DIN/ISO 513 | Description | group | HB | AISI/SAE/ASTM | DIN W.-Nr. | Vc [m/min] | Starting | Range | Coolant |
| Non-alloy steel and cast steel, free cutting steel | 1 | 125 | 1020 | 1.1151 | 210-300 | 0.12 | 0.05-0.2 | ||
| Non-alloy steel and cast steel, free cutting steel >=0.25%C | 2 | 190 | 1040 | 1.0511 | 200-280 | 0.12 | 0.05-0.2 | ||
| Non-alloy steel and cast steel, free cutting steel | 3 | 250 | 1040 | 1.1186 | 200-260 | 0.1 | 0.05-0.2 | ||
| Non-alloy steel and cast steel, free cutting steel >=0.55%C | 4 | 220 | 1060 | 1.0601 | 180-250 | 0.1 | 0.05-0.2 | Dr | |
| P | Non-alloy steel and cast steel, free cutting steel >=0.55%C | 5 | 300 | E 360 | 1.0070 | 180-240 | 0.1 | 0.05-0.2 | y |
| 6 | 200 | 5120 | 1.0841 | 170-240 | 0.1 | 0.05-0.2 | |||
| Low alloy & cast steel (less | 7 | 275 | 4340 | 1.6565 | 160-230 | 0.1 | 0.05-0.2 | ||
| than 5% of alloying elements) | 8 | 300 | 6150 | 1.8159 | 150-230 | 0.1 | 0.05-0.2 | ||
| 9 | 350 | 1.4882 | 140-220 | 0.1 | 0.05-0.2 | ||||
| High alloyed steel, cast | 10 | 200 | H13 | 1.2344 | 120-210 | 0.08 | 0.05-0.2 | ||
| steel and tool steel | 11 | 325 | T15 | 1.3243 | 110-170 | 0.08 | 0.05-0.2 | ||
| Ferritic and martensitic | 12 | 200 | 420 | 1.4028 | 150-230 | 0.08 | 0.03-0.16 | D / Wt | |
| stainless | 13 | 240 | 430 | 1.4021 | 140-220 | 0.08 | 0.03-0.16 | ry e | |
| M | Austenitic and duplex stainless | 14 | 180 | 304L | 1.4306 | 100-160 | 0.06 | 0.03-0.16 | Wet |
| Gti | 15 | 180 | CLASS25 | 0.6015 | 150-250 | 0.1 | 0.03-0.16 | ||
| rey cas ron | 16 | 260 | CLASS45 | 0.6030 | 120-200 | 0.1 | 0.03-0.16 | ||
| 17 | 160 | 80-55-06 | 0.7050 | 150-300 | 0.08 | 0.03-0.16 | |||
| K | Nodular cast iron | 18 | 250 | 100/70/03 | 0.7070 | 100-250 | 0.08 | 0.03-0.16 | Dry |
| Mllbl t i | 19 | 130 | 32510 | 0.8135 | 150-300 | 0.08 | 0.03-0.16 | ||
| aeae cas ron | 20 | 230 | 90001 | 0.8170 | 100-220 | 0.08 | 0.03-0.16 | ||
| Hih t ll Fbd | 31 | 200 | 330 | 1.4864 | 50-60 | 0.08 | 0.02-0.16 | ||
| g emp. aoys, e-ase | 32 | 280 | 1.4977 | 40-50 | 0.03 | 0.02-0.16 | |||
| 33 | 250 | Inconel 625 | 2.4856 | 35-50 | 0.04 | 0.02-0.16 | |||
| S | High temp. alloys, | 34 | 350 | Inconel 718 | 2.4668 | 25-35 | 0.03 | 0.02-0.16 | Wet |
| Ni- or Co- based | 35 | 320 | Inconel X-750 | 2.4669 | 30-40 | 0.03 | 0.02-0.16 | ||
| Titanium (pure) | 36 | HRC 30-32 | AMS 5397 | 2.4674 | 65-110 | 0.1 | 0.02-0.16 | ||
| Titanium alloys | 37 | HRC 30-32 | AMS R56400 | 3.7165 | 35-70 | 0.08 | 0.02-0.16 | ||
| H | Hdd l | 38.1 | HRC 45-49 | 4340 | 1.6565 | 55-75 | 0.03 | 0.02-0.16 | D |
| arene stee | 38.2 | HRC 50-55 | P20 | 1.2330 | 55-75 | --- | --- | ry |
| EC-E3/E7-CE (ceramic) d 7 Fl Slid Ci | NOF 7 | O | AL | NOF 3 | OAL | Rd° | |||||||
| an ute o eramc | LH | LH | |||||||||||
| Endmills with Relieved Necks | RE | LU | RE L | U | |||||||||
| or Machining Nickel Base | DCONMS | D | ONMS | ||||||||||
| Alloys, Cast Iron and Graphite | DC | DC | |||||||||||
| APMX | D | N | A | PMX | DN | ||||||||
| Dime | nsions | Tough1 Hard | Recommended Machining Data | ||||||||||
| Designation | DC | APMX | LU | LH | DN | RE(1) | NOF(2) | DCONMS | RMPX°(3) | OAL | Shank(4) | IS35 IS6 | fz (mm/t) |
| EC-E3 06-06/15C06R.4N50CE | 6.00 | 6.00 | 14.50 | 15.0 | 5.50 | 0.42 | 3 | 6.00 | 3.0 | 50.00 | C | • | 0.02-0.03 |
| EC-E3 08-08/20C08R.5N57CE | 8.00 | 8.00 | 19.50 | 20.0 | 7.50 | 0.56 | 3 | 8.00 | 3.0 | 57.00 | C | • | 0.02-0.03 |
| EC-E3 10-10/25C10R.7N65CE | 10.00 | 10.00 | 24.50 | 25.0 | 9.50 | 0.70 | 3 | 10.00 | 3.0 | 65.00 | C | • | 0.02-0.03 |
| EC-E3 12-12/30C12R1.N72CE | 12.00 | 12.00 | 29.50 | 30.0 | 11.50 | 1.10 | 3 | 12.00 | 3.0 | 72.00 | C | • | 0.02-0.03 |
| EC-E3 16-16/35C16R2.N83CE | 16.00 | 16.00 | 34.50 | 35.0 | 15.50 | 1.90 | 3 | 16.00 | 3.0 | 83.00 | C | • | 0.02-0.04 |
| EC-E3 20-20/40C20R2.N93CE | 20.00 | 15.00 | 39.50 | 40.0 | 19.50 | 2.50 | 3 | 20.00 | 3.0 | 93.00 | C | • | 0.02-0.04 |
| EC-E7 08-02C08R1.0N63CE | 8.00 | 0.40 | 8.00 | 9.5 | 7.50 | 1.00 | 7 | 8.00 | 3.0 | 63.00 | C | • | 0.02-0.03 |
| EC-E7 10-02C10R1.5N72CE | 10.00 | 0.70 | 10.00 | 11.5 | 9.50 | 1.50 | 7 | 10.00 | 3.0 | 72.00 | C | • | 0.02-0.03 |
| EC-E7 12-02C12R1.5N83CE | 12.00 | 1.30 | 10.00 | 12.0 | 11.50 | 1.50 | 7 | 12.00 | 3.0 | 83.00 | C | • | 0.02-0.03 |
- Recommended cutting speed on high temperature nickel-based superalloys: 250-1000 m/min
- Maximum width of cut for the 3 flute cutters is 0.1xDC
- Maximum width of cut for the 7 flute cutters is DC
- Only air coolant should be used
(1) Programming radius (2) Number of flutes (3) Maximum ramping angle (4) C-Cylindrical
P M K N(K) S(M) H(P/K)
+ recommended