Каталог Iscar монолитные фрезы 2022 - страница 10
Навигация
 Каталог Iscar торцевые фрезы 2022
 Каталог Iscar инструмент для нарезания резьбы
 Каталог Iscar новые продукты 2018
 Каталог Iscar инструмент для токарной обработки
 Каталог Iscar инструмент для обработки алюминиевых колёс
 Фрезерные инструменты Iscar 2026
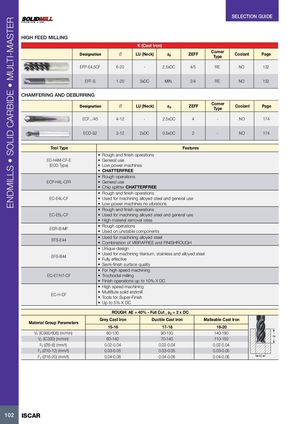
HIGH FEED MILLING
| Designation | Ø | K(Cast Iro LU (Neck) | n) ap | ZEFF | Corner Type | Coolant | Page |
| EFP-E4,5CF | 6-20 | - | 2.5xDC | 4/5 | RE | NO | 132 |
| EFF-S | 1-20 | 3xDC | MIN. | 2/4 | RE | NO | 132 |
CHAMFERING AND DEBURRING
| Designation | Ø | LU (Neck) | ap | ZEFF | Corner Type | Coolant | Page |
| ECF.../45 | 4-12 | - | 2.5xDC | 4 | - | NO | 174 |
| ECD-S2 | 3-12 | 2xDC | 0.5xDC | 2 | - | NO | 174 |
| Tool Type | Features |
| EC-H4M-CF-E (ECO Type) | • Rough and finish operations • General use • Low power machines •CHATTERFREE |
| ECP-H4L-CFR | • Rough operations • General use • ChipsplitterCHATTERFREE |
| EC-E4L-CF | • Rough and finish operations • Used for machining alloyed steel and general use • Lowpower machines no vibrations |
| EC-E5L-CF | • Rough and finish operations • Used for machining alloyed steel and general use • High material removal rates |
| ECR-B-MF | • Rough operations • Used on unstable components |
| EFS-E44 | • Used for machining alloyed steel • Combination of VIBRAFREE and FINISHROUGH |
| EFS-B44 | • Unique design • Used for machining titanium, stainless and alloyed steel • Fully effective • Semi-finish surfacequality |
| EC-E7/H7-CF | • For high speed machining • Trochoidal milling • Finish operations upto 10% X DC |
| EC-H-CF | • High speed machining • Multiflute solid endmill • Tools for Super-Finish • Upto 5% X DC |
| Material Group Parameters | ROUGH: AE = Grey Cast Iron | 40% - Full Cut, ap = 2 x DC Ductile Cast Iron | Malleable Cast Iron | |
| 15-16 | 17-18 | 19-20 | ||
| Vc(IC900/608) (m/min) | 80-130 | 90-130 | 140-180 | a |
| Vc(IC300) (m/min) | 60-140 | 70-140 | 110-150 | p |
| Fz(Ø6–8) (mm/t) | 0.02-0.04 | 0.02-0.04 | 0.02-0.04 | |
| Fz(Ø10-12) (mm/t) | 0.03-0.05 | 0.03-0.05 | 0.03-0.05 | |
| Fz (Ø16-20) (mm/t) | 0.04-0.06 | 0.04-0.06 | 0.04-0.06 | AE |